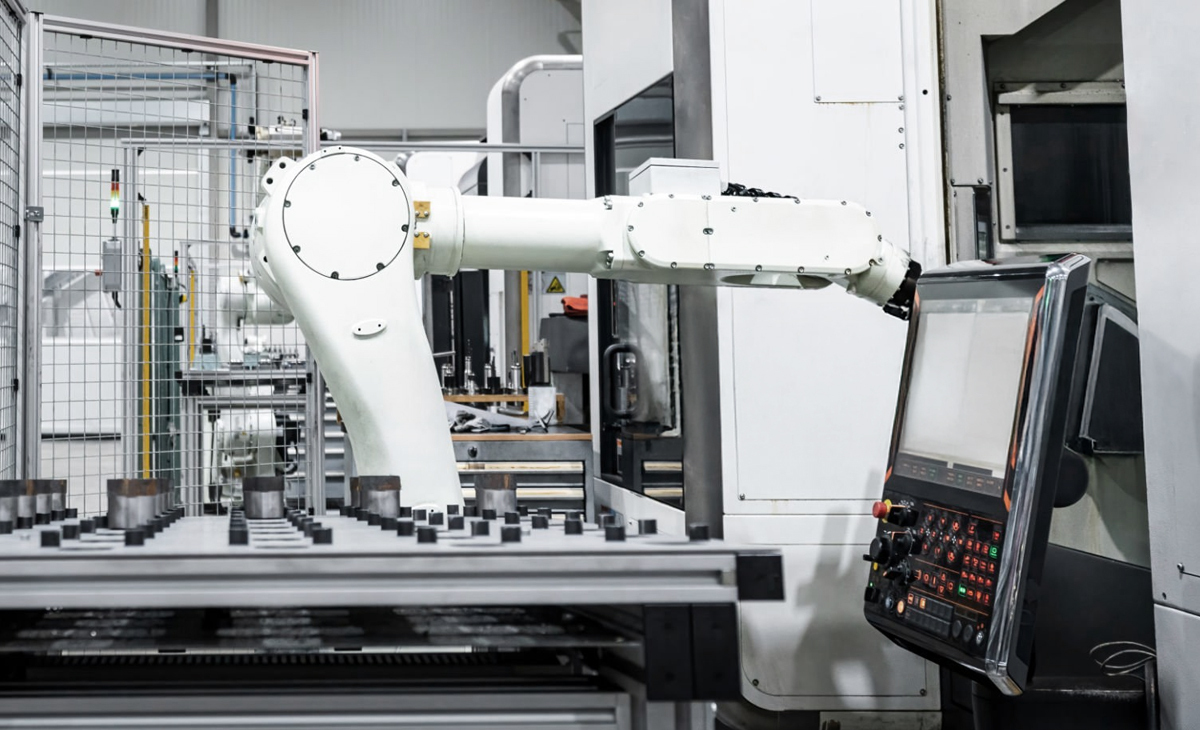
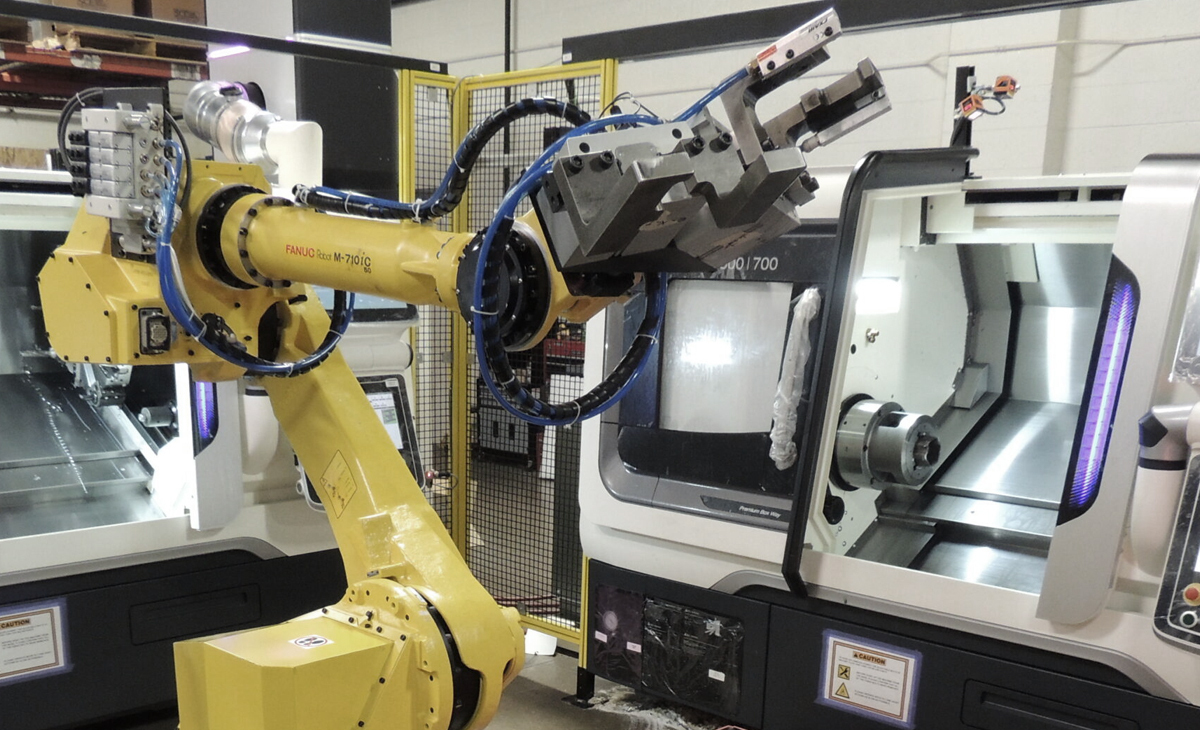
Stryker Deploys Flexxbotics to Digitalize Robotic Production at Scale in Medical Device Manufacturing

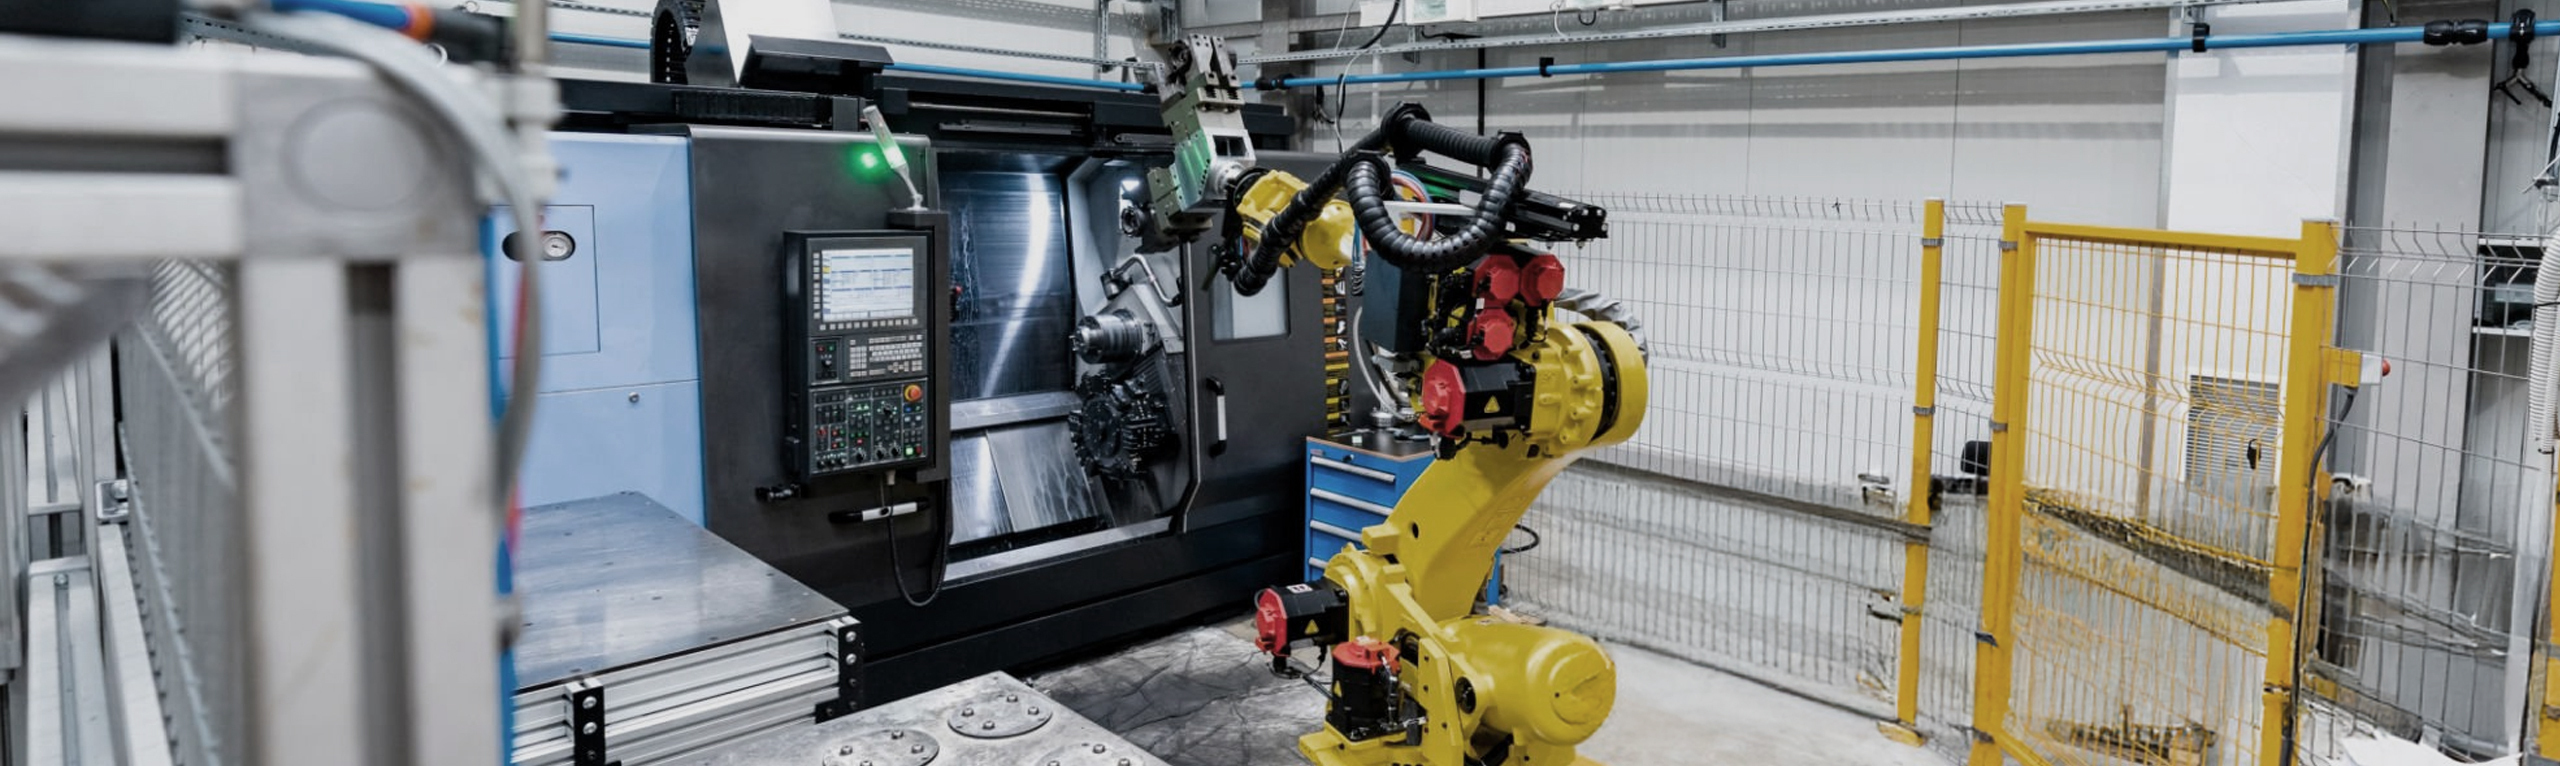
Flexxbotics, the autonomous manufacturing platform leader, today announced that Stryker, a global leader in medical technologies, has deployed Flexxbotics for advanced robotic production with automated manufacturing compliance, process trend intelligence, and autonomous process control in factory operations. Flexxbotics is enabling Stryker to increase throughput, optimize utilization, and minimize unplanned downtime across production workflows.

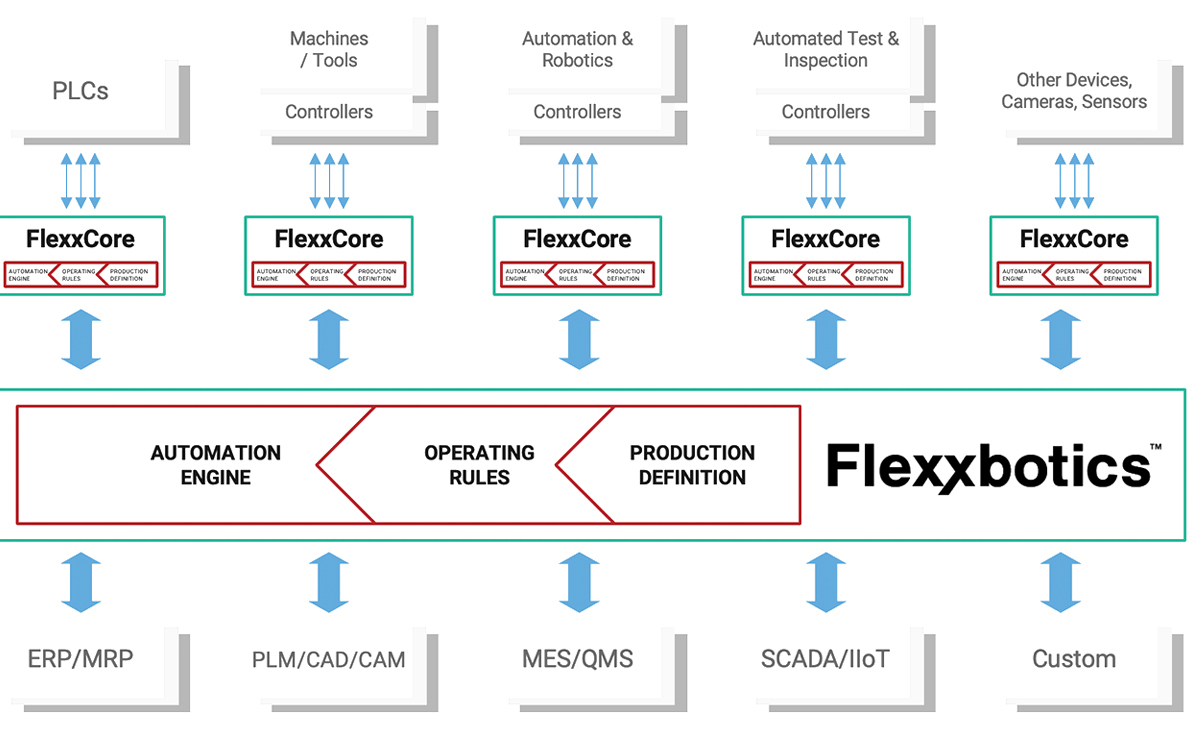
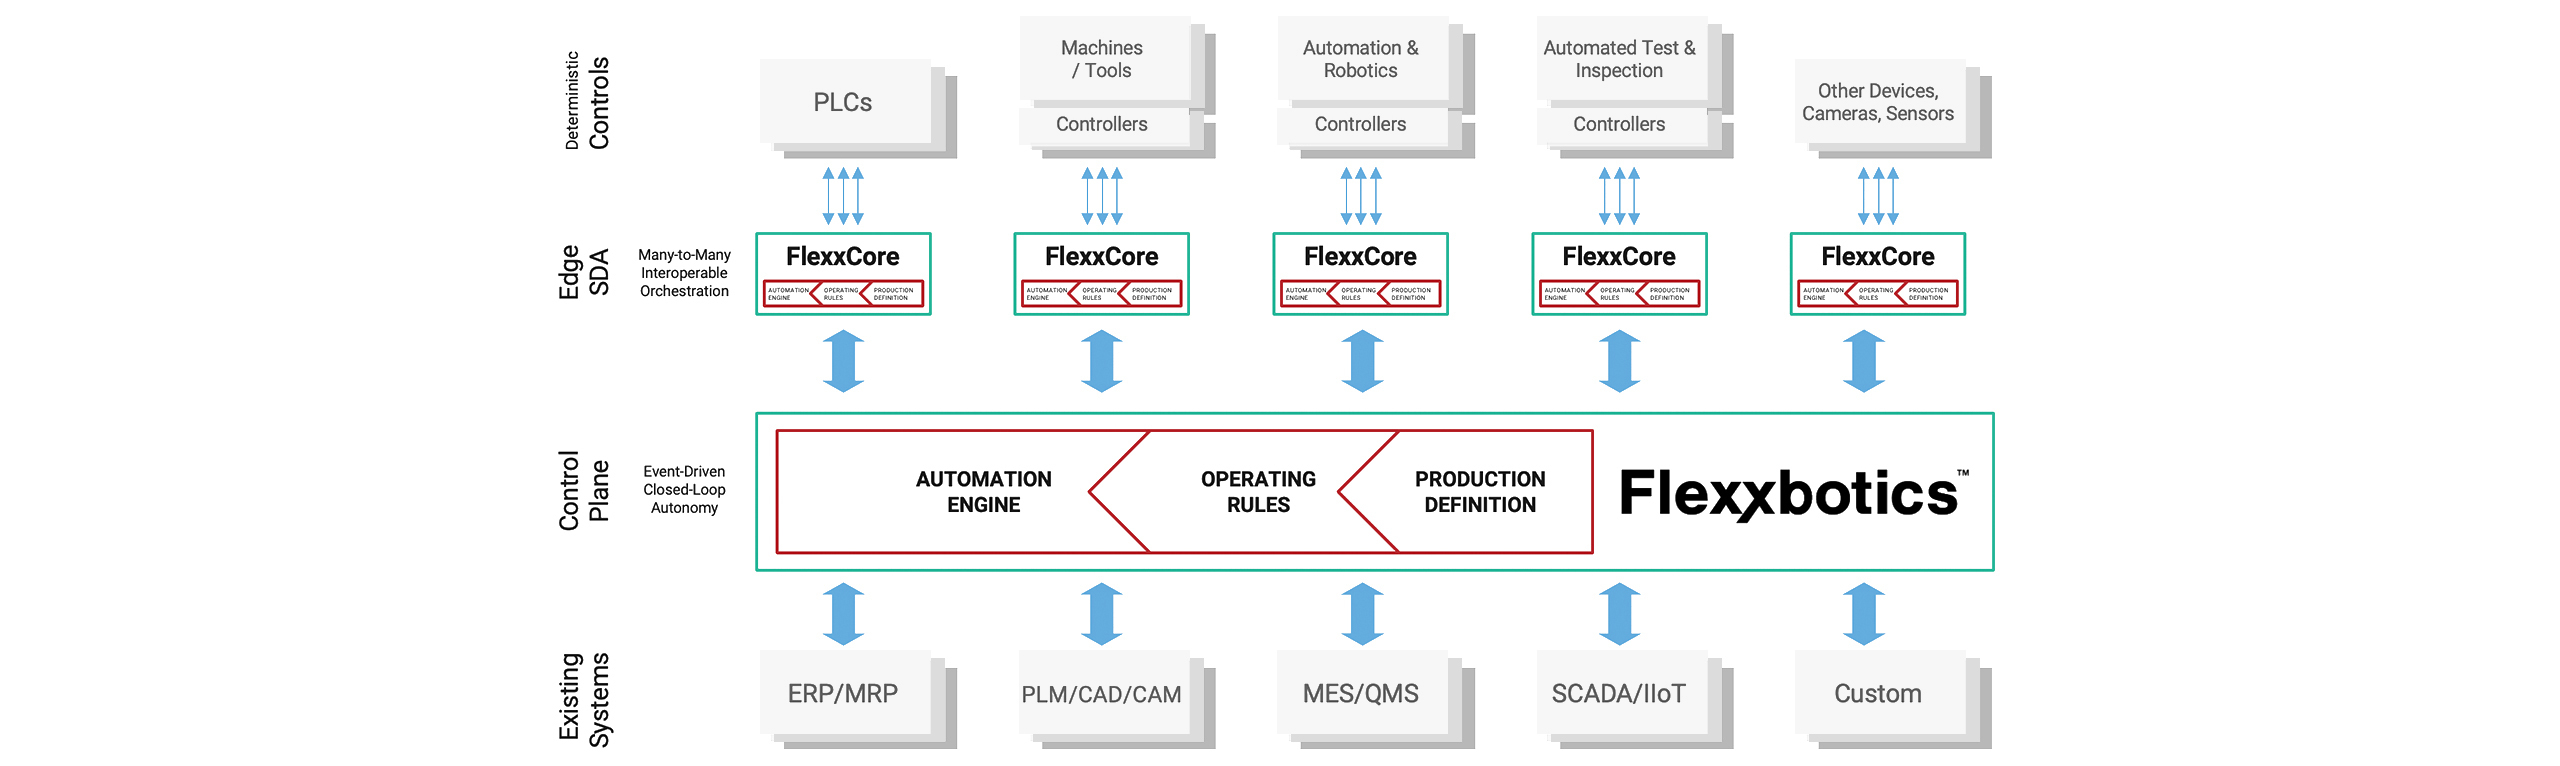
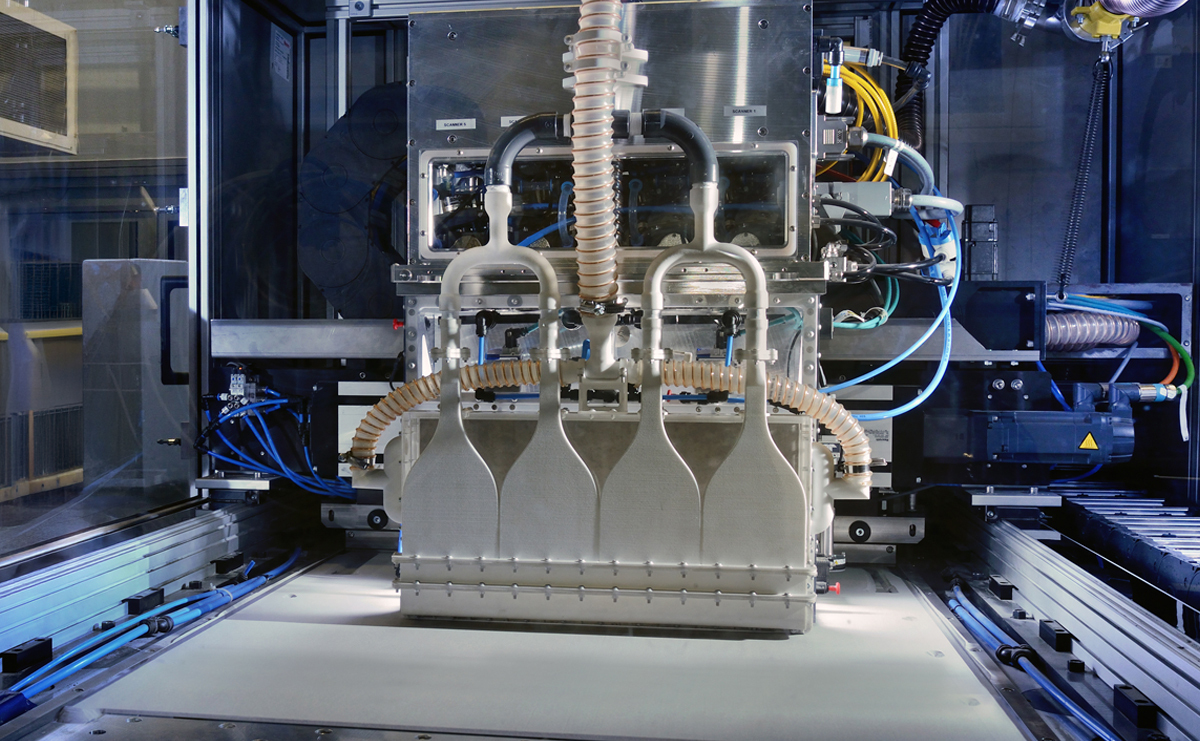
Stryker is using Flexxbotics software-defined automation to orchestrate production-critical assets in high mix volume production requiring automated changeovers. Flexxbotics platform delivers interoperability and closed-loop control across a wide range of factory equipment including production machines, robotic automation, rail systems, and numerous other advanced manufacturing technologies. This integration powers continuous operations during automated production with digital thread traceability to ensure compliance with regulatory requirements while improving operational agility.

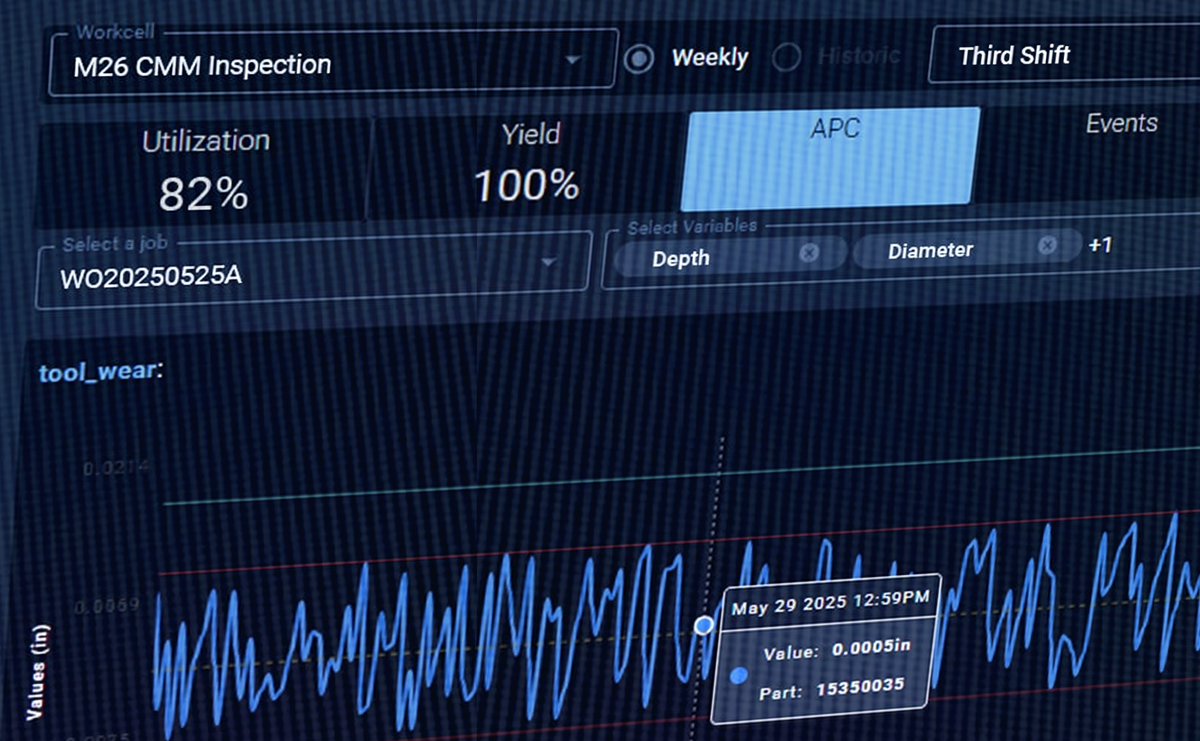
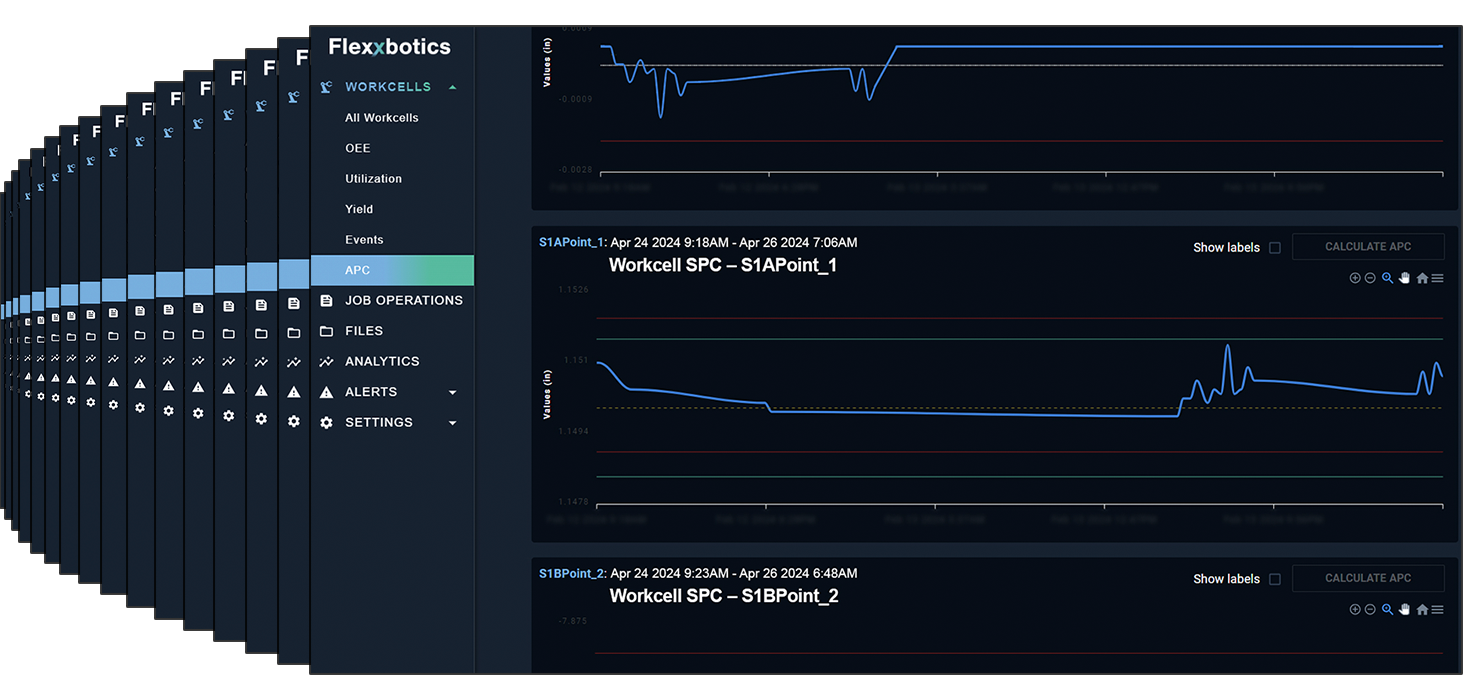
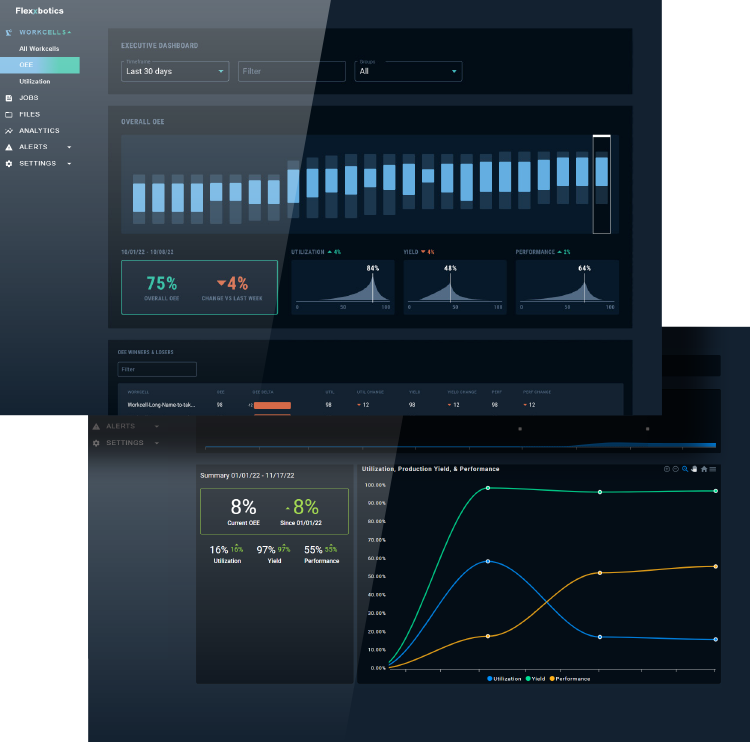
The Flexxbotics deployment enables Stryker to proactively identify process deviations and performance anomalies which improved production consistency for a 41% throughput increase with significant reductions in scrap and rework. Real-time visibility into process conditions drove a 53% improvement in utilization and a 62% reduction in unplanned downtime to increase overall equipment effectiveness and create additional production capacity.

In addition, Flexxbotics establishes a real-time data layer by integrating multi-source data from plant equipment and automation systems which establishes the closed-loop process control required for highly regulated medical device manufacturing. Parallelized data pipelines aggregate high-frequency, multimodal production data into a contextualized data foundation including machine operating conditions, robot execution data, and in-process sensor measurements. This unified dataset powers automated process adjustments, real-time compliance verification, and is structured to support Industrial AI training, validation, and inference.

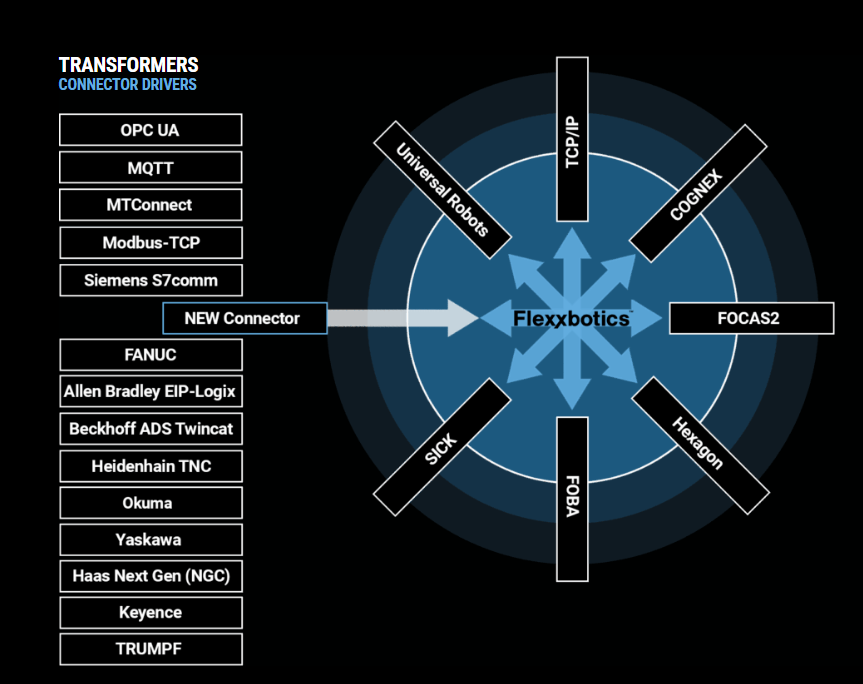
Flexxbotics establishes a scalable foundation for future automation and digitalization initiatives with open connectivity to a broad range of industrial protocols and IT systems. New equipment and workflows can be integrated rapidly, transforming automation deployment into a repeatable, standardized, and sustainable process.

“Software-defined automation is fundamentally changing how smart factories operate,” said Tyler Bouchard, CEO & Co-Founder of Flexxbotics. “We’re proud to partner with global companies like Stryker to intelligently orchestrate plant machines, robotics, and automation in real-time to achieve a more flexible and scalable foundation for autonomous manufacturing.”

About Stryker

Stryker is a global leader in medical technologies and, together with our customers, we are driven to make healthcare better. We offer innovative products and services in MedSurg, Neurotechnology and Orthopaedics that help improve patient and healthcare outcomes. Alongside our customers around the world, we impact more than 150 million patients annually. More information is available at www.stryker.com.

About Flexxbotics

Flexxbotics enables manufacturing autonomy at scale through software-defined automation. Flexxbotics autonomous manufacturing platform provides interoperable communication and orchestration across plant equipment, robotics, and enterprise IT systems. Built to be open and extensible, Flexxbotics digitalizes autonomous process control for continuous operations in next-generation smart factory environments. Visit www.flexxbotics.com to learn more and follow us on LinkedIn.

Autonomous Process Control in Factory Automation Architecture

Autonomous Process Control in Factory Automation Architecture

Autonomous-Process-Control-in-Factory-Automation-Architecture

Many of the concepts discussed in this post are drawn from techniques established in semiconductor fabrication for decades called advanced process control.

Taking these foundational methods, applying them across manufacturing for all industries, and extending them to modern smart factory environments, whether using AI or not, is the intent.

How Do I Achieve True Closed-Loop Production Autonomy Across Machines, Systems, and Processes?

As factories scale automation and introduce AI, the challenge shifts from coordinating systems to achieving consistent, real-time control of production outcomes.

Controls engineers and manufacturing automation technologists are increasingly expected to:

  • Maintain tight tolerances and quality across complex processes
  • Reduce variability, scrap, and rework
  • Improve yield and throughput continuously
  • Enable lights-out production with minimal human intervention

Yet most factories still rely on:

  • Machine-level control loops
  • Operator-driven adjustments
  • Delayed responses to process variation

The automation capabilities exist, yet the ability to execute closed-loop control across the entire production environment is not there today in most plants.

In modern factories Autonomous Process Control (APC) is the foundational building block for autonomous manufacturing. If APC can not be achieved, repeatable manufacturing autonomy is unrealistic.

This post answers the critical question:

  • How do I implement Autonomous Process Control across factory systems to achieve consistent, scalable production autonomy?

1. The Question?

How do I extend process control beyond individual machines to the entire production process?

Most factories already implement some level of process control:

  • PLC-based control loops
  • Machine-level feedback systems
  • Inspection, test, and quality checks often later in the process

Historical this mostly manual approach works:

  • Operators and inspectors monitor outputs
  • Adjustments are made manually
  • Variability is manageable

As production automation density scales, new challenges emerge:

  • Variability accumulates across machines and processes
  • Process drift is detected too late
  • Adjustments are inconsistent across cells, lines, and shifts

The question is no longer:
“How do I control this machine?”

It becomes:
“How do I continuously control production outcomes across a wide range of machines, automation systems, and processes in real-time?”

2. Why Does Process Control Break Down at Scale?

2.1 Why Is Control Limited to the Machine Level?

Traditional factory architectures concentrate control within:

  • PLCs
  • Machine controllers
  • Local feedback loops

This creates:

  • Strong local deterministic control
  • Complicated system-level coordination

Result:

  • Machines operate correctly in isolation
  • Production outcomes vary across cells, lines, and plants

2.2 Why Is There Not More Closed Loop Between Production Operations?

Most factories separate:

  • Production systems (machines, equipment, automation)
  • Inspection & test systems (automated testers, inspection, optical, CMMs, etc)
  • Factory data analysis (manufacturing, quality, maintenance event data)

This leads to:

  • Long feedback loops requiring human interpretation and intervention
  • Inspection results analyzed after production occurs
  • Adjustments applied manually or inconsistently after the fact

Result:

  • Delayed corrections and prolonged downtime
  • Increased defects, rework, and scrap
  • Missed opportunities for proactive optimization

True Autonomous Process Control requires closing this loop, where feedback directly drives production adjustments in real-time

2.3 Why Does Process Variability Persist?

Production variability is introduced by:

  • Material differences
  • Environmental conditions
  • Tool wear and degradation
  • Machine drift

Without coordinated control:

  • Variability compounds across operations
  • Intervention is reactive, not proactive
  • Adjustments do not occur continuously

Result:

  • Throughput bottlenecks and reduced output
  • Unplanned downtime
  • Inconsistent quality and yields

2.4 Why Is Human Intervention Still Required?

Most factories depend on:

  • Operator and inspector interpretation
  • Engineers analyzing and making adjustments
  • Tribal knowledge for process tuning

This creates:

  • Inconsistent responses
  • Delayed decision-making
  • Areas of dependence on a single person
  • Systemic drift and downtime risk
  • Limited ability to scale

Result:

  • Production performance is over-reliant on individuals, not systems

3. What Do Existing Approaches Miss?

3.1 What Are the Implicit Assumptions in Process Control?

Most architectures assume:

  • PLCs handle control
  • Inspection and test systems validate results
  • MES tracks production

These assumptions leave a gap:

No system is responsible for continuously aligning production behavior with throughput, uptime, and quality outcomes across the factory

3.2 Why Is Machine-Level Control Not Enough?

Machine-level control ensures:

  • Repeatability within a cycle
  • Stability within a machine

But does not ensure:

  • Consistency across machines, lines, and processes
  • Processing adjustments based on quality outcomes
  • Proactive corrections to avoid downtime
  • Optimization across the full production process

3.3 Why Does Self-Correcting Control Require a Closed-Loop Architecture?

Autonomous Process Control requires:

  • Multi-source data
  • Real-time feedback
  • Immediate adjustments or corrections

Without a closed-loop architecture:

  • Control is dependent of individuals
  • Adjustments are delayed and inconsistent
  • Scaling becomes difficult

4. What Are Modern Principles for Autonomous Process Control?

Extend Process Control Beyond the Machine

A modern factory automation architecture for autonomy must treat process control as a system-wide capability, not a machine-level function.

4.1 Closed-Loop Factory Automation Architecture

Purpose:
Continuously align production processing with output and quality requirements

Responsibilities:

  • Enable all production equipment to interoperate with continuous feedback loops
  • Feed data streams into a control plane for anomaly detection and event recognition
  • Enable real-time adjustments and corrections

Key Principle:
Process control becomes autonomous when production activities are continuously linked in a closed-loop

4.2 Contextualized Process Control

Purpose:
Ensure adjustments are applied correctly

Responsibilities:

  • Enrich multi-source production data with part, process, and equipment context
  • Characterize nominal values and control limits for every data stream
  • Apply adjustments based on actual production conditions

Key Principle:
Process adjustments must be based on characterized production data streams, not isolated signals

4.3 Real-Time Detection and Response

Purpose:
Reduce latency between condition and correction

Responsibilities:

  • Detect process drift immediately
  • Trigger adjustments without delay
  • Maintain continuous control

Key Principle:
Effective process control depends on immediate detection and response to production condition changes (minutes or seconds as opposed to hours or days)

4.4 Governed Implementation of Adjustments

Purpose:
Ensure safe and consistent control

Responsibilities:

  • Define rules, thresholds, and limits
  • Control which adjustments are allowed
  • Maintain traceability of actions

Key Principle:
Autonomous process control requires governed oversight to ensure reliability and compliance

4.5 Key Design Insight

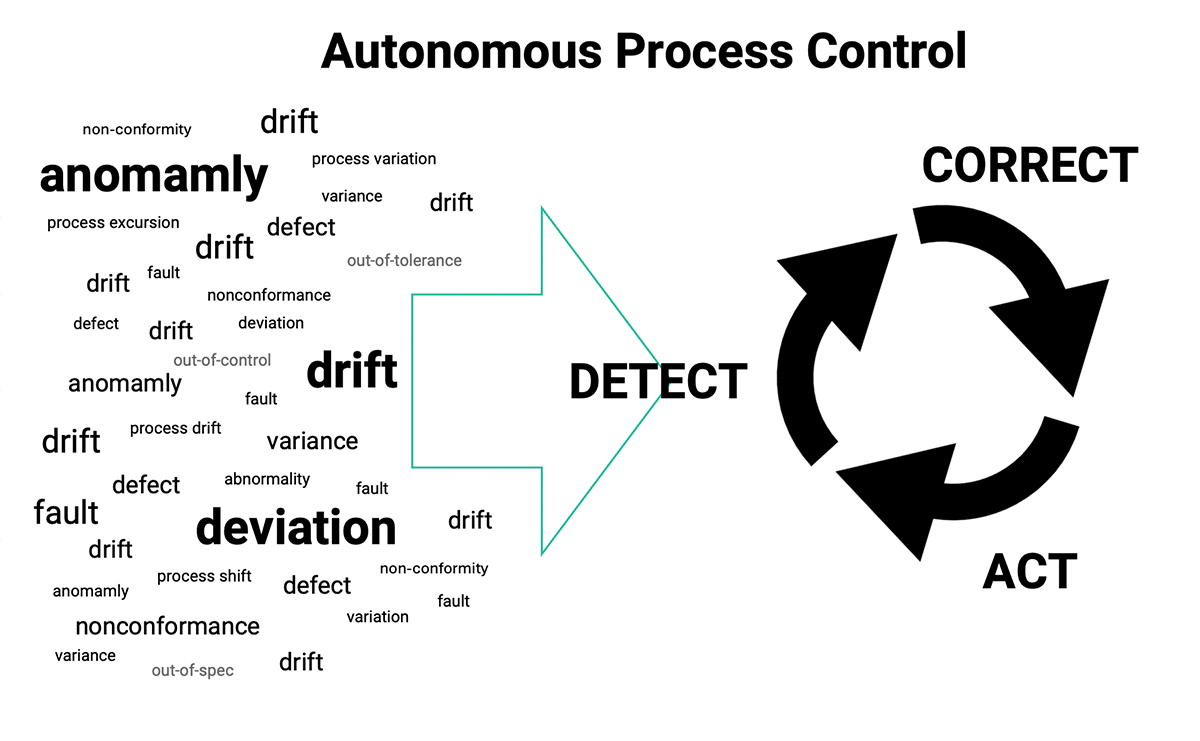
Autonomous Process Control is only possible when interoperability, orchestration, and traceability are combined into a closed-loop detect > correct > act process across the production environment

5. What Are Practical Implementation Patterns for Autonomous Process Control?

Flexxbotics enables Autonomous Process Control through an Autonomous Manufacturing Platform using a Software-Defined Automation layer + Control Plane layer

5.1 Software-Defined Automation at the Edge (FlexxCore)

Enables:

Real-Time Factory Equipment Interoperability

  • Connects machines, automation, test & inspection equipment, cameras, sensors, safety systems, and equipment for secondary operations
  • Enables direct feedback loops between all equipment during production

Contextualized Data Capture

  • Aligns machine data with part, process, job, and other production relevant context
  • Normalizes multi-source, multimodal data across heterogeneous systems

Event-Based Process Detection

  • Identifies drift, variation, and anomalies in real time
  • Triggers conditional adjustments at the source

5.2 Control Plane (FlexxControl)

Provides:

Centralized Process Governance

  • Defines operating rules, thresholds, and limits
  • Ensure consistent process control across cells and lines

Detect > Correct > Act Automation

  • Identify deviations and anomalies
  • Calculates adjustments
  • Applies authorized corrections to production variables and parameters

Cross-System Coordination

  • Aligns factory machine behavior with ERP, MES, QMS, and PLM defined specifications
  • Ensure production meets business and compliance requirements

5.3 Role of AI in Autonomous Process Control

Artificial Intelligence is not required for Autonomous Process Control, however, AI/ML can be used with governed oversight to enhance APC in range of targeted ways:

Pattern Recognition

Identify trends and anomalies across production as data streams scale and become overwhelming

Predictive Adjustment

Identify drift based on prior patterns before defects or downtime occur

Prescriptive Optimization

Recommend process adjustment improvements using insights from production observations

Controlled Introduction

Incrementally apply AI into specific production use cases with human oversight and governance

6. What Does Autonomous Process Control Enable?

6.1 From Reactive Intervention to Continuous Control

From:

  • Manual adjustments

To:

  • Continuous real-time correction

6.2 From Isolated Machines to Coordinated Production

From:

  • Machine-level control

To:

  • Factory-wide process control

6.3 From Variable Quality to Consistent Output

From:

  • Drift and variability

To:

  • Stable, repeatable production

6.4 Measurable Production Improvements

Autonomous Process Control delivers:

  • Reduced defects and nonconformances
  • Increased yields
  • Improved profitability

6.5 Foundation for Autonomous Manufacturing

APC enables:

All to support:

Autonomous Process Control as the foundation for fully autonomous manufacturing

Final Takeaway

Factories already have:

  • Machine-level control
  • Inspection systems
  • Automation infrastructure

The remaining challenge is extending control across the production environment:

How production systems continuously detect, recognize, and act to maintain process outcomes automatically

The Shift

From:

  • Machine-level control loops
  • Manual adjustments
  • Disconnected inspection and production

To:

  • Closed-loop factory-wide control
  • Real-time coordinated adjustments
  • Governed execution across systems

Factories that make the shift to Autonomous Process Control do not just improve automation performance.

They establish the capability required for greater levels of manufacturing autonomy enabling intelligent manufacturing operations at scale.

AI-Ready Factory Automation Architecture for Autonomy

AI-Ready Factory Automation Architecture for Autonomy

AI-Ready Factory Automation Architecture for Autonomy

This post is about preparing the factory automation architecture for the controlled introduction of Industrial AI using a layered approach with governance and oversight.

This is the expanded application of advanced process control principles for autonomy in manufacturing with intelligence for compliance and control.

What Industrial Automation Architecture Should Be Used for AI and Machine Learning in Production?

As AI adoption continues to grow, the challenge shifts from experimentation to safe and consistent operationalization in production environments.

Controls engineers and industrial technologists are increasingly under pressure to:

  • Apply machine learning to improve yield and throughput
  • Use artificial intelligence (AI) for predictive maintenance and quality
  • Introduce optimization across lines and plants

Yet most AI efforts stall after proof-of-concept.

The issue is the factory automation architecture required to support AI in production.

This post answers the critical question:

  • What factory automation architecture should be used for AI and machine learning in production?

1. The Question?

How do I deploy AI in a factory in a way that actually works in production?

Most factories are already experimenting with AI:

  • Computer vision systems
  • Predictive maintenance models
  • Process optimization algorithms

At small scale, this works:

  • Models run offline or in isolated environments
  • Insights are reviewed manually
  • Limited operational impact

In actual production operations, new challenges emerge:

  • AI requires consistent, high-quality data across the factory
  • Models need to observe plant activities in real-time
  • Recommendations and interactions must be applied safely and consistently

The question is no longer:

“How do I build an AI model for manufacturing?”

It’s become:

“How do I integrate AI into factory operations safely so it can provide reliable information that can improve production?”

2. Why Do AI Initiatives Fail in the Factory?

2.1 Why Is Factory Data Not AI-Ready?

Most factories have large volumes of data:

  • Machine signals and states
  • Inspection and test results
  • Production records

But:

  • Data is not contextualized
    • What part was being produced
    • What process step was occuring
    • What was the status of the tool
  • Data definitions vary across machine brands, PLCs, and systems
  • Data are incomplete or inconsistent

This leads to:

  • Poor model performance that erodes confidence
  • Extensive effort doing data preparation, cleansing, and transforms
  • Trouble meaningfully scaling models

Example:
A defect detection model may fail because:

  • Machine states are not aligned with part data
  • Process conditions are not consistently captured

Result:
AI projects spend more time preparing data than delivering value

2.2 What Happens When Industrial AI Systems are Isolated?

Most Industrial AI operates:

  • On data from weeks or months after actual production occurred
  • In separate analytics environments
  • Outside of the production environment

This creates:

  • Limited access to live machine states
  • Long lead times to correct anomalies
  • Delays in decision-making responses

Result:

  • Insights are generated but not applied
  • Engineers attempt to figure out what to do manually

2.3 Why Is There No Controlled Way to Apply AI Recommendations in the Factory?

Even when Industrial AI produces useful recommendations:

  • There is no standardized mechanism to apply them
  • No governance over when and how actions should occur
  • No traceability of data inputs or actions taken

Example:
An AI model recommends adjusting a process parameter:

  • One engineer applies it manually
  • Another ignores it
  • A third applies it incorrectly

Result:

  • Inconsistent outcomes
  • Relevance and accuracy degrade over time

2.4 Why Doesn’t AI Scale Across Lines and Plants?

AI implementations are often:

  • Built for a specific system or situation
  • Dependent on custom integrations
  • Lacking difficult to access data across the production environment

Result:

  • Repeated development and testing efforts
  • Isolated results
  • Limited production impact

3. What Do Existing Industrial AI Automation Approaches Miss?

3.1 What Are the Implicit Assumptions About AI in Manufacturing?

Most approaches assume:

  • The manufacturing system vendor’s AI will be best
  • Data lakes are sufficient for AI training and inference
  • Insights should only be manually operationalized

These assumptions ignore a critical gap:

To operationalize AI in automated production requires multi-source data context and closed-loop control with traceability across production systems

3.2 Why Is “More Data” Necessary Yet Not Sufficient?

With Industrial AI, most think:

  • Increase data collection
  • Make bigger data lakes
  • Build more models

This leads to:

  • Data swamps with unreliable data sets
  • Model sprawl, complexity, and conflicts
  • Limited operational impact

Industrial AI effectiveness depends on contextualized data and controlled application, not data volume alone

3.3 Does Industrial AI Require Governed Execution?

Yes. Using AI in manufacturing requires controlled introduction, governed operation, and managed oversight to assure issues do not arise or cascade.

AI introduces:

  • Probabilistic outputs
  • Non-deterministic behavior

Factory environments require:

  • Deterministic control
  • Predictable execution
  • Safety and compliance

Without governed orchestration and traceability:

  • AI inputs will not be understood or explainable
  • Compliance requirements cannot be demonstrated
  • Adoption will continue to be limited

4. What Are Modern AI-Ready Factory Automation Architecture Principles?

Introduce AI in Targeted Use Cases in the Factory

A modern factory automation architecture brings AI safely into the existing processes.

4.1 Contextualized Multi-Source Data Foundation

Purpose:
Provide AI with comprehensive production-relevant data

Responsibilities:

  • Enrich machine and controls data at the source with context about parts, processes, jobs, and equipment
  • Normalize data across control systems, machines, inspection, and other factory devices
  • Combine multimodal data across cells, lines, and plants

Key Principle:

AI models require contextualized production data, not raw signals

4.2 Real-Time Production Observation

Purpose:
Enable AI to observe live operations in ongoing production

Responsibilities:

  • See real-time machine states
  • Understand event-driven activities
  • Consume multi-source high-frequency low-latency data

Key Principle:

To be effective AI must observe production in real-time, using low-latency, event-driven data directly from live machine states and human decisions

4.3 Governed AI in Factory Operations

Purpose:
Control how Industrial AI can interact during production

Responsibilities:

  • Validate AI recommendations and conclusions
  • Define which actions can and cannot be applied with rules and limits
  • Maintain traceability and auditability

Key Principle:

AI generated actions should be governable, traceable, and controlled before they are executed in production

4.4 Industrial AI Across Edge and Enterprise Use Cases

Purpose:
Think of Industrial AI operationalization in layers with respect to scope and production priorities and objectives

Responsibilities:

  • Physical AI for real-time responsiveness
  • Edge AI for coordination
  • Enterprise AI for optimization

Key Principle:

Industrial AI includes machine, edge, and enterprise layers that must align with requirements for real-time responsiveness, coordination, and optimization relative to production priorities

4.5 Key Design Insight

AI becomes increasingly useful when it has full context and traceability within the overall factory automation architecture

5. What Are Practical Implementation Patterns for Industrial AI in Factories?

Flexxbotics implements this in an autonomous manufacturing platform to enable AI-ready factory automation architecture through two architectural layers in the platform: Software-Defined Automation + Control Plane

5.1 Software-Defined Automation at the Edge (FlexxCore)

Enables:

• Multi-Source AI-Ready Factory Data Capture

  • Collect high-frequency, multi-modal data from different factory equipment
  • Normalize data across protocols and systems
  • Continuously enrich multi-source contextualized data sets

• Real-Time Integration

  • Enable controlled observation of production environments
  • Provide AI systems secure insight to live machine and device states
  • Interface independent Physical AI systems in machines and devices

• AI-Assisted Interoperability

  • Accelerate development of machine connector drivers for incompatible endpoints
  • Assure consistent interoperable patterns for reliability and safety
  • Reduce agentic interfacing time significantly

5.2 Control Plane (FlexxControl)

Provides:

• Controlled Governance of Industrial AI

  • Establish conditionals and calculation baselines for process thresholds
  • Define rules and limits for when and how AI recommended actions occur
  • Maintain control over automated workflows

• Detect > Correct > Act with AI

  • Identify specific process specifications and job operations
  • Combine AI insights with rule-based sequences
  • Coordinate trigger actions across systems

• Cross-System Coordination

  • Coordinate Physical AI systems with Edge AI for synchronized operation
  • Align AI-driven recommendations with business system instructions
  • Orchestrate AI outputs with ERP, MES, QMS, and other systems

5.3 Role of AI in Production Operations

Target use cases for Industrial AI introduction in production operations

Apply AI in production with controlled rollout building confidence over time

• Pattern Recognition and Prediction

  • Detect anomalies and trends
  • Anticipate process deviations based on operational and machine conditions
  • Identify unplanned downtime conditions proactively

• Prescriptive Optimization

  • Recommend process adjustments using realtime production circumstances
  • Increase throughput by identifying inefficiencies
  • Improve yield through closed-loop feedback

• Continuous Learning

  • Refine models based on real world human decisions
  • Establish granular production feedback
  • Improve operations over runs

• Controlled Introduction

  • Introduce targeted AI use cases incrementally
  • Maintain human-in-the-loop oversight
  • Control deployment of suggested changes

6. What Does an AI-Ready Factory Architecture Enable?

6.1 From AI Pilots to Production Deployment

From:

  • Isolated experiments

To:

  • AI assisted production autonomy

6.2 Ongoing Application of AI Recommendations

From:

  • Manual interpretation

To:

  • Governed repeatable traceability

6.3 Scalable AI Across Plants

From:

  • Equipment-specific models

To:

  • Production AI capabilities for greater autonomy across factories

6.4 Foundation for Autonomous Process Control

Enabling:

All to achieve:

Autonomous Process Control across plant operations for intelligent lights out manufacturing that increases output, yields, and profitability

Final Takeaway

Your factories need more than:

  • More AI models
  • Larger data sets
  • More experimentation

They need to solve what current industrial automation architectures do not address:

How AI connects to real-time production systems in a safe and reliable way with human oversight to execute recommendations

The Shift

From:

  • AI as analytics
  • Machine isolated AI models

To:

  • AI as a governed operational component
  • Integrated within factory systems
  • Governed through the control plane

Factories that make this shift move beyond experimentation to operationalize Industrial AI where intelligence continuously improves production performance with greater autonomy

Scalable Factory Automation Architecture for Greater Autonomy

Scalable Factory Automation Architecture for Greater Autonomy

Scalable Factory Automation Architecture for Greater Autonomy

Now want to dig into the scaling challenges of creating a factory automation architecture for autonomy and what can be done.

How Do I Scale Factory Automation for Autonomy Without Creating Lock-In, Complexity, and Architectural Divergence?

As factories mature their automation installations, the challenge shifts from automating individual machines and cells to scaling the automation architecture for autonomy across lines, plants, and changing production requirements.

Controls engineers, automation engineers, and manufacturing technologists are increasingly expected to:

  • Standardize automation across multiple plants
  • Reduce one-off engineering and custom integrations
  • Support new equipment, new products, and changing production strategies
  • Improve uptime, agility, and output across operations

Yet most factory automation architectures become harder to manage as they expand.

The issue is not whether automation works in one cell or one line. It’s whether the factory automation architecture can scale, adapt, and remain governable over time.

This post answers four critical questions:

  • How do I avoid vendor lock-in across industrial systems while still delivering quickly?
  • How do I design production automation architecture for reliability, fault tolerance, and recovery?
  • How do I standardize factory automation architecture across multiple plants without over-constraining them?
  • What does a future-proof factory automation architecture look like for autonomy?

1. The Question?

How do I design a factory automation architecture that can scale across plants and adapt over time?

Most factories already have automation that works:

  • Machine and cell-specific PLC programs
  • Line workflow logic
  • Custom MES integrations
  • Plant-specific scripts and interface routines

At a relative scale, this can be manageable:

  • One plant with several lines
  • Known equipment configurations
  • A small set of experienced engineers who understand the environment

At enterprise scale, new challenges emerge:

  • Different plants with varying equipment generations and brands
  • Different product mixes and process requirements
  • Different teams implementing logic in different ways
  • Increased pressure to move faster without introducing risk

The question is no longer:

“How do I automate this machine or line?”

It becomes:

“How do I create a factory automation architecture for autonomy that can be reused, governed, and adapted across multiple production environments?”

2. Why Do Factory Automation Architectures Break Down as They Scale?

2.1 Why Does Vendor Lock-In Become a Long-Term Problem?

Many automation architectures are built around:

  • Specific PLC ecosystems
  • Single-vendor system stacks
  • Proprietary machine interfaces and protocols
  • Custom code tightly coupled to one supplier’s way of working

This can speed up an initial deployment, but over time it creates:

  • Limited flexibility when adding new machine types
  • Difficulty integrating components the vendor doesn’t offer or innovative new equipment
  • Reduced leverage in purchasing and architecture decisions
  • High switching costs and rip & replace requirements

Example:

A plant standardizes on one vendor’s control stack, and then acquires a new factory with different machines, controllers, robots, and testers.

Result:

The team either forces an expensive and disruptive equipment replacement or creates another custom layer of one-off integrations that increases complexity, operation, and maintenance.

2.2 Why Does Multi-Plant Standardization Often Fail?

Many companies try to standardize by:

  • Mandating one vendor’s control systems
  • Requiring one systems stack everywhere
  • Copying the same logic templates line to line and plant to plant

But in practice:

  • Plants have different line configurations
  • Equipment makes and model generations vary widely
  • Production process requirements differ by plant
  • Local teams make practical deviations to make production work efficiently

This leads to:

  • Architectural drift and complexity
  • Divergent implementations and logic
  • Limited reuse despite “standardization” efforts

Result:

Companies believe they have a global standard, but in reality they have local custom control software implementations running on the corporate hardware standard

2.3 Why Doesn’t Factory Automation Reliability Take Into Account Downtime Recovery?

Many architectures assume:

  • Downtime scenarios can be handled quickly manually
  • Recovery procedures can live in tribal knowledge
  • If the line is running today, the system is reliable enough

This creates problems when:

  • A system update affects production behavior in unexpected ways
  • A plant network segment fails
  • An integration service goes down
  • A data component loses sync

Result:

Unplanned downtime recovery becomes slow, inconsistent, and dependent on a few people who know how certain aspects of the system really work

2.4 Why Do Factory Architectures Become Obsolete So Quickly?

Manufacturing environments are constantly changing:

  • New machines and tooling are added
  • Existing equipment stays in service longer than expected
  • New compliance requirements are introduced
  • Production goals change

Architectures become obsolete when they are:

  • Dependent on assumptions that no longer hold true
  • Too tightly coupled and impede necessary changes
  • Built around a single vendor’s mandates that only cover a portion of the requirements

Result:

Every change causes added complexity and rework not reuse

3. What Do Existing Factory Automation Approaches Miss?

3.1 What Are the Implicit Assumptions in Scaling Automation for Greater Autonomy?

Most approaches assume:

  • Standardizing on a single vendor stack will make everything work together
  • A successful pilot architecture can be copied elsewhere
  • Standardization means forcing sameness across plants, lines, and cells

These assumptions ignore a critical gap:

Scaling factory automation for autonomy requires an architectural model that is interoperable, governable, fault-tolerant, and adaptable as different plant’s production environments change over time

3.2 Why Is “More Standardization” Not Enough?

Historical thinking includes:

  • Standardize on one PLC brand
  • Standardize on a set of function blocks
  • Standardize on a single interfacing workflow

Standardization is beneficial although becomes problematic when operational realities are disregarded leading to:

  • Unrealistic architectures that do not fit real plant requirements or variations
  • Hidden customizations that cause divergence and complexity
  • Suppressed optimization in each plant’s lines and cells causing inefficient workarounds

Standardization must take into account plant operational requirements that change over time to increase autonomy

3.3 Why Is Reuse More Important Than Uniformity?

A scalable factory automation architecture for autonomy must not force over standardization for standardization’s sake

For example, standardization of requirements for interoperability between heterogeneous equipment into the future is important to enable reuse and repeatable scaling as the factory changes

It should enable:

  • Reusable interoperability interfaces
  • Reusable orchestration and traceability patterns
  • Reusable governance models
  • Reusable recovery and deployment approaches

Without this:

  • Every plant’s lines and cells become a separate automation project irrespective of the vendor’s standard hardware
  • Engineering effort increases exponentially
  • Scaling remains slow and expensive

3.4 Why Does Future-Proofing Require Separation of Responsibilities?

Future-proofing is not about predicting future requirements.

  • It is about structuring the architecture so change can be absorbed without disrupting or destabilizing production

That requires:

  • Clear separation of deterministic control vs orchestration and traceability
  • Interoperable coordination at the edge
  • Governed operating rules and limits in the control plane

Without this separation:

New equipment, AI, and emerging business requirements keep getting forced into the wrong layers creating unmanageable complexity and scaling obstacles

4. What Are Modern Principles for Scalable and Future-Proof Factory Automation for Autonomy?

Standardize the Architecture, Not the Vendors

A modern factory automation architecture for autonomy should make plants more reliable without making them inflexible.

4.1 Open Interoperability Over Vendor Standardization

Purpose:

Enable different machines, controllers, and systems to work together without forcing the rip and replace expense and disruption required for a single-vendor stack

Responsibilities:

  • Support heterogeneous equipment and protocols while limiting proliferation
  • Reduce dependence on proprietary interfaces and custom factory code
  • Enable optimized choices over time

Key Principle:

The architecture for factory autonomy should preserve optionality while ensuring fast deployment, production reliability, agility, and maintainability – no single vendor can provide that on an ongoing basis for an entire plant environment including secondary operations.

4.2 Standardized Coordination Patterns Across Plants

Purpose:

  • Create reusable automation behavior and rules across cells, lines, and sites

Responsibilities:

  • Normalize state models, data structures, and machine interaction
  • Enable repeatable orchestration patterns and traceability rules
  • Support site-specific implementation without architectural divergence

Key Principle:

Global consistency should come from shared patterns, not identical plant configurations.

4.3 Build In Reliability, Fault Tolerance, and Recovery

Purpose: 

  • Ensure automated production can continue safely and recover quickly

Responsibilities:

  • Reduce single points of failure; especially important in autonomous processes
  • Preserve state, traceability, and recovery workflows
  • Support resilient edge operation without an internet connection
  • Make sure systems continue operating when portions of the architecture are offline or degraded

Key Principle:

  • Reliability should be designed into the architecture, not added after a failure occurs

4.4 Change-Ready Architecture for New Systems and Use Cases

Purpose:

  • Enable the factory automation environment to evolve over time

Responsibilities:

  • Enable the insertion of new equipment and inclusion of new systems
  • Support gradual introduction of AI and levels of autonomy
  • Allow operating rules and integrations to be updated without reengineering entire aspects of the stack

Key Principle:

  • Future-proofing means making change manageable, not making change unnecessary

4.5 Key Design Insight

A scalable factory automation architecture for autonomy becomes future-proof when interoperability, governance, resiliency, and adaptability are built into the structure of the system from the start

5. What Are Practical Implementation Patterns for Modern Factory Autonomy?

Flexxbotics implements this as an autonomous manufacturing platform to enable scalable and future-ready automation through two architectural layers in the platform: Software-Defined Automation + Control Plane

5.1 Software-Defined Automation at the Edge (FlexxCore)

Enables:

• Inherited Interoperability Across Equipment

Creates compatibility across PLCs, machines, robots, inspection & test equipment, camera systems, sensors, and other factory devices

  • Normalize communication across vendor protocols and systems
  • Reduce dependence on custom point-to-point interfaces

• Standardized Coordination Across Lines and Plants

Creates many-to-many machine interaction patterns for repeatable deployment

  • Supports line and cell coordination using shared interoperability models
  • Enables cell, line, and plant-specific variation without architectural fragmentation

• Resilient Edge Operation

Operates locally in the factory with existing PLCs and equipment

  • Continues functioning with or without online connectivity
  • Eliminates dependency on centralized infrastructure for continued production output

• Production Extensibility for Change

Supports the addition of new machines, equipment, and systems over time

  • Enables new asset deployment and device provisioning in the factory for new capability insertion as technology advances without restriction

5.2 Control Plane (FlexxControl)

Provides:

• Centralized Governance Across Plants

Define product and process-specific autonomy operating rules, thresholds, and conditionals

  • Maintain production governance across sites while supporting local implementation requirements

• Coordinated Recovery and Controlled Change

Provide a secure source of truth for autonomy operating rules

  • Support controlled updates to rules and responses
  • Ensure traceability of what changed, when, and why

• Cross-System Standardization

Connect ERP, MES, QMS, SCADA, and other factory systems consistently across heterogeneous tool and machine environments

  • Reduce variation in how business systems interact with production systems from plant to plant

• Foundation for Scalable Autonomy

Enable repeatable detect > correct > act workflows

  • Support expansion from local automation to plant-wide and multi-site autonomous process control

5.3 Role of AI in Scalable Factory Automation Architecture

AI can help strengthen scalability and future readiness for greater factory autonomy in focused ways:

• Faster Extension of Interoperability

Accelerate development and validation of machine interfacing connector drivers

  • Reduced engineering effort when bringing new equipment into the architecture

• Improved Pattern Recognition

Analyze behavior across plants and lines

  • Surface reusable optimization and orchestration opportunities

• Smarter Reliability and Recovery

Detect anomalies in system behavior

  • Propose process optimizations for greater throughput
  • Recommend corrective actions before downtime repeats
  • Identify continuous improvements for improved yields

• Controlled Architectural Evolution

Enable AI use cases incrementally and safely

  • Maintain human oversight and governance over AI recommendations and improvements

6. What Does the Factory SDA Control Plane Architecture Enable?

6.1 From Vendor Dependence to Interoperable Flexibility

From:

  • Tightly coupled proprietary stacks that constrict production adaptation

To:

  • Reusable multi-vendor interoperability across production environments

6.2 From Custom Implementations to Scalable Architecture

From:

  • Each plant being a one-off implementation

To:

  • Shared architectural patterns across factories, lines, and cells

6.3 From “One Employee that Knows” to Factory Resilience

From:

  • Individual tribal knowledge and manual recovery

To:

  • Structured reliability, fault tolerance, and intelligent recoverability

6.4 From Short-Term Automation to Long-Term Adaptability

From:

  • Systems that must be rebuilt as requirements change

To:

  • A change-ready foundation for autonomy, AI, and future production needs

6.5 Foundation for Autonomous Process Control

Enabling:

All to achieve:

  • Autonomous Process Control with six sigma quality across multiple lines in a global production environment with consistent uptime, increased throughput, and improved profitability

Final Takeaway

If your factories are moving away from:

  • One-off integrations
  • Vendor mandated lock-in
  • Dependence on proprietary automation stacks

They need to solve what current factory automation architectures do not address for higher levels of autonomy:

  • How to scale interoperability, orchestration, governance, and adaptability across changing plant environments

The Shift

From:

  • Rigid vendor-constrained stacks
  • Plant-specific custom automation architectures
  • Downtime recovery by a single individual’s knowledge and manual intervention

To:

  • Standardized interoperability and coordination patterns
  • Governed execution through operating rules and limits in the control plane
  • Resilient, future-ready factory automation architecture for increasing autonomy

Factories that make this shift to an SDA control plane architecture do not just make automation more scalable for greater autonomy, they create an automation architecture that can enable plants to adapt to change and support the next stage of manufacturing intelligence.

Factory Data, Context, and Closed-Loop Autonomy

Factory Data, Context, and Closed-Loop Autonomy

Factory-Data-Context-and-Closed-Loop-Autonomy-

Here we get into the inability of today’s systems to deal consistently with data from different machines with different data definitions and protocols and why that’s a problem for factory automation architectures moving to intelligence and autonomy.

The points being made here were originally identified as important for advanced process control in semiconductor manufacturing in the 1990s. We’re applying them to general manufacturing as a basis for increased autonomy.

How Do I Turn Factory Data into Real-Time Action Instead of Just Monitoring?

As factories become data-rich, the challenge shifts to acting on that data in real time with consistency and control.

Automation and controls engineers have spent years instrumenting factories with:

  • Sensors and machine signals
  • SCADA, historians, and IIoT
  • ERP, MES, QMS, and other factory systems

Yet most operations still rely on:

  • Alarms
  • HMIs and dashboards
  • Human intervention

The gap is not visibility, the gap is closed-loop execution in production.

This post answers three critical questions:

  • How do I enable closed-loop industrial automation instead of just monitoring?
  • What’s the design for a clean, contextualized factory data model for greater autonomy?
  • How do I design for event-driven versus polling-based system interactions?

1. The Question?

How do I transform factory data into coordinated, real-time action?

At a basic level, most factories already collect a lot of data:

  • PLC signals and machine states
  • Inspection and quality results
  • MES production records

At small scale, this supports:

  • Monitoring
  • Reporting
  • Manual decision-making

At larger scale, new challenges emerge:

  • High-frequency data streams that overwhelm people
  • Inconsistent data definitions across equipment and systems
  • Delays between detection and response

The question is no longer:

“How do I collect and visualize factory data?”

It becomes:

“How do I use all this factory data to automatically detect, recognize, and act across the production environment in real-time?”

2. Why Do Factory Automation Architectures Break Down?

2.1 Why Is Factory Data Not Contextualized?

Most industrial data systems capture:

  • Signals
  • Events
  • Measurements

But lack context such as:

  • What part is being produced
  • What process step is active
  • Which machine state matters

This leads to:

  • Data that are technically correct but operationally ambiguous
  • Difficulty aligning machine data with production outcomes

Example:
A temperature reading may:

  • Be within range in one process
  • Be a defect indicator in another

Without context, the same data point has different meanings

Result:

  • Engineers spend time interpreting data instead of acting on it
  • AI models lack meaningful data sets for training inputs

2.2 Why Does Monitoring Not Lead to Action?

Factories have:

  • Alarms / Alerts
  • Dashboards
  • KPI tracking

But:

  • Alarms and alerts require human intervention
  • Actions are not standardized
  • Responses vary by operator or shift

Example:
A process drift alert may:

  • Trigger manual adjustment on one line
  • Be ignored on another
  • Cause unnecessary downtime elsewhere

Result:

  • Inconsistent responses
  • Delayed corrections
  • Increased variability in production

2.3 Why Do Polling-Based Architectures Fall Short?

Many systems rely on:

  • Periodic polling of machine data
  • Batch updates to higher-level systems

This creates:

  • Latency / elongated periods between event and response
  • Missed transient conditions
  • Inefficient data handling

Result:

  • Slow reaction times
  • Inconsistent intervention
  • Inability to support real-time coordination

2.4 Why Is There No Closed-Loop Execution Across Different Factory Systems?

Control loops typically exist at:

  • The machine level (PLC)

But not at:

  • The line, plant, or multi-cell level

This means:

  • Detection happens in one system
  • Decision happens in another
  • Action happens manually

Result:

  • Broken feedback loops
  • Inconsistent actions
  • Limited ability to optimize across the factory

3. What Do Existing Factory Automation Approaches Miss?

3.1 What Are the Implicit Assumptions in Industrial Automation and Data Systems?

Most architectures assume:

  • PLCs = Control
  • Data platforms = Visibility
  • MES = Tracking and workflows

These assumptions leave a gap:

No system is responsible for turning multi-source data into coordinated, real-time action across the production environment

3.2 Why Is Data Aggregation Not Enough?

Common approaches focus on:

  • Centralizing data
  • Building dashboards
  • Doing analytics

This results in:

  • Insight without execution
  • Delayed decision-making
  • Dependence on manual intervention

Data aggregation improves visibility but does not enable automated action for greater autonomy.

3.3 Why Does Closed-Loop Factory Autonomy Require Architecture, Not Just Logic?

Closed-loop factory automation requires:

  • Contextualized data
  • Real-time event handling
  • Coordinated execution across systems

Without a control plane in the factory architecture:

  • Logic becomes fragmented
  • Execution becomes inconsistent
  • Scaling is difficult and complex

4. What Are Modern Factory Automation and Data Principles for Autonomy?

Think of Data, Context, and Action Together

A modern factory autonomy architecture treats:

  • Data
  • Context
  • Action

As interconnected and interdependent, not separate layers or systems.

4.1 Contextualized Data Model

Purpose:
Align machine data with production meaning / intent

Responsibilities:

  • Map signals to parts, processes, and equipment
  • Normalize definitions across systems
  • Enable consistent semantics

Key Principle:

Data must be contextualized at the point of use / generation, not just stored centrally and tagged later.

4.2 Event-Driven Execution Model

Purpose:
Enable real-time responsiveness

Responsibilities:

  • Detect production events as they occur
  • Trigger decisions and actions immediately
  • Reduce reliance on the one engineer that can interpret polling data

Characteristics:

  • Low latency
  • High responsiveness
  • Scalable across factories

4.3 Closed-Loop Factory Automation Autonomy

Purpose:
Execute coordinated actions across cells, lines, and stations factory-wide

Responsibilities:

  • Detect conditions
  • Apply rules and conditionals
  • Trigger machine and system responses

Key Principle:

Closed-loop automation for autonomy extends beyond the machine to the entire production environment

4.4 Key Design Insight

Factory data becomes more valuable when it is contextualized at the source and directly feeds governed action

5. What Are Practical Implementation Patterns for Modern Factory Autonomy?

Flexxbotics implements this as an autonomous manufacturing platform to enable closed-loop automation through two architectural layers in the platform: Software-Defined Automation + Control Plane

5.1 Software-Defined Automation at the Edge (FlexxCore)

Enables the edge for:

Multi-Source Factory Data Capture

  • Collects high-frequency data from machines, PLCs, sensors, automation, robots, inspection systems, safety PLCs, and other factory equipment
  • Normalizes data across protocols, tags, and systems

Contextual Data Alignment

  • Associate machine data with:
    • Part or product being made
    • Process, job, and work order being executed
    • Equipment, tools, and fixtures being used

Event Detection at the Source

  • Identify granular production conditions in real-time
  • Reduce latency compared to centralized polling

5.2 Control Plane (FlexxControl)

Provides:

Centralized Context and Rules for Autonomy

  • Define production rules, thresholds, and conditionals
  • Maintain production business rules on a cell-by-cell basis across plant

Detect > Correct > Act Execution

  • Detect process deviations and anomalies
  • Determine adjustments and corrections
  • Apply authorized updates in real-time

Cross-System Coordination

  • Aligns actions with production requirements for quality and output
  • Connects ERP, QMS, MES, SCADA consistently with different machine-level systems

5.3 Role of AI in Closed-Loop Automation

AI can be used to enhance specific areas in secure and controlled ways:

Data Enrichment and Pattern Detection

  • Identify trends and anomalies across multi-source, multimodal data

Prescriptive Optimization

  • Provide insights to improve output
  • Suggest process adjustments to maintain quality
  • Recommend actions to avoid downtime

Targeted AI Introduction

  • Maintain human-in-the-loop control
  • Apply AI to specific areas in secure ways with traceability
  • Action recommendations only when validated and approved

6. What Does The Factory Control Plane + SDA Architecture Enable?

6.1 From Monitoring to Action

From:

  • Alarms, alerts, and dashboards

To:

  • Real-time automated responses

6.2 Consistent Production Behavior

From:

  • Operator-dependent decisions

To:

  • Repeatable closed-loop actions

6.3 Faster Response to Process Variations

From:

  • Delayed intervention

To:

  • Immediate detection and correction

6.4 Foundation for Autonomous Process Control

Enables:

  • Process trend intelligence
  • Automated manufacturing compliance
  • Robotic production
  • Factory AI data acquisition

Together these support:

Autonomous Process Control in the production environment for greater manufacturing autonomy, increased throughput, and better yields

Final Takeaway

Factories already have alarms, dashboards, and data lakes. The architectural gap lies in solving what current factory automation architectures do not address:

How to turn data into contextualized, coordinated, real-time action across the plant

The Shift

From:

  • Data collection and monitoring
  • Polling-based, delayed responses

To:

  • Event-driven actions
  • Closed-loop automation across factory machines and systems
  • Governed execution through the control plane

Factories that make this shift move beyond visibility to true operational intelligence where data continuously drives action, and actions continuously improves production operations.

Interoperable Orchestration in Factory Automation Architecture

Interoperable Orchestration in Factory Automation Architecture

interoperable-orchestration-in-factory-automation-architecture-lg

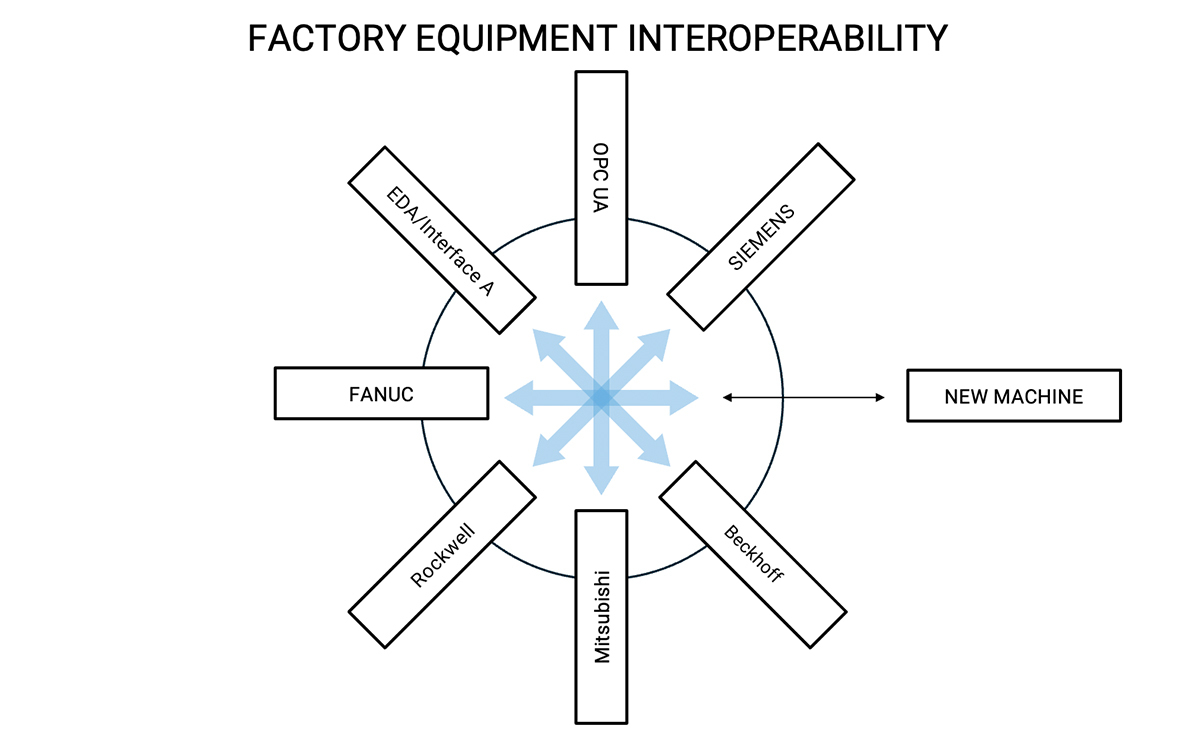
In this post we’ll take a look at the issue with factory equipment and machines that have incompatibilities and what that does to factory automation architecture particularly for increased manufacturing autonomy.

Many of these problems have been identified in semiconductor manufacturing because they would make advanced process control impossible if not addressed.


How Do I Integrate and Coordinate Multi-Vendor Factory Equipment Without Creating an Overly Complex Architecture?

Every modern factory connects machines, what engineers struggle with is coordinating them at scale.

Automation and controls engineers are increasingly asked to deliver systems where factory machines and tools, automation, robots, test & inspection systems, and enterprise software operate as a cohesive production system, not isolated automation silos.

Yet most factory architectures still rely on custom control system patterns that were never designed for this level of complexity or scale.

This post answers three critical questions:

  • How can multi-vendor equipment be integrated without complex custom point-to-point integrations?
  • How can I design for scalable interoperability across machines, lines, and plants?
  • How can legacy plant equipment be connected in a modern factory autonomy architecture?

1. The Question?

How do I integrate and orchestrate heterogeneous factory equipment at scale?

At smaller scale, integration can be complex but manageable:

  • One PLC connected to one machine and a robot
  • One inspection system feeding a QMS

At scale, the problem changes:

  • Dozens of machine types
  • Multiple types of PLCs across plants
  • Robots, vision systems, lasers, sensors
  • MES, QMS, ERP, and other custom systems

The question is no longer:

“How do I connect this machine?”

It becomes:

“How do I coordinate behavior across all these machines and systems in real time?”

2. Why Does Industrial Automation Become a Problem at Scale?

2.1 How Does Point-to-Point Integration Break Down?

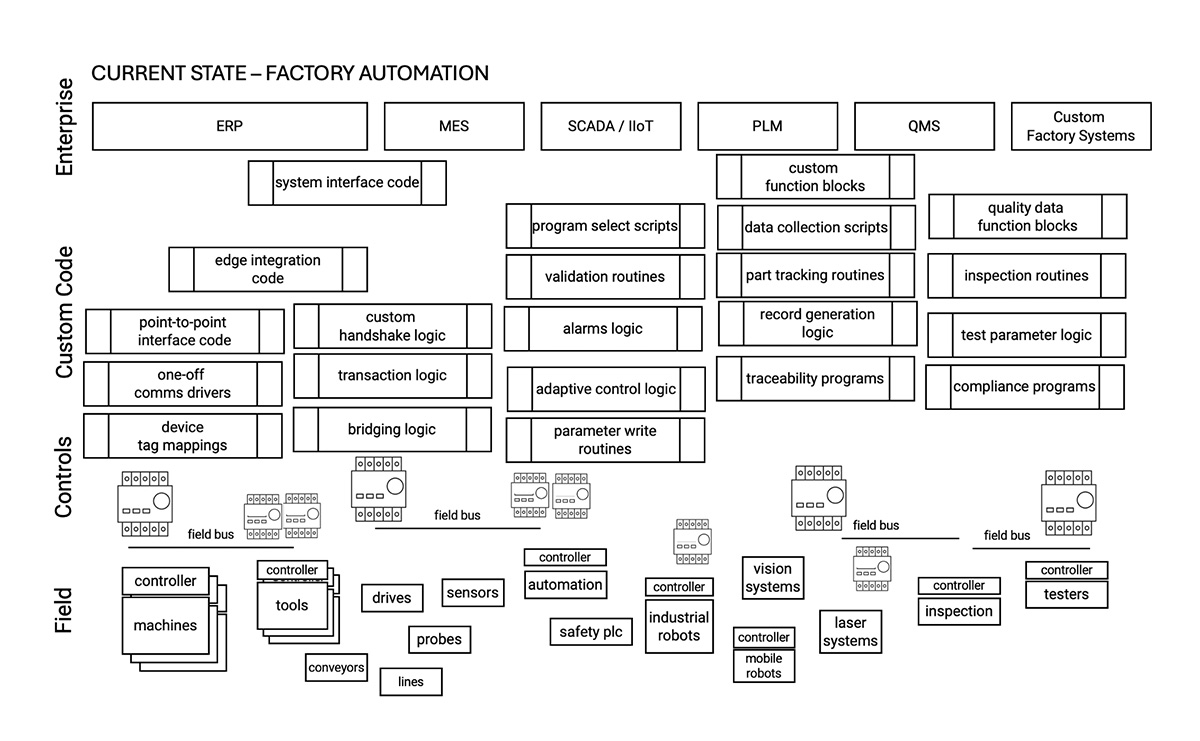
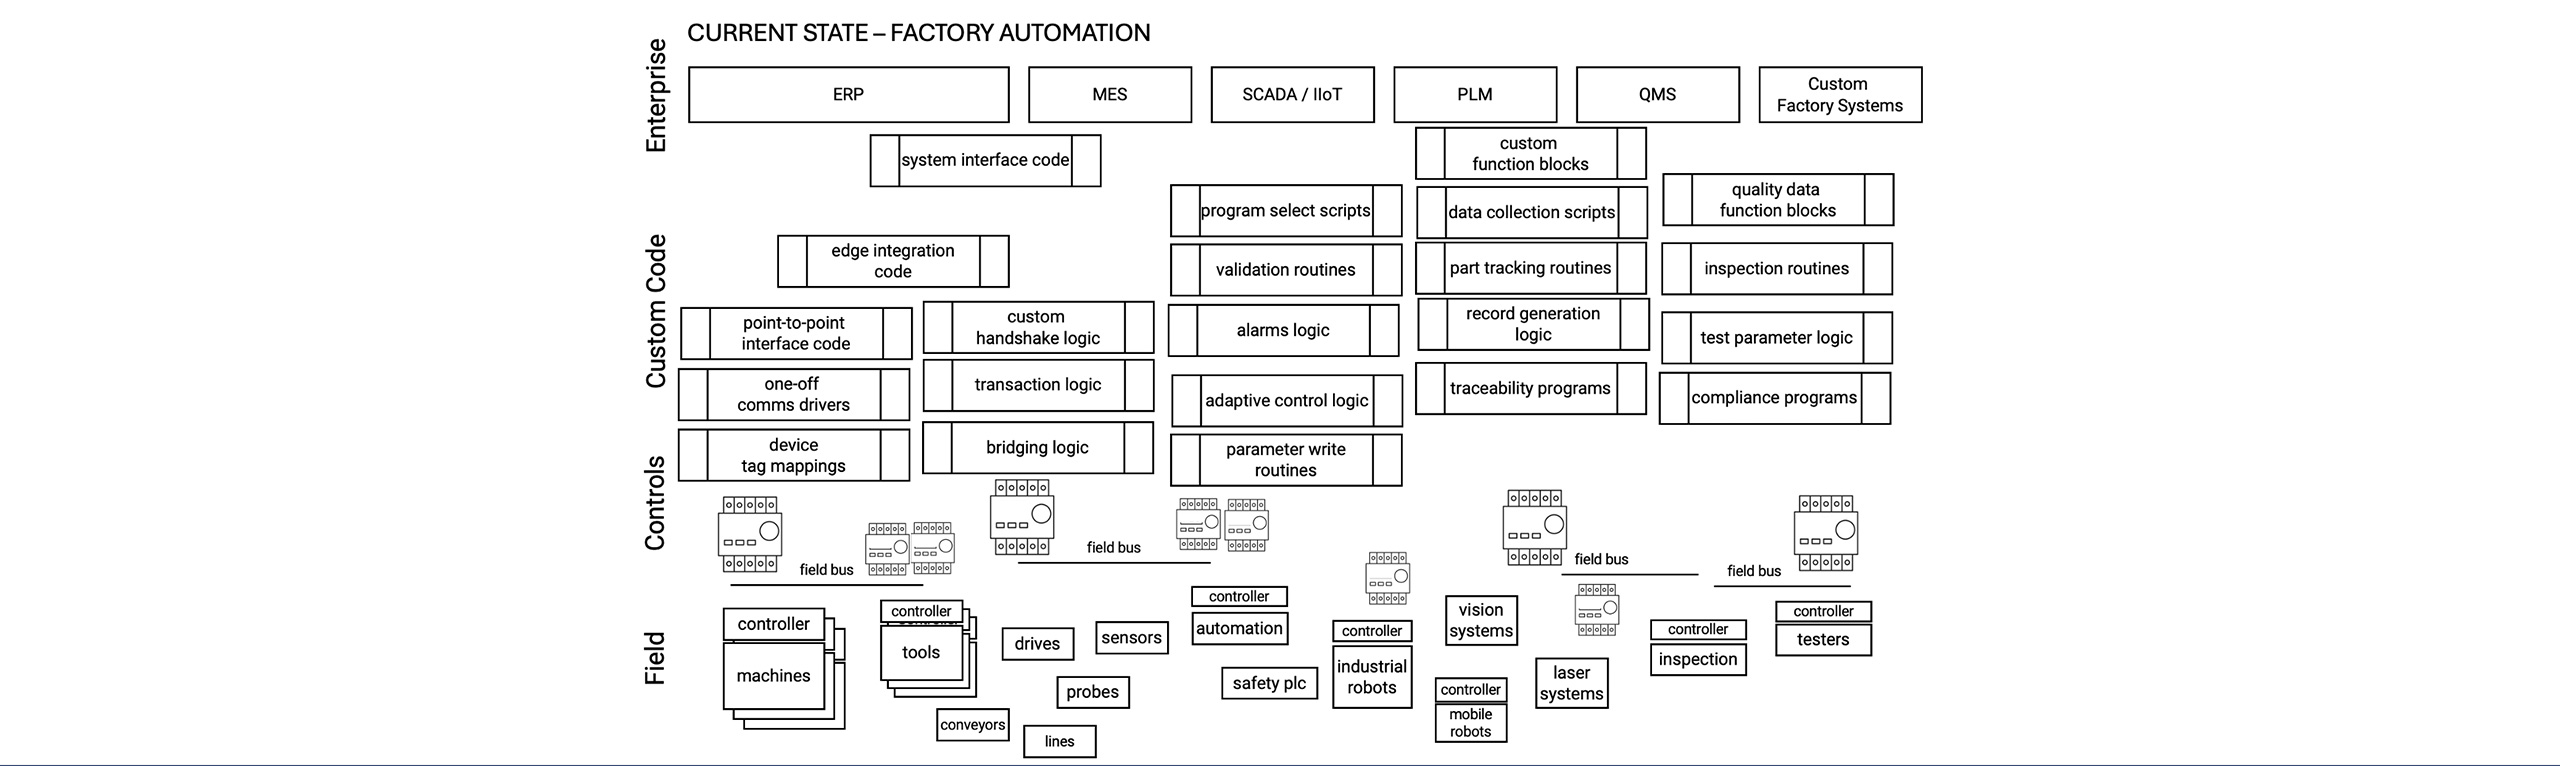
Most factories evolve into automation architectures built on:

  • Custom scripts and handshake logic
  • Protocol adapters and one-off comms drivers
  • Individual system interface integrations with data transforms

This leads to:

  • Exponential integration growth
    • N systems requires N² connections
  • Hard coded tight couplings between equipment and systems
  • High maintenance complexity and an inability to adapt quickly

Example:
Adding a new automation controller may require:

  • PLC logic changes
  • Bridging logic adjustments
  • Data pipeline modifications
  • MES integration updates

Each addition disproportionately increases system complexity and fragility.

2.2 Why Is There No Shared Operational Context?

Even when systems are connected:

  • Different types of machines have different definitions of state
  • Systems interpret data differently
  • There is no unified definition of:
    • Part
    • Process
    • Event

Result:

  • Inconsistent behavior across lines and automation cells
  • Difficult root cause analysis
  • Limited cross-machine coordination

2.3 Why Does Legacy Equipment Amplify Complexity?

Most factories include:

  • Some 10–20+ year-old machines and equipment
  • Proprietary and undocumented protocols
  • Some with limited or no modern interfaces

This forces engineers into:

  • Custom drivers
  • One-off integrations
  • Manual data extraction

Result:
Each factory’s architecture complexity is compounded by the older equipment

2.4 Why Does Integration Solve Connectivity but Not Coordination

Traditional approaches successfully deliver:

  • Machine connectivity
  • Data acquisition

But fail to enable:

  • Machine-to-machine coordination
  • Factory-wide orchestration
  • Consistent production automation execution

3. What Do Existing Industrial Automation Approaches Miss?

3.1 What are Historical Industry Assumptions?

Industrial architectures assume:

  • PLCs handle machine control
  • MES handles production workflows
  • SCADA and IIoT platforms handle data

But no system is responsible for:

Coordinating interactions across machines, equipment, and systems in real time; that’s handled by custom code if handled at all.

3.2 Why is The Real Problem Many-to-Many Orchestration?

Factory automation is not:

  • One MES > many machines

It is:

  • Many machines <> many systems <> many processes

This creates a fundamentally different challenge:

Interoperability is not a connectivity problem, it is an orchestration problem

3.3 Why Does Many-to-Many Orchestration Matter?

Without interoperable orchestration:

  • Machines and automation cannot respond to each other dynamically
  • Process adjustments remain localized and isolated
  • Cross-line optimization is difficult and manual
  • Scaling requires re-engineering integrations

4. What Are Modern Factory Automation Autonomy Architectural Principles?

Separate Interoperability and Orchestration and Make Them Software-Defined

A modern factory automation architecture for autonomy requires two distinct but connected capabilities:

4.1 Interoperability & Line/Cell Coordination (Edge)

Purpose:

  • Enable communication for interoperability across machines, PLCs, tools, equipment, and automation

Characteristics:

  • Supports all major industrial protocols
  • Extends to legacy equipment
  • Operates in real time at the edge

4.2 Orchestration for Autonomy (Control Plane)

Purpose:

  • Coordinate behavior across plant assets, machines, and systems separate from deterministic control

Characteristics:

  • Applies process rules and conditionals
  • Normalizes and contextualizes data
  • Automates and governs actions and corrections

4.3 Key Design Insight

True coordination emerges when interoperability is combined with orchestration that doesn’t effect deterministic control

This is the missing capability in most factory architectures today.

5. What Are Practical Implementation Patterns for Modern Factory Autonomy?

Flexxbotics implements this as an autonomous manufacturing platform through two architectural layers in the platform: Software-Defined Automation + Control Plane

5.1 Software-Defined Automation at the Edge (FlexxCore)

Runs at the edge to enable:

Universal Factory Equipment Interoperability

  • Connects PLCs, machines, automation, robots, inspection systems, testers, vision systems, sensors, safety PLCs, and other factory devices including legacy equipment
  • Normalize communication and data across protocols

Many-to-Many Connector Drivers

  • Comms drivers that inherent compatibility across all endpoints
  • Extendable using AI-assisted development

Real-Time Line/Cell Coordination at the Edge

  • Machines and PLCs exchange states and signals directly
  • Supports coordinated behavior across devices

Example:
A factory machine, robot, and vision system can:

  • Share inspection results
  • Adjust process parameters or variables
  • Coordinate actions without custom scripts, routines, or programs

5.2 Control Plane (FlexxControl)

Orchestrates the software-defined automation at the edge to enable:

Centralized Autonomy Rules and Limits

  • Repository for thresholds, triggers, and process conditionals
  • Enables automated production business rules to scale out across cells and lines

Detect > Correct > Action

  • Observe and recognize production condition changes
  • Trigger updates and responses
  • Safely make variable and parameter adjustments

Cross-System Interfacing

  • Connects MES, QMS, ERP consistently with all types of machine-level systems

5.3 Role of AI in Interoperable Orchestration

The architecture enables the option to introduce AI in targeted use cases safely and without rip & replace disruption:

Accelerated Machine Interfacing

  • Develop, extend, and test machine interfacing connector drivers
  • Cut controller integration time significantly; 22x faster than custom point-to-point

Multi-Source Data Capture

  • High-frequency, multi-modal production data
  • Continuous contextual enrichment

Controlled AI Deployment

  • Introduce AI use cases incrementally with human-in-the-loop control
  • Engineers and managers govern which AI recommendations get acted upon

6. What Does The Factory Control Plane + SDA Architecture Enable?

6.1 Scalable Interoperability

From:

  • Custom integrations for each machine’s controller

To:

  • Reusable, extensible connectivity across all factory equipment

6.2 Coordination of Production Autonomy

From:

  • Isolated machine control

To:

  • Real-time coordination across machines and systems

6.3 Reduced Engineering Overhead

From:

  • Rebuilding integrations per line/cell

To:

  • Consistent automation architecture across cells, lines, and plants

6.4 Foundation for Autonomous Process Control

Interoperable orchestration enables:

  • Process trend intelligence
  • Automated manufacturing compliance
  • Robotic production
  • Factory AI data acquisition

All to support:

Autonomous process control in production operations

Final Takeaway

Companies can build on existing investments in PLCs, deterministic control, and automation while solving what those systems were never designed to do:

Coordinate, orchestrate, and govern behavior across heterogeneous factory machines and systems

The Shift

From:

  • Point-to-point integration
  • Machine-level control

To:

  • Many-to-many Interoperable orchestration at the edge
  • Business system-driven coordination through the control plane

Factories that solve this problem will not just enable greater manufacturing autonomy, they will enable the next level of intelligent adaptation in their production environments.

Flexxbotics SDA runtime, studio, and API are freely available at: https://flexxbotics.com/download/
Factory Autonomy Architecture Foundations

Factory Autonomy Architecture Foundations

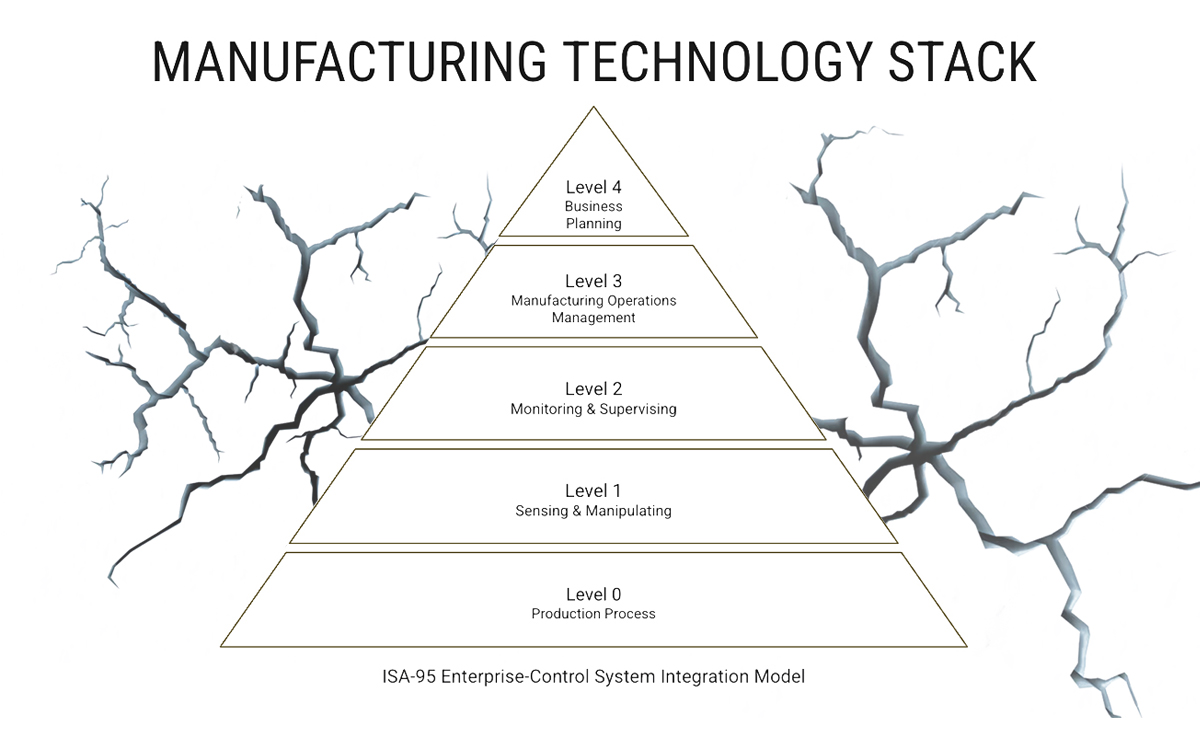
Manufacturing Technology Stack

This post explores the breakdown in traditional factory automation architecture for greater levels of autonomy and what patterns and principles can be used for the next era of factory intelligence.

These concepts draw on techniques used for decades in semiconductor fab called advanced process control.

How Should I Structure My Overall Manufacturing Automation Architecture for Greater Autonomy?

Modern manufacturing systems lack architectural clarity at scale, despite having robust control systems.

Automation and controls engineers are being asked to design systems that span:

  • Machines and PLCs
  • Automation and inspection systems
  • MES, QMS, ERP, and enterprise software

Most factories have all of these components. What they don’t have is a coherent architectural model that defines how they should work together.

This post answers four critical questions:

  • How do I structure my overall manufacturing automation architecture?
  • What is the role of PLC function blocks versus higher-level software?
  • How do I ensure real-time performance and deterministic control across systems?
  • What is the role of MES in a modern industrial automation architecture?

1. The Question?

How should a modern factory automation architecture be structured for autonomy?

At a basic level, most factories already follow a layered model:

  • Machines and PLCs at the control level
  • Supervisory systems and HMIs
  • MES and enterprise systems

Historically, this works, yet in today’s rapidly unfolding advancement toward greater manufacturing autonomy it is incomplete.

At scale, engineers encounter new challenges:

  • Multiple lines with different asset configurations
  • Mixed generations of equipment and machines
  • Increasing demand for coordination and adaptability

The question is no longer:

“How do I control this machine or line?”

It becomes:

“How do I structure the entire factory as a coordinated system while preserving deterministic control?”

2. Why Does Factory Architecture Break Down at Scale?

2.1 Why Do Industrial Architectures Become Blurry?

Traditional models (e.g. ISA-95) define layers:

  • Level 0–2: Machines, sensors, and control
  • Level 3: Manufacturing operations (MES/MOM)
  • Level 4: Enterprise systems

In practice:

  • Responsibilities overlap
  • Control blurs between layers
  • Systems take on roles they were never designed for

Example:

  • PLCs handling coordination and compliance logic across multiple lines
  • MES attempting to control real-time logic behavior
  • Bridging gaps with custom function blocks, programs, and scripts

Result:

  • Unclear control-level ownership
  • Difficulty troubleshooting and analyzing root causes
  • Inconsistent execution and prolonged periods when unplanned downtime occurs

2.2 Why Does Control Logic Fragment Across Industrial Systems?

Control logic ends up distributed across:

  • PLC function blocks
  • Automation programs
  • MES workflows
  • Custom scripts and integration handshakes

This creates:

  • Conflicting thresholds and conditionals
  • Divergent control routines
  • Multiple sources of truth
  • Hard-to-maintain logic paths

Example:
An automated process limit deviation may:

  • Trigger a PLC stop on one line
  • Generate an MES alarm on another
  • Require a human check and intervention on a third

Result:

  • Factory programs that are only understood by one person
  • Inconsistent production output because of downtime
  • Increased engineering resources, cost, and time

2.3 Why Do Real-Time and Non-Real-Time Systems Clash?

Factories must balance:

  • Deterministic control (millisecond-level timing)
  • Higher-level coordination (seconds to minutes)

Problems arise when:

  • Non-real-time systems attempt to oversee real-time control directly
  • Real-time systems are overload with non-deterministic responsibilities

Results:

  • Performance, efficiency, and utilization degradation occur
  • Downtime increases affecting production output
  • Quality and yield issues increase
  • Safety problems happen

2.4 Why Does MES have Overload Problems?

In many cases MES is expected to:

  • Track automated production
  • Manage line/cell operations
  • Coordinate machines and equipment
  • Enforce process rules and limits

In reality:

  • MES systems are not designed for real-time orchestration
  • They lack direct interaction with machine control loops

Result:

  • Either over-reliance on MES in real-time scenarios leading to latency issues and process problems
  • Incomplete or inconsistent data which leads to a lack of trust in management

3. What Do Existing Industrial Automation Approaches Miss?

3.1 What Are the Implicit Assumptions in Industrial Automation?

Most factory architectures assume:

  • PLCs = machine control
  • MES = production management
  • SCADA/IIoT systems = data and analytics

These assumptions are valid but incomplete.

What is missing is:

A defined architectural platform responsible for coordinating behavior – rules and limits – across systems without violating deterministic control boundaries

3.2 Why Is “More Integration” Not the Answer?

When gaps appear, teams often:

  • Add custom handshake logic
  • Extend PLC function blocks
  • Program one-off MES workflows

This increases:

  • Complexity and points of failure
  • Interfacing and tight couplings
  • Maintenance burden and complexity

Custom integration fills gaps temporarily, but does not resolve architectural ambiguity and complexity.

3.3 Why Does Factory Architecture Need Clear Boundaries?

A scalable industrial architecture requires:

  • Clear separation of responsibilities
  • Defined interaction patterns between PLCs and factory systems
  • Preservation of deterministic control where required

Without this:

  • Systems compete for control
  • Custom PLC logic skyrockets, diverges, and becomes fragmented
  • Scaling becomes exponentially complex and difficult

4. What Are Modern Factory Autonomy Architectural Principles?

Define Clear Roles Across Factory Software Layers

A truly modern factory architecture does not require replacing a lot of existing systems and PLCs; it clarifies their roles.

4.1 Deterministic Control Layer (PLCs & Machines)

Purpose:

  • Execute real-time, deterministic control

Responsibilities:

  • Machine-level sequencing
  • Time-critical operations
  • Motion control
  • Safety systems

Key Principle:

Deterministic control remains at the machine level and should not be compromised.

4.2 Interoperability & Coordination Layer (Edge)

Purpose:

  • Enable communication and coordination across machines, automation, and devices

Responsibilities:

  • Normalize communication, function calls, and data structures across protocols
  • Share different machine state definitions across systems
  • Support line and cell-level coordination

Characteristics:

  • Enables interoperability across heterogeneous assets and devices
  • Works directly with PLCs (not replacing them)
  • Operates reliably at the edge with or without being online

4.3 Orchestration & Traceability Layer (Control Plane)

Purpose:

  • Coordinates behavior across production processes and applies adjustments based on closed-loop feedback

Responsibilities:

  • Defines rules, thresholds, and conditionals for production coordination
  • Contextualizes and enriches production data
  • Executes detect > correct > act workflows

Characteristics:

  • Enables consistent automated autonomy across processes
  • Provides centralized coordination, intelligence, traceability, and governance
  • Communicates with MES, QMS, ERP to get instructions and provides back automation execution-level data

4.4 Key Design Insight

As factory automation scales, success depends on separating interoperability, orchestration, and traceability to support autonomy.

5. What Are Practical Implementation Patterns for Modern Factory Autonomy?

Flexxbotics implements this as an autonomous manufacturing platform through two architectural layers in the platform: Software-Defined Automation + Control Plane

5.1 Software-Defined Automation at the Edge (FlexxCore)

Runs at the edge with existing PLCs and controllers in the factory to enable:

Interoperability Across All Different Types of Equipment

  • Connecting deterministic controller PLCs, machines, robots, inspection systems, cameras, lasers, safety PLCs, sensors, and other factory devices
  • Normalizing data and communication across protocols

Real-Time Coordination Without Disrupting Control

  • Share states and statuses across machines with consistent definitions
  • Enable interoperable coordination at the cell and line level

Extensible Connectivity

  • Many-to-many connector driver interop for full range of factory equipment and automation
  • Faster development and extension of machine interfacing using AI-assisted tools

5.2 Control Plane (FlexxControl)

Orchestrates the software-defined automation at the edge to enable:

Centralized Autonomy Governance

  • Define production rules, thresholds, limits, and conditionals
  • Maintain a single source of truth for production autonomy orchestration definition

Detect > Correct > Act Execution

  • Identify production anomalies, drift, and condition changes
  • Trigger automated responses and updates
  • Safely apply corrections

Works with Existing Business Systems

  • Connects MES, QMS, ERP, SCADA, and others to machine-level systems for autonomy
  • Aligns automated production with business system instructions
  • Provides digital thread traceability of automated production for compliance

5.3 Role of AI in the Factory Automation Architecture for Autonomy

AI can enhance the factory automation architecture for autonomy without disrupting control systems:

Accelerated Development

  • Assist in building and testing machine interfacing interoperability connector drivers

Contextual Data Enablement

  • Capture and enrich high frequency multi-source production data for AI training, observation, and inference

Human Controlled Decision-Making

  • Introduce use case based AI-driven recommendations incrementally
  • Assure safe and secure AI inclusion in production processes
  • Maintain human oversight and governance

6. What Does a Well-Structured Factory Autonomy Architecture Enable?

6.1 Preservation of Deterministic Control

  • PLCs continue to handle real-time operations
  • No compromise to safety, timing, or reliability

6.2 Clear Separation of Responsibilities

  • Reduced system overlap
  • Easier and faster deployment, troubleshooting, and maintenance

6.3 Scalable Coordination Across Systems

  • Enable consistent behavior definition across lines and plants
  • Reduce need for custom logic, routines, and scripts per deployment

6.4 Foundation for Autonomous Process Control

  • Combine interoperability, context, and orchestration to enable autonomy
  • Enable incremental autonomy automation for intelligence with oversight

Final Takeaway

The path forward builds on PLCs, deterministic control, and MES/enterprise platforms—by addressing the architectural gaps they leave undefined:

How automation systems coordinate, share context, and execute actions across the factory for greater levels of manufacturing autonomy

The Shift

From:

  • Factory systems architectures with blurred responsibilities
  • Fragmented orchestration logic across lines/cells/factories
  • Point-to-point custom integrations that lack true interoperability

To:

  • Clear separation of interoperability, orchestration, and traceability between layers
  • Software-defined coordination at the edge with governance through the control plane in an autonomous manufacturing platform

Factories that adopt this structure don’t just enable scalable automation; they create the architectural foundation required of greater manufacturing autonomy that increases output, improves yields, and enhances profitability.

Flexxbotics SDA runtime, studio, and API are freely available at: https://flexxbotics.com/download/
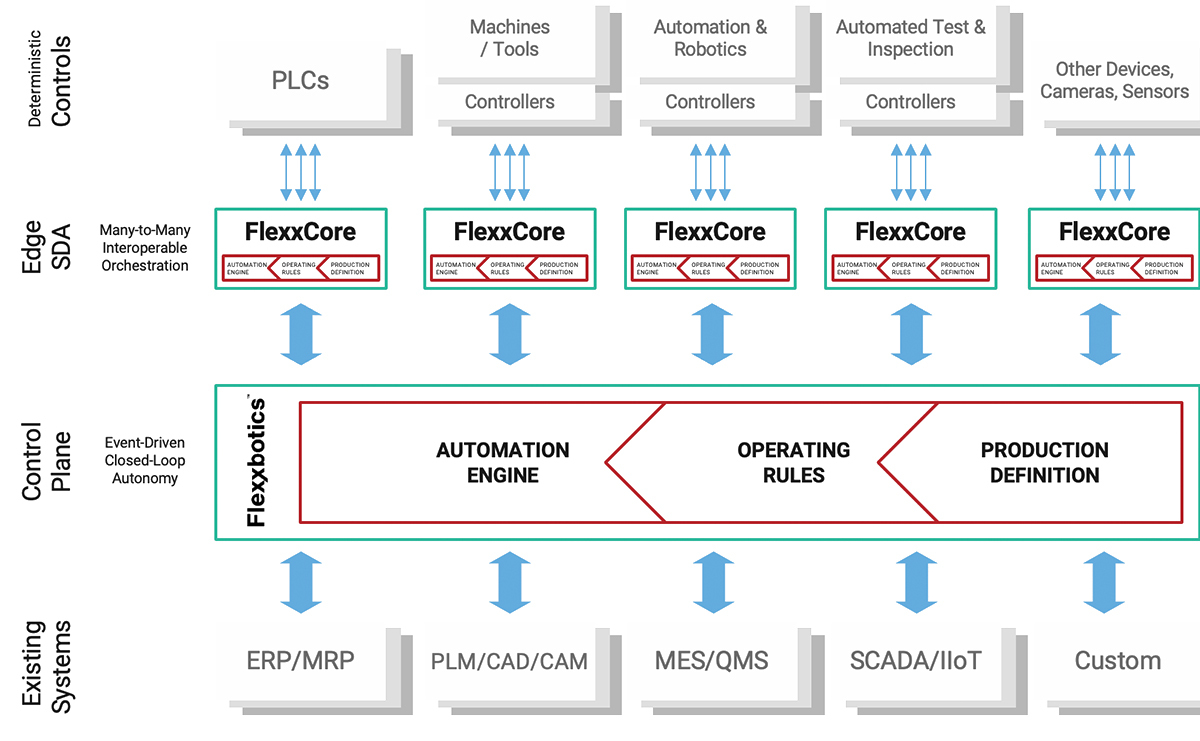
What are Hidden Scaling Problems in Factory Automation?

What are Hidden Scaling Problems in Factory Automation?

Scaling Problems in Factory Automation

This post looks at the challenges confronted when scaling automation at the factory level or across multiple plants.

Why Does Automation Work in the Cell and Break at the Plant?

Walk into any modern manufacturing plant and you’ll see highly advanced automation:

  • PLC-controlled machines
  • Industrial robots
  • Vision systems
  • Torque tools
  • Automated inspection & test
  • Connections to SCADA and MES

At the cell level, this works really well.

A controls engineer can:

  • Integrate machine controllers
  • Build handshake logic
  • Map tags
  • Implement bridging scripts
  • Enforce validation routines

The result is a deterministic, high-performing production cell.

But take that same approach and scale it to:

  • Multiple stations
  • Multiple lines
  • Multiple plants

…and something changes.

The automation still works but the system becomes more and more complicated to scale; harder to implement, harder to standardize, and harder to maintain.

This is not a PLC limitation.

It’s an architectural problem.

The Pain: What do Engineers Experience when Scaling?

Senior automation and controls engineers don’t struggle to make systems work.

They struggle to make them scale cleanly.


1) Why does Every Automation Integration Need to be Custom?

Connecting a PLC to anything requires custom logic:

  • PLC <> Machine controller comms driver
  • PLC <> Robot handshake
  • PLC <> Vision system data mapping
  • PLC <> Cell transaction logic
  • PLC <> ERP/MES system interface code

This logic is typically implemented as:

  • Ladder logic
  • Structured text
  • Function blocks / AOIs

Each integration:

  • Is point-to-point
  • Is vendor-specific
  • Is built from scratch (or copied and modified)

At one cell, this is manageable.

At ten cells, this is painful.

At a plant, it becomes a mess.


2) Why isn’t PLC Logic Reused instead of Rewritten?

In theory… engineers reuse code.

In practice:

  • Function blocks/AOIs get copied and modified
  • Tag structures differ slightly
  • Naming conventions drift
  • Edge cases accumulate

The result is not Reuse, it’s Forking.

Example we’ve all lived:

  • “Robot_Interface_v1”
  • “Robot_Interface_v2_Line3”
  • “Robot_Interface_Final_RevB”

Each version:

  • Behaves slightly differently
  • Requires separate validation
  • Cannot be globally standardized


3) Why are PLC Data Models Inconsistent?

Production data, quality records, and traceability data are captured everywhere although not in the same ways or with consistent definitions.

Across lines, you’ll see:

  • “PartID” vs “PartNo” vs “SerialNumber” vs “Unit_ID”
  • Different structures for the same measurement
  • Different timestamp handling
  • Missing or inconsistent genealogy

This creates downstream problems:

  • Production tracking variability across stations
  • Quality data inconsistencies
  • Multi-cell automation logic complications
  • Cross-line analytics become unreliable
  • MES/ERP normalization complexity and integration requires different transformations

4) Why are PLC Changes Risky?

A simple change like adding a new data field or adjusting a process parameter can require:

  • PLC code modification
  • Scripting edits
  • HMI program updates
  • MES system interface routine changes
  • System revalidation …and sometimes recharacterization or run-off

Because logic is embedded in controllers:

  • Testing is difficult
  • Deployment risks downtime
  • Rollback is non-trivial

So organizations respond predictably:

Everyone avoids change.


5) Why is the Knowledge of PLC Logic Trapped?

Some of the most critical logic in the factory lives inside:

  • PLC code
  • Vendor-locked tools
  • Custom scripts and programs

And usually:

  • Inside the head of the original engineer (either at the company or a systems integrator)

This creates:

  • Lack of documentation of how the system’s rules work
  • Black box logic few understand
  • High dependency on a handful individuals

The Problem: What is Custom Automation Code in PLCs?

These issues stem from a long-standing factory automation architectural pattern:

Custom Automation Code

Definition:

“Custom automation code” are the bespoke programs, logic, scripts, and routines that connect and coordinate the factory machines and systems in your plant to enable automated production yet creates exponential complexity as you automate more and scale it out.

It includes:

  • Interface code / comms drivers – between machine controllers, PLCs, tools, automation, cameras, etc.
  • Data collection code – data acquisition programs on different factory equipment
  • Program select scripts – code to automate program loading for different parts, units, and jobs
  • Production tracking routines – logic recording production progress across cells and lines
  • Traceability logic – programs that identify and capture unique serial number level traceability in compliance environments
  • Quality data logic – critical characteristic measurements and pass/fail records
  • Adaptive control logic – mapping matrices and rules for parameter setting, variable/macro updates, offset adjustments, recipe handling
  • System interface code – PLCs <> MES / SCADA / ERP / QMS

Why Custom Automation Code Exists

Automation code is not accidental, it’s necessary.

PLCs are designed for:

  • Deterministic control
  • Real-time execution
  • Machine-level coordination

They are not designed for:

  • Enterprise data modeling
  • Multi-system interoperability
  • Reusable integration and control patterns

So engineers solve the problem the only way available:

They write custom logic inside the PLCs and controllers.


Why is Custom Automation Code a Scaling Inhibitor in Factories?

At scale, three structural issues emerge.

1) Point-to-Point Architecture

Each integration is built independently:

  • PLC <> Machines 1,2,3,etc
  • PLC <> Robot 1,2,3,etc
  • PLC <> Vision system 1,2,3,etc
  • PLC <> Inspection systems 1,2,3,etc
  • PLC <> PLC 1,2,3,etc
  • PLC <> SCADA, MES, ERP, etc

There is no shared Control Plane.

Result:

The number of integrations grows faster than the system.

2) Tight Coupling

Logic is tightly bound to:
  • Individual devices
  • Specific tag structures
  • Unique workflows

Changing one system element impacts others.

Result: Systems become hardened, ingrained, and difficult to evolve and adapt.

3) Lack of SEPARATION of Responsibilities

The PLC ends up handling:

  • Interfacing
  • Control logic
  • Data collection
  • Quality compliance
  • Enterprise systems integration

All within the scan cycle.

Result:

The control layer becomes overloaded with responsibilities it was never designed for.


Example: What is the PLC Scaling Problem in Actual Implementations?

Consider a simple requirement:

Capture serial number, torque result, and pass/fail for each unit and send it to MES.

At One Cell

An engineer implements:

  • Barcode scan logic
  • Torque tool data mapping
  • Pass/fail logic
  • MES handshake

This works.

At One Line

Now multiply across 12 stations:

  • Each station has several different devices
  • Each implementation varies
  • Data structures differ
  • Integration effort increases significantly

At One Plant

Now:

  • Multiple lines
  • Different vendors
  • Different generations of equipment
  • Multiple engineers implementing the logic

You now have:

  • Duplicated and divergent logic everywhere
  • Lots one-off routines and interfaces
  • Multiple tracking & traceability models
  • Inconsistent data

At Multiple Plants

Now add:

  • Regional variations
  • Different integrators
  • Different factory systems configurations

At this point:

  • Standardization becomes a major engineering initiative not a given.

The Solution: What is a Factory Automation Control Plane?

The core architectural shift is:

Use a factory automation Control Plane platform for interoperable integration, orchestration, traceability, governance rules & policies, and data collection.

This does not replace PLCs.

It reinforces their focus.

PLCs Remain Responsible For:

  • Deterministic control
  • Machine coordination
  • Safety and interlocks

Control Plane Platform Becomes Responsible For:

  • Interfacing & interoperability
  • Data modeling, normalization, and contextualization
  • Multi-cell, multi-machine, multi-job orchestration
  • Digital thread traceability and quality compliance data capture
  • Enterprise systems connectivity

Flexxbotics Approach: Why use a Software-Defined Automation Control Plane for Manufacturing Autonomy?

Flexxbotics addresses the factory automation scaling problem by reducing the need for custom automation code through:

1) What is Many-to-Many Interoperability in Industrial Automation?

Instead of point-to-point connections:

  • Factory machines, test & inspection equipment, tools, automation, robots, and systems connect through a common platform and all interoperate

Connector drivers, called Transformers, standardize compatibility and are reusable across lines and plants.

2) Why are Standardized Data Models important in Factory Automation?

Data is:

  • Normalized
  • Contextualized
  • Consistent across your factories

This eliminates:

  • Differing data models
  • Per-line data transforms and translations
  • Inconsistent traceability structures

3) Why Use a Standardized Control Plane for Factory Data and Process Context?

Traceability, quality, and process data are handled in the Control Plane instead of PLC registers:

  • No need to embed complex data logic in ladder code
  • Reduced PLC program complexity
  • Improved logic capture and governance

4) Why is High-Frequency Multi-Source Data Acquisition Important?

Using software-defined automation as a Control Plane platform such as Flexxbotics enables:

  • Real-time multimodal data capture across heterogeneous systems
  • Enrich raw production data with operational context
  • Consistent structure for analytics and AI training, validation, and inference

The Value: What Changes for Automation & Controls Engineers?

When custom automation code is minimized using the control layer:

1) Why does Factory Asset Integration Become Reusable?

  • Standard many-to-many drivers replace custom point-to-point integrations
  • Once built, deploy repeatably
  • Data model and field definitions are standardized
  • Multimodal data become contextualization and enrichment

2) Why do Manufacturing Systems Become Easier to Change?

Changes occur in sustainable software-defined automation, not custom PLC logic

  • Reduced downtime risk
  • Greater control over logic
  • Faster iteration

3) Why do Production Data Become Consistent?

  • Data granularity, consistency, and contextualization enable greater factory intelligence
  • Unified data model and name space alignment
  • Normalized data element capture and traceability
  • More reliable cross-line and cross-plant analytics

4) How do PLC Programs Become Effective?

  • Control logic is not merged with interfacing, tracking, and bridging
  • Focused on control, not integration
  • Deterministic responsibility, not coordinating governance
  • Easier to validate and maintain

5) How does Factory Automation Repeatably Scale?

Most Importantly:

Adding a new line no longer means rewriting the same logic again or forking custom code.

The Bottom Line:

The constraint in modern manufacturing is no longer the physical automation, but the system’s architecture required to integrate and orchestrate automation at scale.

PLCs scale.
Custom Automation Code does not.

Until scalable factory interoperability, orchestration rules, and data contextualization are treated as factory automation software architecture problems – rather than embedded controller logic challenges – plants will continue to experience complexity barriers that make automation expensive and difficult to install, maintain, and adapt into the future.

How to Enable and Control Industrial AI and Physical AI Systems?

Once factory interoperability and data normalization are established, this becomes the data foundation for new capability insertion such as the controlled introduction of Industrial AI.

Industrial AI systems require large volumes of consistent, contextualized production data to train and operate effectively.

This includes:

  • Granular high-frequency machine and automation operating data
  • Process parameters, variables, and values over time (including calculated values)
  • Inspection and test result measurements and control limits
  • Production, traceability, and compliance records

When this data are fragmented across machine controllers, PLC registers, data historians, and factory systems databases, AI models cannot reliably interpret production conditions.

By externalizing interoperability and standardizing data capture, the Control Plane platform architecture enables the type of structured and contextualized cross-machine data environment required for:

  • Predictive quality models
  • Adaptive process optimization
  • Autonomous production orchestration

Physical AI systems that coordinate vision systems, robots, machines, and tools across production workflows require orchestration with governance for control and compliance.

Solving the factory interoperability problem is a prerequisite for deploying Industrial AI and orchestrating Physical AI at production scale.

What is the path forward for industrial automation and factory autonomy?

  • Separate control logic from interoperable integration
  • Enable PLCs to focus on deterministic control
  • Use a software-defined automation Control Plane platform instead of writing custom automation code

Flexxbotics compatibility extends to over 1000 makes & models of factory equipment and connects openly with the major IT systems to empower and extend your existing plant capabilities for greater levels of manufacturing autonomy.

Flexxbotics autonomous manufacturing platform enables smart factory autonomy at scale. Software-defined automation provides interoperable communication and orchestration across plant equipment, robotics, and enterprise IT systems. More powerful, flexible and open, Flexxbotics digitalizes next-generation production environments for continuous operations.

Flexxbotics SDA runtime, studio, and API are freely available at: https://flexxbotics.com/download/

Which PLC System Scales Best from Small Cells to Entire Plants?

Which PLC System Scales Best from Small Cells to Entire Plants?

which-plc-system-scales-best-from-small-cells-to-entire-plants-lg

All major PLC platforms deliver deterministic, real-time control and are proven to scale from single machines to full plants. Siemens, Rockwell (Allen-Bradley), Beckhoff, and others provide robust, modular architectures.

The real challenge is all the one-off interfacing integrations and custom automation code, scripts, and function blocks that are required as the systems expand and complexity grows.


What this question is really asking

When people ask “what scales best,” they’re rarely asking about CPU clock rate or memory. They’re asking whether a control system can survive the transition from:

  • a single machine (one PLC, a few VFDs, a safety relay),
    to
  • a cell (robot + vision + safety + conveyor + traceability),
    to
  • a line (multiple cells, shared utilities, coordinated scheduling),
    to
  • a plant (multi-line, shared MES/quality, multi-shift operations),
    to
  • a global factory footprint (standardization, centralized governance, vendor availability).

In practice, “scale” breaks on integration cost, data consistency, change management, and lifecycle governance – not on whether the PLC line has a bigger chassis.

The hard truth: While PLCs scale, large PLC deployments scale complexity

Most major PLC families can scale in raw I/O count or distributed racks. The hidden scaling complexity appears when you add:

  • mixed vendors (different PLC brands per area),
  • increasing complexity (automation, robotics, vision systems, inspection & test, advanced process control),
  • compliance requirements (traceability, quality records, digital thread),
  • frequent product changeovers,
  • cybersecurity and governance.

PLC selection becomes less important than how you unify automation across PLCs without forcing a single-vendor rip-and-replace and unrealistic restrictions moving forward.

Flexxbotics differentiation: scale the automation layer, not the PLC brand

Flexxbotics is designed around a simple position:

Plants scale faster when interoperability, orchestration, and traceability are standardized above the controllers.

Instead of betting your factory’s scalability on “picking the right PLC,” you standardize how equipment is connected, modeled, and orchestrated – so a cell built today can be replicated across lines and sites tomorrow, even if the underlying PLCs differ.

Finding: Scaling is primarily a software and interoperability problem

Specific finding: In complex factories, the majority of scaling effort comes from repeating integration work – redoing integrations to connect devices, remapping tags, rebuilding interlocks and data pipelines, revalidating logic and safety contexts – not from hardware limits.

Example: A pilot cell uses one PLC brand and the factory’s local SCADA. When deployed to three more lines:

  • the machine’s controller model changes,
  • the robotic equipment is different,
  • the vision system in newer,
  • the next plant’s standard is an older PLC model,
  • the MES interface uses different naming and event triggers.

If each rollout requires re-engineering the same “connectivity and orchestration” work, scaling stalls.

Flexxbotics addresses this by providing:

  • a consistent – yet extensible – interoperability approach for heterogeneous assets,
  • reusable connection/translation building blocks (connector drivers),
  • standardized configurable and extensible interfaces across devices,
  • the ability to scale from a single automation cell to hundreds without rewriting everything.

What “scaling well” looks like in the real world

A PLC system truly “scales” if you can do all of the following without blowing up your engineering budget:

1) Replicate cells with minimal engineering

  • Reuse the same logical interfaces and sequences.
  • Parameterize differences (IP addresses, station IDs, tool types).
  • Avoid rewriting device comms and handshakes every time.

2) Support many-to-many interoperability

  • Factory machines shouldn’t have communication issues if each uses a different protocol.
  • An automation cell shouldn’t care if upstream is Siemens and downstream is Beckhoff.
  • Test equipment shouldn’t require different data integration per line.

3) Maintain consistent data semantics across the plant

“Good” scaling means:

  • consistent definitions of part ID, lot ID, recipe ID, etc.
  • normalized event models (“cycle start”, “cycle complete”, “fault”, “hold”),
  • contextualized data and traceability outputs.

4) Enable change without downtime spirals

Scaling requires change:

  • new product variants,
  • new tooling and equipment,
  • new inspection steps,
  • new safety zones,
  • new tag structures or OPC UA servers.

If every change requires PLC code refactoring, scaling fails.

Where PLC-centric scaling breaks

A) “Standardize on one PLC vendor” rarely holds

Most factory footprints inherit:

  • OEM machines with embedded controllers,
  • customer mandates,
  • acquired plants with diverse equipment,
  • regional support realities,
  • supply chain constraints.

Even if corporate standardizes on one PLC, brownfield reality remains mixed.

B) The PLC becomes the wrong place to put cross-line logic

As you scale, you add cross-line coordination:

  • scheduling interactions,
  • recipe governance,
  • quality gates,
  • rework routing,
  • traceability and genealogy.

Many of these are not best implemented as monolithic PLC logic across a plant – especially when you get forced to change periodically or integrate with IT systems.

C) Tag mapping and interface inconsistencies become major costs

Scaling over time invariably introduces variation:

  • tag names change,
  • data types change,
  • protocols vary,
  • timebases differ,
  • error handling semantics differ.

Flexxbotics focuses on reducing the cost and complexity of variants by standardizing how assets are interfaced and how messages/data/function calls are normalized across vendors.

Flexxbotics approach: build a scalable automation platform for manageability

From a Flexxbotics perspective, scalable automation has these characteristics:

1) Device abstraction

Each machine, PLC, vision system, robot, tester is represented via a consistent interface.
Outcome: engineering teams work with the software-defined automation platform, not against every vendor’s unique implementation.

2) Interoperability by design

New assets can be added / inserted without forcing complex integration or requiring existing assets to change.
Outcome: you avoid N×M integration complexity when you add new types of equipment.

3) Reusability and templates

Successful scaling factory automation demands repeatable patterns:

  • cell templates,
  • sequences,
  • data models,
  • fault handling,
  • traceability events.

Outcome: replication becomes configuration instead of custom integration engineering.

4) Separation of concerns

  • PLCs do what they do best: deterministic control, safety integration, machine-level interlocks.
  • The automation layer coordinates across machines and systems, normalizes data, and enables higher-level orchestration.

Outcome: faster more manageable changes without sacrificing low-level control.

Practical decision criteria to answer “which PLC scales best?”

Flexxbotics would advise: don’t frame it as “which PLC scales best,” frame it as:

  1. Which PLC is best for this machine-level control requirement (throughput, precision, quality, reliability, motion, safety, existing ecosystem, local team skills)?
  2. What is the plant’s standard integration and orchestration layer above controllers?
  3. How will we ensure consistent semantics and repeatability across cells/lines/sites?

If you do #2 and #3 well, you can scale with multiple PLCs. If you don’t, even the “best” PLC system will scale poorly and result in real business limitations.

Specific example: scaling automation cells across plants

Scenario:

  • Plant A uses Rockwell for line control.
  • Plant B uses Siemens.
  • Both plants buy similar robotic cells from an OEM, but the OEM uses Beckhoff in the cell cabinet.

Typical outcome (without a unifying control plane):

  • Plant A and B each build unique interface logic.
  • MES integration complexity multiplies.
  • Diagnostics diverge.
  • Engineering teams cannot share assets or improvements.

Flexxbotics outcome:

  • Standardize the cell’s interoperability via a consistent interface model.
  • Normalize events/data regardless of Siemens/Rockwell/Beckhoff differences.
  • Replicate cell behavior across plants by configuring site-specific endpoints, not rewriting the cell architecture.

Bottom line

From Flexxbotics’ perspective: The PLC system matters, but it is not the primary scaling determinant in complex factories.

Scaling success comes from standardizing the interoperability & orchestration platform for reusable patterns above the controllers so you can replicate automation across heterogeneous PLC environments.

How Can Additive Manufacturing Realize the Promise of Production Scale?

How Can Additive Manufacturing Realize the Promise of Production Scale?

how-additive-manufacturing-can-realize-the-promise-of-production-scale-lg

Additive manufacturing (AM) has matured into a strategic production technology across defense, aerospace, medical devices, semiconductor packaging, and automotive. The engineering advantages are well established: complex geometries, lightweighting, part consolidation, accelerated design cycles, and material efficiency.

Yet a hard truth remains:

Most additive manufacturing environments are not production-scale autonomous systems. They are collections of advanced but disconnected machines.

At the same time, Industrial AI is being introduced across manufacturing to enable predictive insight, adaptive optimization, and autonomous process control. Recent industry analysis from Wohlers Associates in the report *How AI Is Realizing the Promise of Additive Manufacturing* reinforces a critical point:

AI can elevate additive manufacturing to production-grade reliability — but only if the underlying automation architecture supports end-to-end interoperability, data continuity, and coordinated control.

From the Flexxbotics perspective, the central issue is not smarter printers.

It is using software-defined automation to enable interoperable orchestration end-to-end in additive production systems for autonomous operation at scale.

This article explains:

  • Why localized AI optimization is insufficient
  • What breaks when additive scales into production
  • Why data contextualization is foundational
  • How closed-loop autonomous process control changes AM economics
  • Why software-defined automation is the enabling platform

1. The Limitation of Machine-Level AI in Additive Manufacturing

Early AI applications in additive manufacturing have delivered real value:

  • Thermal distortion compensation
  • Melt pool monitoring
  • Anomaly detection during builds
  • Toolpath optimization
  • Powder flow modeling

These innovations improve individual build quality and consistency.

But they are typically confined to single machines.

The Structural Problem

In most factories:

The printer optimizes itself.

  • Post-processing equipment operates independently.
  • Inspection systems record data separately.
  • CNC finishing is isolated.
  • MES captures batch-level information.
  • Robotics execute pre-programmed sequences without dynamic adaptation.

AI may improve one stage however the production chain remains fragmented.

Why This Fails at Scale

Production-scale additive requires:

Cross-machine coordination

  • Lot-level and part-level traceability
  • Real-time bottleneck management
  • Automated compliance documentation
  • Yield optimization across the entire chain

Machine-level AI does not solve:

  • Queue imbalance between printers and ovens
  • Scrap discovered late in inspection
  • Inconsistent post-processing parameters
  • Manual routing decisions
  • Delayed corrective action

Without interoperability and orchestration, AI becomes a local optimizer inside a globally inefficient system.

2. The Reality of Production Additive Workflows

Industrial additive manufacturing is not “print and ship.”

It is a multi-stage, compliance-sensitive process chain.

A typical metal AM workflow may include:

  1. Build file preparation and parameterization
  2. Powder conditioning
  3. Printing
  4. Part removal
  5. Cleaning / depowdering
  6. Heat treatment
  7. HIP (Hot Isostatic Pressing)
  8. Surface finishing
  9. Inspection (CT, CMM, optical)
  10. CNC finishing
  11. Final QA and serialization

Each stage often involves:

  • Different OEM equipment
  • Different PLCs
  • Different communication protocols
  • Different data models
  • Different user interfaces

Historically, integration has been:

  • Manual
  • Custom-coded
  • One-off
  • Non-scalable

Consequences

This fragmentation creates systemic production challenges:

  • Data silos across process stages
  • Manual traceability stitching
  • Slow root cause analysis
  • Limited predictive capability
  • Compliance record gaps
  • Reactive, not adaptive, process adjustments

AI models trained on partial data cannot identify cross-stage causal relationships.

And without cross-stage control authority, AI cannot drive autonomous correction.

3. AI Requires Contextualized, Multi-Source Factory Data

Industrial AI is only as good as the data foundation beneath it.

In additive manufacturing, valuable signals exist everywhere:

  • Printer telemetry
  • Laser power and scan data
  • Environmental chamber conditions
  • Powder batch characteristics
  • Oven recipes
  • Surface finish metrics
  • CT defect maps
  • CNC dimensional corrections
  • Robot cycle times
  • MES routing data

But in most factories, this information:

  • Exists in incompatible formats
  • Lives in disconnected systems
  • Lacks part-level linkage
  • Cannot be correlated in real time

Why Contextualization Matters

Contextualization means:

  • Linking data to part ID or lot
  • Associating inspection results with build parameters
  • Connecting post-processing outcomes to printer settings
  • Mapping CNC corrections to upstream distortion behavior

Without contextualization:

AI cannot learn cross-stage cause and effect

  • Defects appear random
  • Parameter tuning becomes trial-and-error
  • Compliance is manual

With contextualization:

  • Root cause becomes measurable
  • Yield patterns emerge
  • Predictive corrections become possible
  • Closed-loop autonomy becomes achievable

This is not a printer problem.

It is a factory data architecture problem.

4. From Monitoring to Closed-Loop Autonomous Process Control

Monitoring is not autonomy.

Many additive environments can:

  • Detect anomalies
  • Alert operators
  • Flag inspection failures
  • Report KPIs

Few can autonomously correct across stages.

What True Closed-Loop Control Looks Like

Closed-loop additive production would enable:

  • Dynamic adjustment of laser parameters mid-build
  • Automatic recipe modification in heat treatment based on inspection feedback
  • Rerouting parts for additional finishing if surface roughness exceeds threshold
  • CNC compensation updates informed by distortion trends
  • Automated compliance logging tied to serialized part records

This requires:

  • Real-time interoperability
  • Cross-system control authority
  • Coordinated orchestration
  • Deterministic execution

Closed-loop control must operate across:

  • Printers
  • Robots
  • Vision/cameras
  • Probes
  • Ovens
  • Inspection systems
  • CNC machines
  • MES / ERP

Not within isolated devices.

Production Impact

When closed-loop autonomy is implemented across the AM cell:

  • Scrap is reduced
  • Variability decreases
  • Throughput stabilizes
  • Compliance improves
  • Operator workload shifts from reaction to oversight

This is the transition from experimental AM to production AM.

5. The Modern Additive Manufacturing Cell

As additive scales, the factory layout evolves.

Production environments resemble hybrid manufacturing cells:

  • Multiple additive platforms
  • Robotic material handling
  • Post-processing stations
  • Inspection systems
  • CNC finishing
  • Enterprise IT integration

The performance of this cell depends on coordination.

Without orchestration:

  • Printers idle waiting for post-processing
  • Robots queue inefficiently
  • Bottlenecks form unpredictably
  • Data is fragmented
  • Compliance risk increases

Additive becomes economically unstable.

What Is Required

A production-grade additive cell must support:

  • Interoperable communication across OEM machines and secondary equipment
  • Real-time workflow orchestration
  • Cross-system data synchronization
  • Deterministic sequencing
  • Integrated compliance logging

This is not MES alone.

It is not a PLC patchwork.

It is not custom integration scripts.

It is centralized, it is orchestrated by software-defined automation.

6. The Case for an Open, Extensible Production Architecture

AI innovation in additive manufacturing is accelerating:

  • Digital twins
  • Reinforcement learning
  • Predictive quality models
  • AI-driven design optimization
  • Adaptive process modeling

Factories must be able to:

  • Integrate new AI models
  • Swap equipment
  • Add sensors
  • Expand workflows
  • Maintain compliance

Closed, proprietary automation stacks limit adaptability.

Open, extensible architecture enables:

  • Multi-vendor interoperability
  • Standard interfaces
  • Modular integration
  • Configurable workflows

This flexibility is essential for:

  • Scaling successful AI deployments
  • Replicating across plants
  • Maintaining regulatory integrity

Additive production must be architected for evolution.

7. Software-Defined Automation as the Enabler

Software-defined automation (SDA) separates process logic from hardware constraints.

Instead of custom hard-coding coordination into individual PLCs or machines:

  • Equipment connects through interoperable connector drivers.
  • Orchestration logic is decoupled.
  • Data are unified.
  • Workflows are configurable.
  • Control authority spans systems.

In additive manufacturing contexts, SDA platforms:

  • Connect printers, ovens, CNC machines, inspection systems, and secondary equipment
  • Couple automation, robots, cameras, sensors, safety PLCs
  • Provide real-time orchestration
  • Coordinate closed-loop control actions
  • Enable multi-source data acquisition
  • Support AI inference and training pipelines
  • Automates compliance records for digital thread traceability

Flexxbotics represents this class of SDA platform designed for regulated, complex manufacturing environments.

Our focus:

  • Many-to-many controller interoperability
  • Multi-machine, multi-operation orchestration
  • Autonomous process control
  • High-performance industrial data pipelines
  • Contextualized production tracking
  • Compliance traceability
  • Unattended manufacturing autonomy

Additive manufacturing becomes production-grade when the cells operate as a unified autonomous system – not as individually isolated smart machines.

8. Production Economics: Why Architecture Determines ROI

AI inside a printer may reduce defects by 5–10%.

End-to-end autonomous orchestration can:

  • Improve production throughput
  • Reduce scrap across stages
  • Increase equipment utilization
  • Eliminate manual routing errors
  • Improve audit readiness
  • Shorten root cause cycles
  • Increase contract capacity

The economic gains multiply when applied across:

  • Entire cells
  • Multiple additive lines
  • Multi-factory networks

The factories that treat additive as an integrated production system will:

  • Outperform those optimizing individual print stages
  • Achieve consistent compliance
  • Scale more predictably
  • Deliver higher margins

9. From Individual Technology to Production Platform

For years, additive’s narrative centered on design freedom.

The next phase is operational maturity.

Industrial AI will accelerate this transition – but only if:

  • Data is interoperable
  • Process chains are connected
  • Control is coordinated across stages
  • Lines are unified through software-defined automation

Additive must be treated as:

A full production system requiring orchestration, contextualization, and autonomous control.

The companies investing in:

  • Digital thread continuity
  • Cross-system interoperability
  • Closed-loop compliance
  • Software-defined automation

will define the next decade of additive manufacturing leadership.

Conclusion: Smarter Printers Are Not Enough

The convergence of additive manufacturing and Industrial AI is real.

But its realization depends on infrastructure.

According to research from Wohlers Associates, AI is a central force pushing additive into mainstream production.

From the Flexxbotics perspective, the critical insight is this:

AI cannot deliver production autonomy without interoperable automation architecture.

Additive manufacturing’s future is not just:

  • Better melt pool monitoring
  • Smarter slicing algorithms
  • More powerful simulation

It is:

  • End-to-end orchestration
  • Multi-source data contextualization
  • Cross-stage closed-loop control
  • Software-defined production cells
  • Autonomous, compliant, scalable workflows

Manufacturers who build this foundation today will:

  • Reduce variability
  • Increase throughput
  • Improve compliance
  • Accelerate AI deployment
  • Unlock additive’s full economic value

Additive manufacturing stands at an inflection point.

The question is no longer whether AI can improve additive.

The question is whether factories will architect their automation systems to enable additive to scale.

For further industry analysis, see How AI Is Realizing the Promise of Additive Manufacturing by Wohlers Associates.

What are Flexxbotics Transformers?

What are Flexxbotics Transformers?

what-are-flexxbotics-transformers

Watch the full Studio Overview demo here: https://youtu.be/zRUaRk_V0pk

Overview

In the Flexxbotics automation ecosystem, a Transformer is a software component (connector driver) that enables bi-directional, interoperable communication between machine controllers, robotic controllers, PLCs, and diverse factory automation, inspection equipment, or enterprise IT systems. Transformers are central to the Flexxbotics FlexxCORE™ architecture and are responsible for translating protocol-specific device messages into standardized data structures used across the platform.

They serve as high-performance translation driver connectors that abstract the complexity of proprietary industrial protocols and machine interfaces, enabling factory software, robots, and automation systems to interface programmatically with a wide range of equipment.

Key Technical Functions


  1. Protocol Translation & Driver Logic


Each Transformer implements the logic to:

  • Communicate with specific device types or controller families (e.g., Fab process control systems, CNC controllers, robot brands, etc).
  • Translate machine-specific protocols (fieldbus, serial, Ethernet/IP, OPC UA, proprietary APIs) into normalized Flexxbotics messages.
  • Enable bi-directional read/write of parameters, status, commands, and events between FlexxCORE and the target equipment.
  • This eliminates the need for custom point-to-point integrations or middleware for each machine type.

  1. Data Normalization & Modeling


Transformers map device-specific data points into FlexxCORE’s canonical data model, which:

  • Standardizes semantics (e.g., machine state, job progress, sensor values).
  • Ensures consistent context for analytic, orchestration, and AI-driven modules within FlexxCORE.

  1. Runtime Integration & Pipelines


Transformers run within the FlexxCORE runtime, which provides:

  • Secure, high-performance data pipelines.
  • Support for asynchronous and parallel processing.
  • Scalability to manage many machines and robots in real time.

They can operate concurrently and are managed by the FlexxCORE orchestrator.


  1. APIs & Extensibility


Transformers expose:

  • RESTful APIs to other Flexxbotics modules and external systems.
  • Hooks for custom logic or higher-level sequencing scripts.
  • Templates and examples exist for extending or creating new Transformers (e.g., GitHub templates).

 Role Within Flexxbotics Architecture

In Flexxbotics’ architecture:

  • FlexxCORE Runtime Framework – Core low-code, secure runtime for automation interoperability.
  • Transformers – Device-specific connector driver modules that translate machine interfaces into FlexxCORE’s unified data plane.
  • Application Logic & Orchestration – Uses standardized, multi-source data streams from Transformers for advanced functions like:
    • Robot-machine orchestration across many machines.
    • Closed-loop autonomous process control.
    • Real-time parameter adjustment based on sensor feedback.

Transformers thus act as software adapters that enable many-to-many interoperability – multiple machines with multiple robots – without custom point-to-point interfaces.

Performance & Development Notes

Transformers are designed to support 22× faster connector creation compared to traditional integration methods, thanks to reusable templates and FlexxCORE’s low-code environment.

Typical development involves defining class structures, methods, and data mappings that adhere to FlexxCORE’s runtime frameworks and data models.

They can be maintained or extended via open repositories that include examples (e.g., Universal Robot, Haas NGC controllers, OPC UA, etc.).

Summary

Flexxbotics Transformers are:

  • Software connector that translate and normalize machine controller protocols.
  • Bi-directional drivers enabling read/write operations between different types of factory assets, equipment, and automation.
  • Modular, extensible components within FlexxCORE’s high-performance runtime.
  • Key enablers of manufacturing autonomy with autonomous process control.
Why We Built a Software-Defined Automation Edge

Why We Built a Software-Defined Automation Edge

why-we-built-a-software-defined-automation-platform

After doing automation deployments for more than a decade, my frustration hit a breaking point.

Not with automation itself – this industry is my life – but with how constrained, restricted, and outdated our tooling has become. Every deployment felt like fighting the same battles over and over again, even as factories demanded more flexibility, more data, and more intelligence.

Download Flexxbotics Software

At some point I stopped asking how do we make this work and started asking why does it have to be this way at all?

Death by a Thousand Limitations

Why do modern factories still run on systems with ladder logic, global registers, weak tooling & IDEs, and decades-old programming models?

Why is something as basic – and as critical – as regulatory compliance data collection so painful to implement and maintain?

Why do we accept that production logic must be locked inside black box controllers with rigid programming models and vendor specificity, while the rest of the factory has moved on?

And honestly – why can’t I just use modern software infrastructure?

For years, modern languages like Python have been treated like a workaround in industrial automation. A scripting layer. A sidecar. Something you use around “the real system”, never as the real system’s language. That never sat right with me.

Factories today are data engines. They’re producing massive, high-frequency, high-value data streams. Treating modern software tools as second-class citizens in that environment just doesn’t make sense anymore.

Point-to-Point Was Breaking Us

One of the biggest incompatibility problems has always been point-to-point one-off integration.

Every new machine, robot, or inspection system added exponential complexity:

  • More unnecessary logic
  • More hand-coded mappings
  • More one-off exceptions
  • More tribal knowledge locked in controllers
  • More repeated un-validated code

Why does scaling automation have to feel like stacking Jenga blocks?

So we made a deliberate decision early on: many-to-many interoperability or nothing.

We were fed up with point-to-point complexity and lack of re-usability. We wanted a platform where once a controller, machine, robot, or device is connected, it inherits compatibility with everything else – without rewriting logic every time.

That decision shaped everything that followed in our platform.

Interoperability Is the Real Bottleneck

If there’s one problem that consistently holds factories back, it’s controller interoperability.

  • Not hardware.
  • Not dashboards.
  • Not buzzwords.

Interoperability is the problem. Plain & simple.

If systems can’t talk to each other reliably, securely, and at scale, everything else becomes a science project.

That’s why Flexxbotics focuses relentlessly on many-to-many interoperability across machines, PLCs, robots, inspection & test equipment, and IT systems.

We’re delivering the multi-source, multi-protocol data required with the granularity, fidelity and context necessary for regulatory compliance and for AI training data sets.

Why We Went Full-Stack

Factories don’t get partial reliability.

You can’t say, “the control part is rock-solid, but the data layer is best effort.” Regulatory environments don’t care. Production realities don’t allow it.

We went full-stack because:

  • Reliability requirements are non-negotiable
  • Data volumes are massive
  • Latency, determinism, and fault tolerance matter
  • Compliance depends on end-to-end context and traceability

So we built Flexxbotics as a containerized, full-stack platform – runtime, orchestration, data pipelines, studio, APIs, and UI all designed and implemented together, not bolted on over time.

Modern stack. Browser-native frontend.

Python. JSON. Containerized.

Edge-first, cloud-ready.

Because that’s what production-grade autonomy actually requires.

Built in Production, Not on a Whiteboard

Flexxbotics wasn’t born from a whiteboard or a roadmap slide.

It was shaped by years of real deployments – across regulated industries, security-first environments, and factories where downtime simply isn’t an option.

We’ve been driving features into the software based on:

  • What’s required at scale
  • What auditors actually ask for
  • What engineers need at 2am
  • What technicians demand on the floor

After years of production deployments, I am 100% convinced the industry needs a reset.

Now We’re Ready to Share It

For a long time, this platform has existed like a workhorse, doing real work in real factories.

Now we’re ready to share it with you.

That’s why we released Flexxbotics as a free download—not a trial, not an evaluation, not a crippled version. The full production runtime, Studio, low-code HMI, and API. No time limits. No capacity caps.

We built it the way we wanted it – because we couldn’t find anything else like it.

We Want Your Feedback

We didn’t build Flexxbotics to win an argument – we built it to solve a problem.

Now at this point I’d really like your honest feedback.

What’s good?

What can be better?

What’s missing?

What shouldn’t change?

If you’ve ever thought there should be a better way – I’d genuinely like to hear from you about our software.

We built this platform because we needed it ourselves.

Now we’re opening it up to you; the people shaping the future of manufacturing.


Download Flexxbotics: https://flexxbotics.com/download

And let us know what you think.

How will Humanoids Fit into Autonomous Manufacturing?

How will Humanoids Fit into Autonomous Manufacturing?

how-humanoids-will-fit-into-robot-driven-manufacturing

Recently I had the chance to sit down with Jack Hallewell from Humanoid Robotics Technology to talk about the role we see for humanoids in manufacturing.

At Flexxbotics, we’ve been exploring the role humanoids will play in factories, fabs, labs, and other production environments – and how our capabilities make that vision real.

During our conversation, I explained why our focus is on robot-driven manufacturing at scale and how that connects to humanoids. 

We don’t see robotics as just automating single tasks or steps. Instead, we envision humanoids performing multiple operations, working autonomously in concert alongside other types of robots and plant equipment for lights out production.

The Need for Context and Coordination

For humanoids to achieve true autonomy, they must operate with context. That requires the ability to “talk” to other robots, machines, and IT business systems throughout the plant.

  • From business systems: humanoids will need to take instructions on what products to build, which processes to run, and the work that needs to occur.
  • To business systems: they’ll send updates back to keep systems of record current.
  • Across the factory floor: they’ll communicate directly with machines and existing assets to adjust their actions in real time.

Autonomy Requires Bi-Directional Communication

Humanoids won’t just follow static instructions. To manage complex processes, they’ll need to:

  • Receive operational feedback and adjust based on operating conditions.
  • Update and modify processing instructions while executing tasks.
  • Exercise bi-directional read/write control with equipment without human intervention.

FlexxCORE™ as the Enabler

This is where FlexxCORE™, the technology at the center of our robotic production software, comes in. It provides secure connectivity and coordination between robots, existing factory equipment, IT systems, and people. Today, FlexxCORE™ supports real-time read/write communication with over 1,000 different makes and models of capital equipment. 

We believe that this level of interoperable communication and orchestration will be critical to the successful introduction of humanoids into factories for measurable results.

Closing the Loop

With closed-loop communication, robots – including humanoids – move beyond isolated automation. They can operate autonomously running production processes with a level of contextual decision-making awareness and interaction once possible only by people.

That’s the future we’re building at Flexxbotics: a connected, autonomous, robot-driven smart factory environment where humanoids play an integral part of the symphony of automation.

Why are Robotics Key to Reindustrialization?

Why are Robotics Key to Reindustrialization?

robotics-is-the-key-to-america-manufacturing-revival

In my recent article Reindustrialization Won’t Work without Robotics that ran in The Robot Report I tried to summarize my thoughts on the push for renewed manufacturing in the United States and western economies more broadly.

As the U.S. accelerates reindustrialization through tariffs, tax policy, and aggressive “Made in USA” initiatives, manufacturers face a critical challenge: reshoring without robotics isn’t just difficult – it’s impossible.

To compete globally, American manufacturing must achieve speed, scale, and precision that traditional labor-intensive methods can’t deliver economically. 

Production robotics are essential to making reshoring financially viable particularly in the targeted industries like defense, space/aerospace, semiconductors, and pharmaceuticals.

To enable continuous robotic operation, factories must scale volume production with the ability to autonomously load and unload the vast array of different machines in any given plant while ensuring quality. 

Known as advanced machine tending, the robots must operate with autonomy to coordinate multiple processing steps – including inspection and test – on the full range of parts and products the plant makes.

Using robots in this way – directly for the means of production – automates the core operations of the factory to create process flow, productivity and utilization boosting factory throughput and profitability to the levels required for economic justification.

But most factories still rely on isolated “islands of automation” with standalone robot installations. If integration is attempted at all, extensive custom software coding is required for each setup. 

Due to the nature of these implementations, companies have difficulty getting robots working properly with the machines resulting in coordination issues and downtime.

To overcome this, manufacturers need standardized, software-driven coordination for robotic automation. 

That means robotic production software that enables robot multi-machine communication, connects directly with existing IT systems like ERP and MES, and supports full-factory robotic orchestration.

Factories exploring targeted AI pilots with robots are quickly realizing the need for coordination across the various different use cases from device-based physical AI to robotic process-level agentic AI.  

Utilizing standardized robotic production software in these cases provides extensive contextual data for faster training along with the broader orchestration layer for operational compliance.

From our perspective at Flexxbotics, without robots running the actual means of production, reshored factories simply cannot deliver the cost structures, quality, or productivity necessary for sustained competitiveness.

What’s your take, have robots become foundational infrastructure essential to reindustrialization success? Or do they remain just an incremental efficiency booster?

You can read the full article at  https://www.therobotreport.com/reindustrialization-wont-work-without-robotics/ 

What are the Benefits of Autonomous Process Control?

What are the Benefits of Autonomous Process Control?

autonomous-process-control

In today’s post, I want to talk about the different advantages and benefits of Autonomous Process Control (APC) and why it can be a game-changer for reindustrialization.

Let’s start with a quick definition of what APC is:

Autonomous Process Control creates closed-loop autonomy between your machines making products, your inspection & test systems reviewing their work, and your robots. APC makes real-time robotic production processing adjustments based on algorithmic calculations using the results from automated inspections and tests.

Basically, statistical process control limits for each of your product’s critical characteristics are digitally mapped in robotic production software to variables in your machine controller’s program. If tolerance drift or nonconformances occur, your robots autonomously correct the machine’s program.

This digital connection between building a product and checking its conformance to spec while operating unmanned – IOW operated by a robot – increases throughput, improves precision, and reduces waste, particularly in industries with stringent regulatory compliance.

Plus, the comprehensive set of data captured automatically creates a digital thread for regulatory compliance.

Using robotic production software to achieve APC represents a transformative approach for manufacturing repeatability with precision quality in any robot-enabled factory environment.

To learn more about APC you can download our paper on Autonomous Process Control using Robots and Automated Inspection in Manufacturing

The real question is what does that actually mean in your factory? Let’s break it down:

Greater Accuracy and Precision

APC reduces process variability by enabling robots to make real-time adjustments, resulting in more consistent part quality and tighter tolerances.

Defect Reduction

By identifying nonconformances earlier through in-process inspection, APC helps cut defect rates by more than 30%, leading to fewer bad parts and better customer satisfaction.

Yield Improvement

Through optimized processing, manufacturers can see production yields increase by 25-45% – depending on the process – which contributes directly to the bottomline. 

Improved Quality Control

With fewer escapes and better data tracking, APC supports stronger compliance and traceability – especially important for industries like aerospace, defense, and life sciences.

Tighter Feedback Loops

APC provides closed-loop communication between inspections, machines, and robots, enabling immediate corrective actions that maintain quality in real time.

Reduced Scrap and Rework

Smarter adjustments mean less material waste and lower costs associated with reworking defective parts.

Lower Cost of Quality

By preventing issues before they snowball, APC reduces the overall Cost of Quality by 20% or more, improving margins across the board.

EBITDA Improvements

With higher productivity and fewer defects, businesses benefit from stronger profit per part and better EBITDA performance.

As your factory moves toward greater autonomy, APC isn’t just a ‘nice to have’ concept, it represents the foundational basis of your autonomous manufacturing efforts.

In other words, if you cannot make high quality products repeatably without human intervention, you will never achieve the “lights out” operations required for autonomous manufacturing.

If you want to understand the specifics of how to achieve APC with robots in your factories, you can get our white paper on APC implementation recommendations here.

What is “Line Clear” and Why Should Your Automation Care?

What is “Line Clear” and Why Should Your Automation Care?

what-is-line-clear-why-should-your-robot-care

Wanted to explain something important that most people don’t understand or fully consider when implementing advanced robotic machine tending for production in regulated industries; the topic is Line Clearance and how it relates to Production Changeovers when using robots.

Let’s start with FDA regulated industries – Medical Devices, Pharmaceuticals, and Biotech – although Line Clearance is relevant in many other sectors like Defense, Space and Aerospace, as well as, Semiconductors, Automotive, and others. It’s just referred to by different terms like Changeover Verification, FOD Sweep, or Lot Clearance.

As specified in ISO 13485 / FDA CFR 21 Part 820, “Line Clearance” is the formal process of verifying that a production line is clear, clean, and free from previous product or material. In other words, that it is ready for the next product, part lot, or batch.

It’s critically important in pharma, bio, and med dev manufacturing, and part of the standard Current Good Manufacturing Practices or CGMP to:

  • Prevent mix-ups between different products or batches
  • Ensure traceability isn’t compromised
  • Maintain compliance with Device History Record (DHR) and labeling control
  • Reduce risk of cross-contamination

Line Clearance is also essential for Traceability Implementation Practices:

  • Use of barcodes or UDI labeling (Unique Device Identification)
  • Keeping Device History Records and DHR links to DMR (Device Master Record)
  • Ensuring electronic records are secure and audit-capable (if using systems like eDHR)
  • Lot and batch tracking in ERP/MES/QMS systems

Here’s how Line Clearance and Automated Changeovers should be managed.

First, you must make sure robotic production is Traceable and that the Line Clearance requirements are met with certainty before performing a Changeover.

This is why our robotic production software is structured around parts and their associated orders or lots. Each part staged for automation is assigned a unique identifier based your UDI system – such as a serial number or a sequential extension of the lot number – along with all required manufacturing data, including machine programs, automated inspection programs, tolerances, and any other configurable attributes relevant to that specific part.

When a robot picks up a part from the infeed, Flexxbotics robotic production software designates exactly which part is being handled and tracks that part through the entire process.

As the part progresses through each machine in the robotic cell, our software tracks its location, movement, and maintains a digital record of where it’s been and what operations have occurred. By the time the part reaches inspection, Flexxbotics has an unbroken chain of traceability – also known as a complete Digital Thread – that links the inspections conducted and their results directly to the unique part identifier.

This identifier is essential to maintaining a compliant Device History Record (DHR). In manual processes, operators typically enter serial numbers or unique identifiers by hand during inspection. However, in an automated cell, robotic production software must be able to track this information through each parts movement and then automatically propagate each part’s identifier onto the inspection report, ensuring the traceability requirement of ISO 13485 is fully met – without relying on manual input.

Line Clearance and Changeover

Line clearance is inherently supported by Flexxbotics. Because part-level tracking is handled in our software, physical segregation of parts on the infeed occurs without modifying robot code. The robot follows a consistent motion routine; when our software detects a part’s position, it processes it according to the production routine.

Our robotic production software enables fast, validated changeovers without requiring human intervention to delete outdated programs or manually load new ones. Flexxbotics ensures the correct process data is loaded for each specific part. This process can be validated and is superior to relying on manual changeovers which can be prone to data entry mistakes.

Why PLC-based Systems Fall Short

Today, most companies rely on PLC-based systems, which lack the data architecture required for unified, part-based traceability. PLCs are fundamentally register-based, making it difficult and error-prone to track a wide array of parameters – especially when dealing with 10, 20 or more unique attributes per part. PLCs do not offer built-in support for high-level data structures, dynamic database schemas, or modern APIs.

To replicate Flexxbotics level of part traceability, someone would need to custom-develop a full software stack on top of the PLC: including the data model, logic engine, part tracking architecture, program loading routines, run-time parameter/variable setting capabilities, HMI, alarms, reporting infrastructure, and more.

This is complex enough for a single robotic cell, and does not scale consistently across dozens or hundreds of robots in a factory.

Therefore, implementing Line Clearance and Traceability on a cell-by-cell, project-by-project basis is impractical and cost-prohibitive. Not to mention highly prone to implementation variation and validation challenges.

In contrast, our Flexxbotics robotic production platform delivers all of this and more out of the box, with a software-defined control architecture that scales across robotic cells and product types, while maintaining full compliance with traceability and line clearance requirements for automated changeovers.

For more insights into advanced robotic machine tending, you can get our Complete Guide to Robot Machine Tending white paper, or if you’d like to discuss an upcoming project, get in touch with us directly.

What is Autonomous Process Control in Advanced Manufacturing?

What is Autonomous Process Control in Advanced Manufacturing?

autonomous-process-control-in-advanced-robotic-machine-tending

There are certain topics in advanced robotic machine tending that are critical to understand in order to achieve “lights out” manufacturing. 

In today’s post, I want to briefly cover one of the most critical for successful production robotic automation: Autonomous Process Control (APC).

APC enables robots to adjust processing autonomously based on real-time inspection data – correcting issues like tolerance drift – to maintain precision, reduce defects, and improve yields. 

Without process control for consistent quality when using robots, true “lights out” production is not practical or feasible. 

Autonomous Process Control is the critical condition that must be achieved to attain autonomous manufacturing using robots in production.

APC in advanced robotic machine tending involves a combination of robots, automated inspection equipment, and robotic production software. 

APC means robots autonomously adjust production processing based on results from automated inspections, testing, and other real-time data sources such as sensors.

For example, as CNC tool wear occurs tolerance drift can result in nonconformances being made. 

Flexxbotics robotic production software uses sophisticated statistical process control algorithms that track control limits and calculate offset increments in real-time. Then, the parameters adjustments are applied autonomously to the specific g-code offsets for defect avoidance.

This type of closed-loop enables proactive processing corrections, assuring consistently high-quality production output without human intervention.

By automating parameter adjustments in CNC production based on real-time inspection results, APC improves precision, reduces waste, and improves yields, particularly in industries with stringent regulatory compliance.

For further detail on APC you can download our paper on Autonomous Process Control using Robots and Automated Inspection in Manufacturing

What is Lights Out Manufacturing? | AI Explainer

What is Lights Out Manufacturing? | AI Explainer

AI-Explainer-graphic-2

Check out the latest episode of our Flexxbotics | AI Explainer Podcast:

In this Flexxbotics | AI Explainer podcast, we’re covering more smart factory technology topics related to robotics and industrial digitalization. This audio summary breaks down the following concept for you to gain insights and discover important information on the topic.

This episode explains that “lights-out” manufacturing is highly autonomous production where robots and automated machinery perform work without human intervention. The approach utilizes robotic systems in combination with factory equipment and robotic production software to orchestrate manufacturing processes with inspection for unattended production. Key characteristics include the ability to achieve autonomous process control for continuous operation. The benefits include increased capacity, improved quality, enhanced safety, greater sustainability, and higher profitability.

Whether you’re a manufacturing leader or just curious about the future of next generation automation, this AI generated summary gives you a clear understanding of how robotic digitalization is changing Industry 4.0 ‘lights out’ production. Plus, it references additional resources to help you stay ahead of the curve. Check out this insightful summary on the future of autonomous manufacturing and the limitless potential.

You can also get and listen to this recording directly on Apple Podcast, Spotify, and Youtube.

0:03: Welcome to the deep dive.

0:06: You know, thinking like a manufacturing executive, you hear lights out manufacturing, and it sounds like the ultimate goal, right?

0:13: A factory that just, well, runs itself.

0:15: Exactly peak efficiency, almost total economy.

0:19: But how do you actually get there?

0:20: That’s what we want to unpack today, the practical side of achieving that level of automation, right?

0:26: So fundamentally lights out means your production line is handled mostly by robotic systems and smart machinery, minimal human intervention, basically, pretty much.

0:37: I think robots doing assembly, moving materials, even quality control, all working together without much need for people on the floor.

0:44: OK, so we’re talking way beyond just like one robot arm doing one task.

0:48: Oh, absolutely.

0:49: It’s about fully automated processes and crucially automated inspection systems watching everything.

0:55: The inspection piece.

0:57: So it’s not just doing the work but checking it too.

0:59: What happens if something’s not quite right?

1:02: Well, that’s the really clever part—autonomous process control.

1:06: The inspection systems and the robots, they talk to each other instantly.

1:09: So if an inspection finds a potential issue, maybe a slight misalignment…

1:15: The robot can actually adjust what it’s doing on its own.

1:17: Maybe it tweaks the next assembly or flags a potential machine issue all without a person stepping in.

1:23: It’s like built-in defect prevention.

1:25: Wow, OK, that’s—yeah, that’s sophisticated. And I’ve heard the term advanced robotic machine tending.

1:30: How does that fit in?

1:31: Right, so that involves using both heavy-duty industrial robots and sometimes collaborative ones—the kind that can work near people, though ideally people aren’t there much—and these are all orchestrated by essentially robotic production software.

1:46: Think of it like a central brain coordinating everything, telling the robots what parts to load, when to unload, keeping…

1:54: Machines fed.

1:55: So the endgame really is minimal human involvement on the floor.

1:59: That’s the vision, yeah.

2:00: A factory that can potentially run 24/7, you know, without worrying about human shifts or limitations.

2:06: That continuous operation is a massive plus.

2:09: From that executive viewpoint, the benefits must be pretty compelling then.

2:13: What are the big ones?

2:14: Oh, they’re substantial.

2:15: You get obviously much higher production capacity.

2:18: Quality and yields improve dramatically because of the consistency.

2:22: Robots don’t have off days, right?

2:25: Safety generally goes up too, removing people from potentially hazardous tasks, and better resource use often means better sustainability.

2:34: It all adds up to, well, healthier margins.

2:36: So it’s really about creating this interconnected system.

2:40: Robots, machines, inspection—all communicating and adjusting autonomously.

2:45: Exactly, a fully automated autonomous ecosystem. And you know it’s important to remember this isn’t a switch you flip, right?

2:52: It’s a process.

2:52: Definitely it’s an ongoing journey of adding automation, refining it, making the system smarter over time—not a one-time project.

3:00: OK, that makes sense.

3:01: So the key takeaway here is that lights out…

3:04: While it sounds futuristic, is actually a tangible goal for manufacturing execs driven by advanced robotics and this autonomous control.

3:12: Precisely. It’s achievable—and actually, for listeners interested in really digging into that autonomous control aspect, how you make the robots and inspection work together so effectively, there’s a great…

3:24: Source—a white paper called Using Robotics and Automated Inspection in Manufacturing to Achieve Autonomous Process Control.

3:32: It dives much deeper into that specific mechanism.

3:35: Good to know.

3:35: We’ll make sure that’s available.

3:36: It really is fascinating to think about where this is heading, isn’t it?

3:39: The constant evolution.

3:41: Thanks for breaking that down today.

3:42: My pleasure.

3:42: It’s definitely an exciting field.

Why Factory Robotics Must Work for Everyone and How It’s Happening Now

Why Factory Robotics Must Work for Everyone and How It’s Happening Now

Advanced-robot-machine-tending-automate (2)

Wanted to thank Aaron Prather for featuring Flexxbotics in his recent article: “Robotics for the Rest of Us: Why Main Street Can’t Wait.” If you haven’t read the article yet, you can check it out here at this link: https://sixdegreesofrobotics.substack.com/p/robotics-for-the-rest-of-us-why-main

Aaron clearly points out that robotic automation must be made practical and accessible for businesses of all sizes. Basically, he’s saying that robots have to work without the custom science projects required today.

Production Robotics Reality

Sadly, most robot projects fail because they rely on custom, one-off software technology – especially in industries like medical devices, aerospace, and defense, where installations often become overly complex science projects.

At Flexxbotics, we’re fully aligned with Aaron’s vision. We believe that for robotic automation to truly scale across your factory, robot cells must be usable, adaptable, and modularized to be deployed and run by your teams.

And it’s not just about the robots. To be effective production robotic automation needs to be part of your factory’s operations, not just stand-alone technology in isolation. Robots must communicate with your factory’s machines to coordinate work execution for safe, continuous operation.

To run with any level of unattended autonomy, robots also need to receive instructions from your IT business systems about what jobs to run >> What parts to make, lot quantities, quality specs, other production info… In other words, robots must be part of your manufacturing process to scale out effectively.

Robot’s Way Forward

At Flexxbotics we call this Robot-Driven Manufacturing. It’s why we’ve created standardized robotic production software at the heart of the Flexxbotics solution. Unlike the custom automation integration projects required yesterday, we’ve made our solution powerful, flexible, and open so that it can be deployed quickly, adapted easily, and scaled rapidly in companies of all sizes.

The result? A modular solution for production robots that works for all different types of factories from the largest global organizations to smaller tier suppliers. Able to handle a wide range of parts from complex geometry parts and multi-part assemblies to simple stock parts. Even parts with ISO 2768 and ISO 286 precision tolerances including Class III orthopedics & implants.

Now, you can run multi-op process for multiple parts/SKUs across multiple machines. Robots can take your parts from multi-step machining through post-processing, cleaning, and even inspection.

You’re able to do multi-SKU as well for high volume / high mix environments with support for both line clear and non-line clear set-ups. Bar code scanning automatically calculates part quantities across multiple machines, and work order changeovers detect order completion and update part properties for the next order in-feed.

These kinds of capabilities are foundational for advanced robotic machine tending, robotic quality control, and robotic production lines, and represent the ‘tip of the iceberg’ of what Flexxbotics delivers.

It’s what Robot-Driven Manufacturing looks like in practice: automation that’s resilient, scalable, and straightforward to deploy, no matter your size or sophistication level.

Practical Production Robotics

Aaron calls for a shift in thinking – from complex, robot-only perspectives to more holistic and practical solutions. At Flexxbotics, we’ve embraced that perspective, and are providing a solution that’s as robust and adaptable as the businesses we serve.

Whether you’re optimizing a global factory footprint or single plant, your robotic automation should be a practical part of your overall production strategy in our view.

We all should continue championing the stories of businesses that embrace automation to drive innovation and operational excellence. In fact, if you’re interested in real world examples, you can check out this case study on Ruland Manufacturing achieving lights out manufacturing using Flexxbotics.

The future of smart factory robotics is about solutions that truly work for everyone. It’s happening. And we believe it’s a game-changer.

What are Common Challenges in Robotic Machine Tending?

What are Common Challenges in Robotic Machine Tending?

Challenges in Robot Machine Tending

Automating machine tending with robots in your factory provides a wide range of benefits from longer unattended runs and greater capacity to increased profit per part.

However, robotic automation presents certain challenges that are not always obvious. 

These include interfacing between the robots and CNCs and other machines, managing multi-machine operations, and part presentation for robots as opposed to humans to enable autonomous “lights-out” production. 

I’ll cover a few of the most common here today and you can learn more about these and others in our Complete Guide to Robotic Machine Tending Projects white paper.

Part Presentation In-Feed / Out-Feed

An often overlooked consideration in robot machine tending is that robots require consistent part presentation. Robots need parts consistently positioned for in-feed and out-feed operations. 

If parts are randomly aligned or jumbled, the robot may pick and load them incorrectly. This makes it important to organize part staging for robotic requirements.

Robot-to-Machine Interface

Another challenge in robotic machine tending is overcoming connection and communication incompatibilities between robots and machines and other equipment. Machine PLCs and protocols are not inherently compatible. 

The lack of standards often presents unanticipated issues and can be endlessly frustrating. Custom integrations offer limited functionality, are overly complex to install and difficult to maintain over time. Standard off-the-shelf interfacing solutions for interoperability such as Flexxbotics represent the best option in many cases.

Multiple Machine Robot Operation

When deploying robots across multiple factory machines and equipment assets, referred to as advanced robotic machine tending, process workflow considerations become critically important. 

Any combination of multi-machine, multi-part, multi-step operational requirements means the robots have to operate in a coordinated manner in the overall process. 

Managing the timing and coordination of tasks is crucial to assure consistent operation and avoid bottlenecks and unexpected stoppages. The robot must be able to transition between different machines and tasks without mistakes or unplanned downtime.

In addition, different machines and machine types often have different controllers with different protocols as noted previously which can complicate set-up and ongoing operation further. Standardized interfacing solutions like Flexxbotics become essential in these advanced configurations.

Achieving “Lights Out” Automation

“Lights out” operation where production runs continuously without human intervention requires more than just robots. 

Production process orchestration becomes essential including not just loading and unloading, but tool wear detection, defect identification, sorting, corrective action, and more. 

All must be fully automated and synchronized. This requires sophisticated interoperable coordination between the robots, factory machines, and other equipment, as well as, robotic production software that manages the parts, jobs, changeovers, workflows, and processes for unattended operation. 

Standard digital solutions such as Flexxbotics are intended for these types of complex smart factory robotic operation at scale.

If your company is undertaking new automation projects now or planning them for later in the year, you may want to take a look at our CNC Robot Machine Tending Essentials blog or get in touch with us here at Flexxbotics.

What is Industry 4.0? | AI Explainer

What is Industry 4.0? | AI Explainer

AI-Explainer-graphic-2

Check out the latest episode of our Flexxbotics | AI Explainer Podcast:

In this Flexxbotics | AI Explainer podcast, we’re covering more smart factory technology topics related to robotics and industrial digitalization. This audio summary breaks down the following concept for you to gain insights and discover important information on the topic.

Industry 4.0 – the fourth industrial revolution – represents a significant shift in manufacturing through the use of smart factory technologies. Key components include robotic automation, industrial internet connectivity using open standards, and six sigma levels of process control for ‘lights out’ production. The overarching goal is to create fully autonomous smart factories with increased efficiency, reduced waste, and higher profit margins. Transformation occurs over time and is foundational for the future introduction of machine learning and artificial intelligence. Industry 4.0 delivers self-regulating production processes with greater visibility, agility, and continuous optimization which increases output capacity and yields while reducing waste and downtime leading to significantly higher operating margins.

Whether you’re a manufacturing leader or just curious about the future of next generation automation, this AI generated summary gives you a clear understanding of how robotic digitalization is changing Industry 4.0 ‘lights out’ production. Plus, it references additional resources to help you stay ahead of the curve. Check out this insightful summary on the future of autonomous manufacturing and the limitless potential.

You can also get and listen to this recording directly on Apple Podcast, Spotify, and Youtube.


0:03: All right, everybody, welcome back.

0:05: I am pumped for today’s deep dive.

0:06: We’re going deep on industry 4.0.

0:09: Yeah, this is exciting stuff, really is.

0:11: You know, we’ve got robots, we’ve got AI, smart factories.

0:15: It really feels like we’re stepping into the future of manufacturing.

0:19: Absolutely, you hit the nail on the head, and we’re seeing this transformation happen right before our eyes.

0:23: So let’s, let’s just jump right in.

0:25: For someone in manufacturing like.

0:27: What is industry 4.0 really all about?

0:30: So it’s more than just a buzzword, you know, it’s really a paradigm shift in how we approach manufacturing.

0:37: You know, we’re moving from a world of, you know, isolated machines to a fully interconnected and intelligent ecosystem.

0:45: Ecosystem.

0:45: OK.

0:46: We’re not just talking about like swapping out a few old machines for some fancy new robots, right?

0:49: Right?

0:50: It’s a much more holistic approach.

0:51: It’s a journey and not a destination.

0:53: But where do we even start?

0:55: What are like the core components of this whole industry 4.0 thing?

0:58: Well, you know, you have to start with the foundation, and that’s robotics and automation.

1:02: OK, robots, everybody loves robots, but I think people hear robots in manufacturing and they think, you know, big clunky arms welding car parts, right?

1:11: And it’s so much more than that now.

1:13: Think advanced robotic machine tending.

1:15: Robots that can handle incredibly complex tasks adapt to changes in the production process, you know, real-time decision making.

1:23: So these robots, they’re not just replacing human workers, they’re like collaborating with them.

1:27: Exactly.

1:27: It’s all about creating a seamless workflow, human and machine working together for maximum efficiency and productivity.

1:35: OK, so robots are definitely cool.

1:38: But they’re just one piece of the puzzle, right?

1:40: Absolutely.

1:41: You need a way to connect all these robots, machines and systems, and that’s where industrial internet connectivity comes in.

1:47: All right, so we’re talking about the internet of things, but for factories, precisely.

1:52: So instead of having all these separate silos of information, you have this free flow of data throughout the entire factory.

1:57: Exactly.

1:58: It’s like giving the factory a central nervous system.

2:00: OK, I’m getting the picture.

2:02: So we’ve got the robots, we’ve got them all connected.

2:04: What’s next?

2:05: Well, that’s where things get really interesting.

2:07: We’re talking about autonomous process control.

2:09: OK, break that down for me.

2:11: Imagine software that’s constantly analysing all the data coming in from the factory floor, learning from it, and making adjustments in real time to optimise the entire production process.

2:23: And with all this automation and data analysis, we’re talking about some pretty.

2:27: Curious efficiency gains, right?

2:28: Absolutely.

2:29: Think 6 sigma levels of quality, lights out production, the kind of efficiency that was once unimaginable.

2:35: Wow, it sounds like industry 4.0 is really pushing the boundaries of what’s possible in manufacturing.

2:41: It is, and the best part is it’s just the beginning.

2:44: As AI and machine learning continue to advance, we can only imagine what the future holds.

2:49: It’s an exciting time to be in manufacturing.

2:52: I feel like we’ve only just scratched the surface of what’s possible with Industry 4.0.

2:56: I agree it’s a journey and it’s one that I’m excited to be a part of.

2:59: Well, if our listeners are ready to start their own industry 4.0 journey, where should they go?

3:05: I’d recommend checking out the white paper using robotics and automated inspection and manufacturing to achieve autonomous process control.

3:14: It’s a great starting point for anyone looking to learn more about the practical applications of these technologies.

3:20: Sounds like a great resource.

3:22: Well, thanks for taking us on this deep dive into industry 4.0.

3:25: It’s been an eye opener for sure.

3:27: Until next time, keep innovating.

3:29: Absolutely.

What is Autonomous Manufacturing? | AI Explainer

What is Autonomous Manufacturing? | AI Explainer

AI-Explainer-graphic-2

Check out the latest episode of our Flexxbotics | AI Explainer Podcast:

In this Flexxbotics | AI Explainer podcast, we’re covering more smart factory technology topics related to robotics and industrial digitalization. This audio summary breaks down the following concept for you to gain insights and discover important information on the topic.

Autonomous Manufacturing is automated, self-governing smart factory operations, a key element of Industry 4.0, which uses robots and robotic production software digitalization along with existing systems to optimize production with minimal human involvement. Achieving autonomous manufacturing requires attaining autonomy in production process control and typically involves an incremental implementation. Autonomous manufacturing uses robots to self-adjust production processes for consistent, high-quality output. The benefits include increased capacity, improved product quality, and higher EBITDA profit margins.

Whether you’re a manufacturing leader or just curious about the future of next generation automation, this AI generated summary gives you a clear understanding of how robotic digitalization is changing Industry 4.0 ‘lights out’ production. Plus, it references additional resources to help you stay ahead of the curve. Check out this insightful summary on the future of autonomous manufacturing and the limitless potential.

You can also get and listen to this recording directly on Apple Podcast, Spotify, and Youtube.


0:03: Hey everyone, welcome back.

0:05: Ready for another deep dive?

0:07: Today, we’re exploring something pretty fascinating—something that’s already started to change how things are made.

0:12: Yeah, it’s a pretty hot topic right now in the manufacturing world.

0:16: We’re talking about autonomous manufacturing.

0:18: That’s right, autonomous manufacturing.

0:20: And even though it sounds like robots taking over the factory, it’s actually a lot more nuanced than that, and that’s what we’re going to dive into today.

0:28: It’s a journey, right?

0:30: Not just flipping a switch.

0:31: Exactly—a journey. And we’re going to explore what that means for businesses.

0:36: I think the best way to kick this off is to think about it like this:

0:41: Imagine a self-driving car.

0:44: But for a factory.

0:46: I like that analogy.

0:47: It really captures the essence because, just like with a self-driving car, we’re talking about a system that can make decisions and take actions based on data without constant human intervention.

0:58: So how does this whole thing work? What does autonomous manufacturing actually look like on the factory floor?

1:05: Picture this:

1:07: You walk into a factory and see robots working alongside humans.

1:11: You’ve got collaborative robots—or cobots, as they’re called—assisting with tasks that require precision and dexterity.

1:18: Cobots.

1:19: I like that.

1:20: Right, it’s kind of a catchy name.

1:21: Then you’ve got industrial robots doing the heavy lifting, handling repetitive tasks that are tough on human workers.

1:29: But it’s not just about the robots, is it?

1:30: It’s the way it all comes together.

1:32: Absolutely.

1:33: It’s about connecting those robots, integrating them with existing IT systems, and using specialized software to orchestrate the entire operation.

1:38: It’s like a symphony—everything working together in harmony.

1:44: So, is there a “brain” behind all this?

1:47: You could say that.

1:48: There’s something called autonomous process control.

1:51: It’s basically a closed-loop system where robots adjust the production process in real time based on data from automated inspections.

2:01: OK, so I’m starting to see how this can lead to some pretty significant benefits.

2:05: Oh, absolutely, and that’s the exciting part! We’re talking about a potential increase in production capacity—anywhere from 45% to even 100% in some cases.

2:16: That’s a game changer for businesses.

2:18: And fewer defects, right? The robots are so precise.

2:22: Exactly.

2:23: We’re talking about a reduction in defects of around 30% or more.

2:27: That translates to higher-quality products, less waste, and improved profit margins.

2:34: So this isn’t just about futuristic technology.

2:37: It’s about making businesses more efficient and competitive.

2:40: That’s exactly it.

2:41: It’s about empowering businesses to operate at their peak, deliver high-quality products, and stay ahead of the curve.

2:47: For anyone intrigued by autonomous manufacturing, what’s a good first step?

2:55: A great place to start is checking out the white paper called Using Robotics and Automated Inspection in Manufacturing to Achieve Autonomous Process Control.

3:03: Catchy title.

3:04: It gets right to the point. It dives into the nuts and bolts of how this technology works and how it can be applied in different manufacturing settings.

3:13: Awesome.

3:14: And for everyone listening, remember: keep those minds curious and keep exploring.

3:19: The future is autonomous.

15 Point Project Planning Outline for Robot Machine Tending

15 Point Project Planning Outline for Robot Machine Tending

project-planning-outline-for-robot-machine-tending

Wanted to share our recently published white paper which is a Complete Guide to Robotic Machine Tending Projects.

The paper provides comprehensive info on the different aspects of a machine tending initiative using either cobots or industrial robots to achieve greater unattended operation, higher yields, and better margins. 

If you haven’t gotten it yet, you can download the full 51 page white paper guide here.

Included in the paper are several practical tools that’ll help successfully guide you through your factory’s robotic automation projects.

One of these is a 15 Point Project Planning Outline which you can use as the basis for developing a structured roadmap for your production robotic initiative.

These points are important steps that if missed can cause projects to fail. It’s particularly relevant to CNC robot machine tending projects.

Planning outline covers:

  1. Business Goals & Target Outcomes
  2. Selecting Operations to Automate
  3. Requirements & Constraints
  4. Budgeting & Return On Investment (ROI)
  5. Internal Communications Plan
  6. Identifying Parts & Part Families
  7. Throughput Volume & Cycletimes
  8. Objective-based Design
  9. Robot+Machine Connectivity
  10. Business Systems Connectivity
  11. Safety & Risk Assessments
  12. Validation Testing
  13. Documentation & Training
  14. Ramping Volumes
  15. Maintenance & Support

Here’s where you can download the full 15 Point Project Planning Outline

And, if you’re currently organizing for your next robotic automation project – especially if it’s an Advanced Robotic Machine Tending setup – you’ll probably want to learn how Flexxbotics is redefining robot-driven manufacturing.

And we offer turnkey solution implementation services and support for robot machine tending installations from design and deployment through validation and optimization as well as ongoing operation and maintenance. You can Contact us directly to discuss your project needs.

CNC Robot Machine Tending vs Advanced Robotic Machine Tending; What’s the Difference?

CNC Robot Machine Tending vs Advanced Robotic Machine Tending; What’s the Difference?

cnc-robot-machine-tending-vadvanced-robotic-machine-tending-differences

Today, I want to take look at the difference between basic CNC robot machine tending and Advanced Robotic Machine Tending.

While there are a number of differences, the key distinction is that basic machine tending involves a single robot with one machine whereas advanced machine tending involves one or more robots with multiple machines. It could be two, three, five, or more machines being tended at the same time in advanced robotic machine tending setups.

Here are some basic definitions:

What Is CNC Robot Machine Tending?

Basic robotic machine tending automates simple steps such as loading raw materials into CNCs and unloading finished parts. Production robotic automation can be applied to CNCs and other factory machines using different types of robots – typically either industrial robots or power & force-limiting robots known as collaborative robots – which improve machine uptime operation, productivity, and output.

What Is Advanced Robotic Machine Tending?

Advanced robotic machine tending expands the capabilities of basic robot machine tending to enable the robot to operate multiple machines for a wider range of parts with multiple work orders in multi-step operations such as different machining ops, deburring, inspection, sorting, serialization, and/or assembly, all within a single workflow. For example, a robot can load workpieces into several CNC machines, perform wash down and blow-off cleaning, move the finished parts to an automated inspection machine, and then sort the parts based on inspection results. Sophisticated set-ups will include the ability to update and correct the machine programs’ processing instructions (offset parameters) based on inspection results to avoid nonconformances, which is called autonomous process control.

So, in addition to multiple machines being tended by the robots, advanced robotic machine tending often involves multiple parts or SKUs with multiple operations and also involves multiple process steps all orchestrated for continuous unattended operation.

These advanced machine tending deployments are what we do at Flexxbotics, and what we believe is the key to autonomous manufacturing.

If you’re interested in more, check out our Complete Guide to Robotic Machine Tending Projects

What is Autonomous Process Control? Flexxbotics | AI Explainer Podcast

What is Autonomous Process Control? Flexxbotics | AI Explainer Podcast

AI-Explainer-graphic-2

Check out the latest episode of our Flexxbotics | AI Explainer Podcast:

In this Flexxbotics | AI Explainer podcast, we’re covering more smart factory technology topics related to robotics and industrial digitalization. This audio summary breaks down the following concept for you to gain insights and discover important information on the topic.

Autonomous Process Control (APC) is a solution using robots and automated inspection to achieve high-precision, repeatable manufacturing without human intervention. Key components include industrial and collaborative robotics, automated inspection technologies, and standardized robotic production software enabling interoperability and process optimization. APC improves quality, yields, and compliance through continuous monitoring and processing adjustments. The result is enhanced profitability due to reduced defects, scrap, and rework, leading to higher margins. Ultimately, APC is the necessary foundation for fully autonomous manufacturing.

Whether you’re a manufacturing leader or just curious about the future of next generation automation, this AI generated summary gives you a clear understanding of how robotic digitalization is changing Industry 4.0 ‘lights out’ production. Plus, it references additional resources to help you stay ahead of the curve. Check out this insightful summary on the future of autonomous manufacturing and the limitless potential.

You can also get and listen to this recording directly on Apple Podcast, Spotify, and Youtube.

0:00: Hey, everyone.

0:00: Welcome back.

0:01: Ready to jump into another deep dive.

0:03: Today, we’re gonna be talking about something that I think is really transforming the manufacturing landscape.

0:07: And that’s autonomous process control.

0:09: Specifically when we’re thinking about, you know, advanced robotic machine tending.

0:15: And this is all about achieving that repeatable precision that leads to better profitability, but break it down for me a little bit sure.

0:27: What does autonomous process control actually mean?

0:30: What am I looking at?

0:31: If I were to walk onto a factory floor where this is happening?

0:34: So you’re going to see robots working with your existing machines.

0:37: So you know, think CNC machines, injection molding machines was that kind of thing.

0:41: But and this is the key, they’re not just blindly following program, they’re paired with these automated inspection systems that are constantly feeding back data on what’s happening in the process.

0:55: And then the whole system is looking at that data and it’s making adjustments in real time to keep production happening at an optimal level, it’s self governing.

1:05: So walk me through then the technology that makes this possible, like what are the building blocks here?

1:11: So there are three core components first you have your robots but not just any robots.

1:16: We’re talking about robots designed for machine tending.

1:19: So they’re able to interface with your specific machines.

1:23: They could be traditional industrial robots, you know the big, the big arms.

1:27: Exactly, or they could be collaborative robots.

1:31: So which type of robot you need?

1:33: Depends on your process and your environment makes sense.

1:38: OK.

1:38: So we’ve got the robots.

1:39: What’s next?

1:40: Next?

1:40: You have your inspection technologies, vision systems are very common, especially for dimensional checks.

1:47: You might also use laser scanners, coordinate measuring machines depending on the application, all sorts of sensors that are measuring different parameters and these act as like the eyes and ears of the system.

1:59: They’re feeding all that information back to the brains of the operation.

2:03: Got it.

2:03: But the real magic happens in the software.

2:06: It’s a software that ties everything together.

2:08: It allows the robot to communicate with the different machines.

2:12: It processes the data from the inspection system and it uses algorithms to determine the optimal adjustments to make.

2:21: So we’ve got the brawn, we’ve got the senses.

2:23: What’s what makes up the brains, the brains is the specialized software and this is where things get really interesting.

2:30: We’re not talking about just basic programming here.

2:33: This is sophisticated stuff.

2:35: We’re talking about control algorithms, statistical process control.

2:39: This means the system isn’t just reacting to problems.

2:42: It’s constantly crunching data, looking for trends, predicting potential deviations and making tiny little micro adjustments to keep everything running smoothly.

2:53: So it’s preventing issues before they even arise.

2:56: That’s amazing.

2:57: So I mean, I hear a lot of, you know, hype about a lot different technologies give it to me straight.

3:02: Like what are the real world bottom line benefits that I can expect to see from implementing autonomous process control.

3:09: First of all, because the system minimizes variability, you get much more consistent quality parts are produced at tighter tolerances, defects are caught early, less waste from rework.

3:21: And then because the process is continuously being optimized, you often see increases in production yields depending on the application.

3:29: You might see a 25% increase sometimes even more.

3:33: Wow.

3:34: So we’re not just talking about like efficiency here, we’re talking about like actually driving profitability, reduce waste, higher output consistent quality that all feeds into a lower cost of quality overall.

3:46: And that translates to better profit margins and a real competitive edge in the market.

3:51: So paint a picture for me, what would this look like in, in a real world setting?

3:56: Like if I were to walk onto, you know, a factory floor, what kind of setup am I looking at?

4:00: Sure.

4:01: So let’s imagine you have AC NC Machining line making high precision parts.

4:05: So you might have a robot arm that’s equipped with specialized grippers, loading raw materials into the CNC machine and then unloading the finished parts.

4:13: And while that’s happening, you have a separate laser measurement system that’s constantly checking the dimensions of each part makes sense.

4:20: And if that system sees that a part is even a little bit out of spec it signals the software, the software then adjusts the CNC machines parameters in real time.

4:30: Oh, wow.

4:30: So you’re correcting the issue before the next part’s even started.

4:34: That’s incredible.

4:35: I mean, this sounds like honestly something straight out of the future, but this is something that manufacturers can implement now, right?

4:41: Like this is this is happening now.

4:42: OK.

4:43: That’s amazing.

4:44: The technologies are mature and like we’ve been talking about the return on investment can often be seen in less than a year.

4:52: So it’s a really compelling proposition for any manufacturer who wants to, you know, stay ahead of the curve for sure.

4:59: Well, this has been fascinating for anyone who’s listening and wants to learn more about this whole idea of using robotics and automated inspection to achieve this level of control in their factory.

5:10: There’s a fantastic article in quality magazine called using robotics and automated inspection in manufacturing to achieve autonomous process control.

5:21: Definitely check it out if this is something you’re considering.

5:23: And really what I want everyone to take away from this is think about it, which of your processes could benefit from this level of precision, this efficiency and ultimately this profitability because autonomous process control really might be the key to unlocking the full potential of your factory.

5:40: Couldn’t agree more.

5:42: All Right.

5:42: Well, thanks so much for joining us.

5:43: This has been another great deep dive until next time.

5:46: See you then.

CNC Machine Tending Essentials – How to automate your CNCs with robots

CNC Machine Tending Essentials – How to automate your CNCs with robots

Expanded Business Systems Integration & Analytics in Flexxbotics Solution

Expanded Business Systems Integration & Analytics in Flexxbotics Solution

Business System Integrations

Over the last couple of week’s, I’ve highlighted some of the new functionality added in the latest release of our Flexxbotics solution for robot-driven manufacturing including multi-factory power and in-line quality inspection. 

There’s a couple more new capabilities I’d like to give a quick rundown on today. 

The first is that we have expanded the IT systems integration capabilities to include a whole range of enterprise business systems including SAP, Oracle, Siemens and many others for digital process integration.

Our modern architecture works with all your existing systems including ERP/MRP, MES, QMS, PLM/PDM, DNCs, CAD/CAM, SCADA/HMI, IIoT, and of course all the custom systems you have in place already. That’s the point; Flexxbotics is designed to work with everything your company already has.

We’ve also expanded the analytics functionality in our solution with even more dashboards, KPIs, reports and analytical capabilities so you get even deeper analysis of your operations. 

Our dashboards include Utilization, Cycle Performance, Part Throughput, Yield, Failure Reasons, Downtime Reasons, OEE and more along with additional REST API capabilities for your corporate business intelligence tools to ensure you can run comprehensive production analytics and factory optimization at all times. 

We are really excited by the new and expanded functionality in our solution and how it can make an impact on your business. A recent article in Manufacturing.Net sums it up nicely: 

“With this new version of the Flexxbotics solution, global companies can implement advanced robotic machine tending that enables autonomous process control at scale across multiple sites to increase capacity, production yields and EBITDA profitability”

And we’re not stopping there, keep an eye out for our next solution capability announcement which makes the robots even smarter. Stay tuned!

To learn more about Flexxbotics Solution visit our Solutions Overview page.

In-Line Quality Inspection Capabilities with Flexxbotics Solution

In-Line Quality Inspection Capabilities with Flexxbotics Solution

Analytics-Screens

In last week’s blog, I talked about our latest release of the Flexxbotics solution for robot-driven manufacturing and the new multi-factory power.

Some of the other functionality that I’m excited about is the expansion of our in-line inspection capabilities, which use automated inspection results to drive real-time updates to off-sets in CNC machining programs which can significantly reduce rework and scrap.

What does it mean for you? This article in Design News summarizes it well:

“With in-line inspection, Flexxbotics orchestrates the fleets of robots in the smart factory to achieve continuous unattended operations enabling higher yields, greater throughput and increased profit per part.”

Flexxbotics takes automated inspection results for each part, we then run statistical process control (SPC) in real-time, and instruct the robots to sort any nonconformances and perform rework. In addition, you have the option to make autonomous updates to the CNC machine’s programs if you choose which can really cut your defect rate. We have implementations where we’ve reduced nonconformances by over 50%.

Closed-loop autonomy in the workcell is the critical capability that enables autonomous process control, which we believe is the foundation for true autonomous ‘lights-out’ manufacturing.

All types of inspection equipment can be included in-line – such as probes, vision systems, lasers, and Coordinate Measuring Machines (CMMs) – with the robots using the inspection results to make real-time modifications to the parameters/variables/macros in the PLC programs to adjust for processing changes, tool wear, and other factors.

This enables robotic production autonomy on even the most complex geometry parts with the highest level of precision. 

In the last few weeks, we have already announced robot compatibility for in-line inspection with Hexagon, Cognex, Renishaw, SICK equipment, and have enabled many others that we will be announcing soon.

Stay tuned for more news as the team rapidly expands our range of compatibility which is already 1000+ makes & models of inspection equipment, CNCs and other machinery.

To learn more about Flexxbotics Solution visit our Solutions Overview page.

Flexxbotics Solution Scales for Multi-Factory Deployments

Flexxbotics Solution Scales for Multi-Factory Deployments

Factory-Screens

We recently announced the latest release of our Flexxbotics solution for robot-driven manufacturing with autonomous process control. 

Included in the release are several new and expanded capabilities that the team has been working on to further enhance our solution such as multi-factory power, expanded in-line inspection functionality, more IT business system integration capabilities, analytics, and support for mobile tablets and smartphones. 

If you missed this announcement, you can take a look at what’s new here. 

One of the capabilities that I am most excited about is the multi-factory power. It provides a control room dashboard enabling command and control of robot-enabled workcells across your entire factory footprint. 

Our experience with leading manufacturers in medical, aerospace, automotive, defense, and electronics is that enterprise control across multiple sites is critical. Large companies need full visibility to robots+CNC machines operating simultaneously in “lights-outs” manufacturing. 

Our cockpit functionality enables fleets of production robots connected to a large variety of workcell machines with compatibility to thousands of makes & models of CNCs and inspection equipment, plus other factory machinery such as laser markers and additive manufacturing machines. 

This is made possible by our breakthrough FlexxCORE technology which is the unique software infrastructure inside the Flexxbotics solution that enables robot+machine interoperability.

FlexxCORE is a low-code environment for composing and running connectors that includes a highly secure, high-performance run-time framework for connectivity and communication between robots and all different types of factory assets.

With this new version of the Flexxbotics solution global companies can implement advanced robotic machine tending that enables autonomous process control at scale across multiple sites to increase capacity, production yields, and EBITDA profitability.

To learn more check out our Flexxbotics Latest Release video (1 min)


Industry 4.0: the interoperability issues impeding robotics use in smart factories

Industry 4.0: the interoperability issues impeding robotics use in smart factories

iot-insider-flexx

I recently got together with Kristian McCann at IoT Insider for a Q&A on the role of robotics in Industry 4.0/5.0, applications of robots in factories and some of the challenges during implementation. 

A major issue we discussed that is limiting the success of smart factory digitalization initiatives is the lack of interoperability between the robots and machines. When the robots are disconnected and unable to communicate with the machines in the factory due to interfacing complexity and incompatibilities efficiency gains are reduced and unplanned downtime issues occur. 

We believe that interoperability between robots and machines in the factory is critical to achieving ‘lights-out’ manufacturing. That’s why the Flexxbotics solution – with our breakthrough FlexxCORE™ technology – seamlessly connects and coordinates robots with existing machines, other factory machinery, inspection equipment, IT, and business systems. 

We’re already compatible with hundreds of makes and models of machines and systems, and we have the ability to add more quickly.

Read the article in full here to learn more: https://www.iotinsider.com/industries/industrial/industry-4-0-the-interoperability-issues-impeding-robotics-use-in-smart-factories/


Scott Harris Makes New Investment in Flexxbotics

Scott Harris Makes New Investment in Flexxbotics

Scott-Harris-Investor-&-Advisor

Author: Tyler Bouchard, Co-founder & CEO of Flexxbotics 

We’re pleased to announce that Scott Harris, co-founder of SOLIDWORKS and Onshape, has invested in Flexxbotics. Scott has been an advisor and mentor to me for a number of years as we’ve been scaling up Flexx. This investment marks an exciting development as we continue to innovate in smart factory robotics software solutions.

Scott Harris is a renowned figure in the world of manufacturing software and CAD, and he brings a huge amount of knowledge and experience to our team. His involvement has helped shape our vision and the way we think about our cloud services and software+hardware interfacing.

As we developed our FlexxCORE™ technology – our unique breakthrough – he made it clear that seamlessly connecting and coordinating robots with existing automation equipment would be a real challenge given all the incompatibilities. The result was our laser focus on making it more powerful, flexible and open than had been done previously.

We both believe that interoperability between robots and machines in the factory will be critical to achieving ‘lights out’ manufacturing. That also led to our realization of the importance of process control.

The ability for next-gen machining environments using robotics to truly achieve autonomous manufacturing relies on their ability to first achieve autonomy in  process control.

Scott’s practicality in thinking about these types of scenarios has really led to some of our most groundbreaking work. Connectivity and bi-directional communication are necessary foundations to orchestrate robots and equipment in the smart factory.

From my perspective as someone who has been in manufacturing technology my entire career, Scott’s two systems have had a profound impact on how we all design and make products. Both SOLIDWORKS, acquired by Dassault Systèmes, and OnShape, acquired by PTC have redefined the industry forever. 

This investment and Scott’s continued mentorship will help us as we accelerate our engineering efforts and expand our product offerings. Our collaboration not only strengthens our position, it also consistently brings us an exceptionally innovative perspective to this rapidly evolving field of robot-driven manufacturing in the era of Industry 4.0 digitalization.

The rising demand for robotic machine tending

The rising demand for robotic machine tending

The rising demand for robotic machine tending

In this distributor insights video, Tim Anderson, Sales Director at Automation Inc. covers the rising demand for robotic machine tending.

Established in 1981, Automation, Inc. is a Minneapolis based value-added stocking distributor of motion, machine vision, robotics, pneumatic, electrical, process control, and machine components.

This interview covers:

  1. Tell us about yourself and Automation Inc.
  2. What are the main industries for machine tending?
  3. What challenges does machine tending solve?
  4. What are the benefits that customers will see as soon as they automate.

Automation Inc. is a Flexxbotics Distributor Partner. We have an extensive network across North America and Europe. Reach out today if you’d like become a part of our fast growing distributor community.

Find out more about Flexxbotics: https://flexxbotics.com/about/

Learn about Flexxbotics’ Robotic Driven Machine Tending solution here. https://flexxbotics.com/solutions/

https://www.youtube.com/watch?v=7l_NWRoMQvI
How to adopt flexible CNC automation

How to adopt flexible CNC automation

How to adopt flexible CNC automation

In this partner insights video, Mike DeGrace, UR+ Ecosystem Manager at Universal Robots covers adopting flexible CNC automation.

Founded in 2005 by three university students in Denmark, Universal Robots was the first company to deliver commercially viable collaborative robots – and transforming companies and entire industries.

The interview covers:

  1. Could you tell us about yourself and what you do at Universal Robots?
  2. What industries do you see the most for machine tending?
  3. What challenges are your customers looking to overcome?
  4. How does CNC automation help them overcome these challenges?
  5. What makes for a successful automation project?
  6. What are they key benefits customers see after they start automating their CNCs?
  7. How does Flexxbotics help CNC machine shops to achive their automation goals?

Universal Robots is a Flexxbotics Strategic Partner. Flexxbotics greatly values our partner relationships. We have an extensive partner network across North America and Europe. Reach out today if you’d like become a part of our fast growing community.

Learn about FlexxTend™ – The complete automated machine tending solution here. https://flexxbotics.com/flexx-tend/
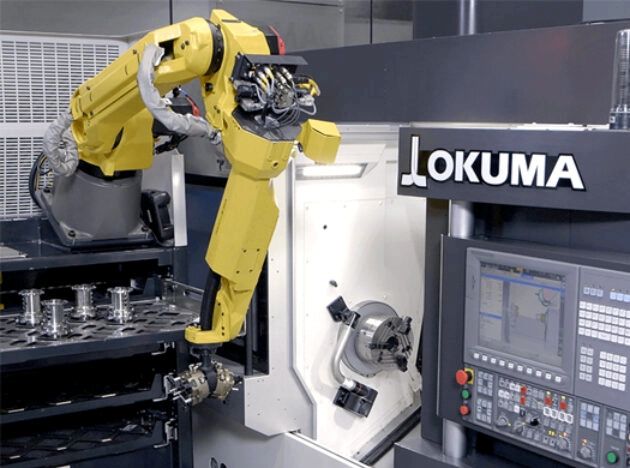
https://www.youtube.com/watch?v=7rMZ-wyPJQo
What makes for a successful automation project?

What makes for a successful automation project?

What makes for a successful automation project?

In this partner insights video, Anthony Gillespie, Territory Sales Manager at Schunk covers CNC automation and how automating can overcome the most common machine tending challenges.

Schunk is the international technology leader in toolholding and workholding, gripping technology and automation technology. It has its roots at its headquarters in Lauffen/Neckar. The company was founded here in 1945 by Friedrich Schunk as a mechanical workshop. Under the management of his son Heinz-Dieter Schunk, Schunk evolved into a global player and the world’s leading technology supplier for robots and production systems.

This interview covers:

  1. What industries do you see the most for machine tending?
  2. What challenges are your customers looking to overcome?
  3. How does CNC automation help them overcome these challenges?
  4. What makes for a successful automation project?
  5. What are the benefits your customers are seeing since automating their CNC machines?

Learn about FlexxTend™ – The complete automated machine tending solution here. https://flexxbotics.com/flexx-tend/
https://www.youtube.com/watch?v=ubLPRKkFdFo
WPI Sponsorship

WPI Sponsorship

WPI Sponsorship

Flexxbotics Sponsors WPI Undergraduates

Flexxbotics was pleased to sponsor three students from Worcester Polytechnic Institute (WPI) for their senior year capstone major qualifying project.

For the project, Mayank Govilla, Brian Francis and Niko Neathery successfully researched, designed and implemented a robust solution for integration of the FlexxConnect™ automated process control platform to monitor specific robot performance metrics.

The project was a huge success and we really appreciate the efforts and contribution from the students.

With several Flexxbotics staff including both of our founders being WPI Alumni, it was an honor to give back and provide this sponsorship, and we look forward to continuing to support WPI in the future.

View more of our latest news.

Adopting CNC Automation to Meet Demand Growth

Adopting CNC Automation to Meet Demand Growth

Flexxbotics Customer Spotlight - Machining Concepts

In this video, Jackson Brining, Automation and Process Engineer at Machining Concepts talks about adopting CNC automation to meet growing demand.

This interview covers:

  1. Tell us about Machining Concepts
  2. What are the main benefits of working with Machining Concepts?
  3. What were the challenges you were facing in advance of adopting cobot automation?
  4. How has robotic machine tending helped you to overcome these challenges?
  5. How did Flexxbotics help you to achieve your automation goals faster?
  6. What are some of the specific improvements you have seen automating your CNC?

Learn how you can adopt Robot-Driven Manufacturing today https://flexxbotics.com/solutions/
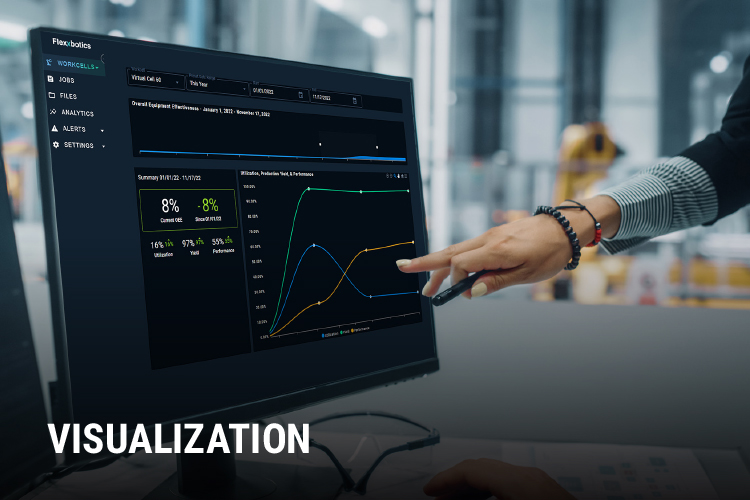
https://www.youtube.com/watch?v=Z-E0js6_YS0
Automate 2023

Automate 2023

Automate 2023

Flexxbotics to present machine tending solutions at Automate 2023

Flexxbotics will showcase its FlexxTend™ complete robotic machine tending solution at Automate 2023 on May 22-25 in Detroit, Michigan.

Powered by FlexxConnect™, and its breakthrough innovation, the patented Hardware Abstraction Core technology, FlexxTend™ makes your CNC automation goals a reality by having your cobots tending your machines in 2 months from project start.

Flexxbotics will be located at Booth #147.

Automate is the premier show for anyone who works with or is interested in automation. With 750+ exhibitors showing the latest cutting-edge robotics, vision, AI, motion control and related automation technologies.

Tyler Bouchard, Co-founder & CEO at Flexxbotics, said: “We’re excited to be at Automate again this year. If you’re a manufacturer looking to adopt CNC automation and attending the show, please reach out, we would love to meet.”

Contact us to arrange a meeting

Northwest Machine Tool Expo 2023

Northwest Machine Tool Expo 2023

Northwest Machine Tool Expo

Flexxbotics on show at Northwest Machine Tool 2023

Flexxbotics will exhibit at the upcoming Northwest Machine Tool Expo with our partner Olympus Controls. The Expo will take place on May 10-11, 2023 at the Oregon Convention Center in Portland, Oregon.

Northwest Machine Tool Expo is a unique regional event for the machining and manufacturing industries. It features several educational sessions and an exhibition floor showcasing the latest products and services in the industry.

If you are attending, be sure to stop by Olympus Controls Booth #915 to learn about our joint turnkey machine tending solution that makes your CNC automation goals a reality in 8 weeks.

Lance Price, Senior Robotics Sales Specialist at Olympus Controls said: “We’re excited to demo our latest robotic machine tending solutions with Flexxbotics. Please reach out if you are at the show, we would love to meet.”

Book a meeting with us at the Northwest Machine Tool Expo

FlexxCNC™ Compatibility Expansion

FlexxCNC™ Compatibility Expansion

FlexxCNC Compatibility Expansion

Flexxbotics expands FlexxCNC™ to include Hurco,
Siemens & Heidenhain compatibility

Flexxbotics is excited to announce that we have expanded the functionality of our FlexxCNC™ cobot to CNC communications interface to include compatibility with Hurco, Siemens and Heidenhain controllers.

The FlexxCNC™ interface enables machine shops to integrate their Universal Robot cobot onto any machine in their shop in half a day. FlexxCNC™ forms an important element of our FlexxTend™ complete automated machine tending solution.

FlexxTend™ is the leading choice for machine shops looking to adopt CNC automation but are busy getting parts out of the door. FlexxTend™ takes care of the whole process for you. Our team designs everything to your specification and can be onsite integrating, validating and training 6 weeks later.

FlexxCNC™

FlexxCNC™

FlexxTend™

FlexxTend™

Tyler Bouchard, Co-founder & CEO, comments: “We are pleased to expand the FlexxCNC™ library to support even more controller types and in-turn strengthen the FlexxTend™ platform.”

Tyler continues: “We are seeing strong demand for FlexxTend™ from machine shops across North America that are ready to automate their CNC’s to either solve the labor shortage or increase throughput. If this sounds like your shop, give us a call, we’d love to help.”

Learn more about FlexxTend™

5 Tips For Hiring a CNC Machinist During a Labor Shortage

5 Tips For Hiring a CNC Machinist During a Labor Shortage

5 Tips For Hiring CNC Machinist During a Labor Shortage

In today’s competitive job market, it is increasingly difficult to find skilled workers in certain industries. CNC machining is no exception. There is a global shortage of experienced machinists to operate the complex machinery and produce parts. So how should machine shops go about the hiring process? This article provides 5 tips that will help.

Look Beyond Traditional Hiring Methods

1. Look beyond traditional hiring methods

During a labor shortage, it is important to think outside of the box when it comes to finding and attracting talent. Instead of relying solely on job boards or recruitment agencies, consider reaching out to local trade schools, technical colleges, and other training programs. These institutions often have graduates who are looking for work and may be a perfect fit for your shop.

Invest In Training and Development

2. Invest in training and development

CNC machining is complex and requires ongoing training and development. Investing in training helps to upskill your existing workforce. This often leads to higher job satisfaction and increased value/contribution to your machine shop. Examples include on-the-job training, attending industry conferences and trade shows, and offering tuition reimbursement for advanced education.

Create a Positive Work Environment

3. Create a positive work environment

A positive work environment is vital for attracting and retaining talent. Things like flexible work schedules, a comfortable workspace, and opportunities for professional growth. By creating a culture of respect, collaboration, and continuous improvement, you can build a team of skilled machinists who are dedicated to your organization’s success.

Streamline Your Hiring Process

4. Streamline your hiring process

Having a long-drawn-out hiring process is one of the biggest mistakes you can make during a labor shortage. By simplifying your application and interview process, providing clear job descriptions and expectations, and timely feedback you have the best chance of securing talent, quickly.

Consider CNC Automation

5. Consider CNC automation

Machine shops are increasingly turning to CNC automation to help solve the labor shortage. By adopting robotic machine tending, not only can you alleviate the challenge of hiring and retaining skilled machinists, but you can increase productivity and reduce operational costs. Automation can also free up your skilled workers to focus on more complex tasks, and gives you a competitive edge when hiring new talent.

In summary, hiring skilled CNC machinists during a labor shortage can be hard, but it is not impossible. By looking beyond traditional hiring methods, investing in training and development, creating a positive work environment, streamlining your hiring process, and considering CNC machine tending automation, you can find and hire the best talent for your machine shop.

Learn more about CNC automation here

PMTS 2023

PMTS 2023

PMTS Show

Flexxbotics on show at PMTS 2023

We are looking forward to attending the Precision Machining Technology Show (PMTS) on April 18-20, 2023 at the Huntington Convention Center in Cleveland, Ohio.

PMTS is one of the leading global events for the precision machined parts community to share challenges and insights, see new technology solutions and learn about process innovations.

If you are attending the show, be sure to stop by our partner Datanomix’s Booth #1060 to learn more about our FlexxConnect™ process control solution which combines with Datanomix’s next generation CNC production monitoring to provide your machine shop with a continuous improvement platform.

Book a meeting with us at PMTS

FlexxTend™ Product Launch

FlexxTend™ Product Launch

FlexxTend Product Launch

Flexxbotics Launches Complete Automated
Machine Tending Solution

Flexxbotics has today announced the official launch of FlexxTend™, a turnkey automated machine tending solution for machine shops to automate their CNC machines.

Setting up a machine tending application takes time and effort. Especially when machine shops are busy trying to get parts out of the door. FlexxTend™ takes care of the whole process for you. Our team designs everything to your specification and can be onsite integrating, validating and training 6 weeks later.

FlexxTend™ helps to…

Ensure rapid design and integration so your cobots go into production quickly, increasing your machine utilization and accelerating time to ROI.

Eliminate the headaches and inefficient time figuring out an optimal setup. Let our expert team handle everything, so you can focus on production.

Maximize functionality out of your machine tending setup by leveraging all the automation features of your CNC, cobot, and online services to enable lights out manufacturing.

Ensure robust operations and support by providing the tools to be able to run high mix low volume jobs.

Tyler Bouchard, Co-founder & CEO at Flexxbotics, said: “One of the key benefits of FlexxTend™ is that it gives us direct access to the systems so we can recognize downtime, troubleshoot issues, and provide direct changes to programs, all remotely. It’s like all of our customers have a Flexxbotics Automation engineer onsite all the time.”

Tyler continues: “We’re incredibly excited to launch the FlexxTend™platform which optimizes the design of your work cell so you can handle multiple parts, conduct rapid changeover, and run lights out manufacturing.”

Check out the FlexxTend™ demo below:

Learn more about the new FlexxTend™ Platform.

Benefits to CNC Machine Tending Standardization

Benefits to CNC Machine Tending Standardization

Benefits to CNC Machine Tending Standardization

Standardizing your CNC machine tending interfaces can have several benefits for your manufacturing process. From improving efficiency to reducing downtime, standardization can help your company run more smoothly. In this article, we’ll look at the benefits of standardizing your CNC machine tending interfaces, what you stand to lose by failing to standardize, and other factors you should consider when interfacing a cobot with your CNC machine. By the end of this article, you’ll have a better understanding of how standardization can help you streamline your manufacturing process and future-proof your facility.

What are the Benefits of Standardizing Your CNC Machine Tending Interfaces?

Faster Integration
Standardizing your CNC machine tending interfaces can significantly benefit the integration process, making it faster and more cost-effective. With pre-made software libraries and pre-built hardware available, you can quickly interface a cobot with a CNC machine without starting from scratch. Using a standardized method when integrating a new CNC machine also gives you a clear path forward, saving you time and resources. In addition, standardization simplifies the integration process, allowing you to get your cobot up and running more efficiently. On non-standardized units, integration costs are higher, and timelines are longer.

Simplifies Interfacing with Other CNC Machines
In most facilities, there are a variety of CNC machines in use. For example, multiple brands and various models within brands are typically represented on any manufacturing floor. By using a single standardized platform, you can use the same method to interface with all systems, regardless of whether they are new or legacy equipment. This eliminates the need to figure out a unique approach for each machine, streamlining the process and saving you time and resources. In addition, standardization simplifies interfacing with other CNC robots / machines, making integrating new equipment and maintaining existing systems more accessible.

Easier to Document and Retain Setup Knowledge
As a company grows, knowledge retention around the setup and operations becomes critical for onboarding new operators. With everything labeled, wired, and set up in a standardized way, including the software interface, it is easier for new operators and machinists to understand the system and get up to speed quickly. Standardization also allows for faster cross-training of operators, as they can learn one standardized system rather than multiple variations. This process makes it easier to rotate staff to different machines and maintain flexibility and productivity across your manufacturing floor. Standardization can help you onboard new staff more quickly, cross-train operators faster, and easily rotate staff to various machines. This flexibility is crucial for manufacturers in times of high demand and a thin labor pool.

Knowledge silos characteristic of non-standardized facilities leave manufacturers vulnerable to employee mobility. As engineers, machinists, and operators with specialized machine knowledge leave, so does their knowledge of how to set up, operate, and reconfigure that machine.

Faster Troubleshooting
In addition to easier documentation and knowledge retention, a standard setup makes it easier to identify variations that might be causing issues. This allows you to quickly isolate and fix problems, reducing downtime and improving productivity. Standardization can help you troubleshoot issues faster and more effectively, allowing you to keep your manufacturing process running smoothly.

Difficulty troubleshooting machine issues can lead to extended downtime, lost revenue, and increased frustration among staff. This can negatively impact a manufacturing business in terms of productivity, revenue, and employee morale.

Better Support and Knowledge Retention with the Interface
How quickly your operators and machinists can get up to speed with your CNC machine tending systems can be a significant challenge when interfaces aren’t standardized. In addition, if your system integrator or engineer is no longer working on the project or leaves, it can be difficult to determine how the previous integrator set up each machine. This knowledge gap ultimately leads to revenue loss due to increased downtime.

Standardization helps to eliminate these knowledge gaps, making it easier to retain interfacing knowledge and maintain your systems. Additionally, working with a third-party interfacing company, such as Flexxbotics, can provide additional support and standardization to help with the setup and future maintenance of your CNC machine tending system. Standardization can help you retain knowledge and ensure that you have a reliable source of support for your machine interface.

Simpler Remote Support
A standardized system lets you know exactly what the setup should look like on any machine, regardless of where you are located. This makes providing remote support for your machines easier and helps ensure that your manufacturing process stays running smoothly, even when you are not physically present on site. In addition, remote capabilities allow manufacturers to save on travel costs for themselves or the integrators they use for support.

Did you know that Flexxbotics provides remote support? Reach out to us today to learn how we can provide world class service remotely for our automation systems.

Simplified Maintenance and Updates
Standardizing your CNC machine tending interfaces makes it easier to perform maintenance and updates. With standardization, you can follow the same instructions for all machines, rather than creating and following different procedures for each one. This saves time and resources and helps keep your manufacturing process running with minimal downtime required for regular maintenance and software updates.

Easier to Standardize on Processes and Instructions
Standardizing hardware and software should lend itself to standardizing operator processes and workflows. Standardization can be incredibly beneficial for several reasons.

First, it helps to streamline the manufacturing process, making it more efficient and consistent. By having a standardized set of processes and workflows, operators can easily follow the same steps to complete tasks, eliminating the need to learn multiple variations. This systematic approach can reduce errors and improve the overall quality of the finished product.

In addition, standardization can also help to improve operator training and onboarding, as there is a clear set of procedures to follow. Without standardization, manufacturers may have to deal with multiple variations of processes and workflows, leading to confusion and a higher risk of errors.

Simpler Regulatory Compliance
Certain industries require specific documentation for regulatory compliance. A standardized system and set of instructions can remove a layer of complexity when meeting these requirements. With a standardized system in place, you can easily follow the same set of procedures and documentation requirements across all of your machines. This can be particularly helpful when processes need to be changed frequently, as it eliminates the need to create and follow separate procedures for each machine. Standardization can help manufacturers streamline their compliance efforts and make it easier to meet regulatory requirements across multiple machines.

Streamlined Re-deployment to Other CNC Machines
With standardized setups, it’s easier and faster to move cobots to new CNC machines. This mobility is important because production requirements can change, and machines can go down for scheduled service or unexpected reasons. The ability to move your CNC machine tending robots easily can be a huge benefit. Standardization can ensure that re-deployment is fast, simple, and minimizes downtime, helping you keep operations running even when facing unexpected situations. Other manufacturers will be tied to systems that they can’t move around flexibly as needed—leaving them stranded when CNC issues occur.

Reduce Errors and Oversight
When you have a standardized system in place, you can streamline your operations and eliminate common mistakes that might occur due to setup variations. This can help you maintain optimal levels of quality control. Poor quality control leads to increased part failures and wasted material–resulting in reduced profits.

If you are looking for a system to help you track performance and give you the tools to optimize and continually improve your workcell, check out FlexxConnect™ here.

Easier Scalability
One of the primary benefits is the ability to scale production more quickly. Adding additional CNC machines to your production line becomes much more straightforward when you have a standardized system. This is because you have already established a standardized integration, setup, and control process, so you don’t have to worry about the complexity, increased costs, and ramp-up time of one-off setups for each new machine.

In addition, you can easily copy previously proven systems to scale out production to meet increasing demand for your products. Overall, standardizing CNC machine tending can help manufacturers to be more agile and responsive to changes in the market.

Other Factors that You Should Consider when Interfacing a Cobot with Your CNC

Standardizing your CNC machine tending solutions can provide a range of benefits that can help your manufacturing business to run more smoothly and efficiently. Some additional benefits may include:

Upskilling Current CNC Machine Operators and Machinists
By using a standardized platform like FlexxCNC™, you can make it easier for your current CNC operators to learn how to operate the CNC machine tending setup. Furthermore, you might find your machinists able to take on tasks typically reserved for engineers. By upskilling your existing workforce, you enable them to be more versatile, which can improve the overall efficiency of your manufacturing process.

Loading G-Code and Macros into Memory
The FlexxCNC™ system allows you to load g-code programs and macros into memory on the CNC machine, which can help streamline your CNC machines’ operation. For example, this can make it easier for machinists to run multi-op and real-time offsets on their CNC machine directly through the cobot system without altering their g-code.

Running your CNC Machine Lights Out
With the FlexxCNC™ system, you can automate all aspects of your CNC machines, including the execution of g-code, the actuation of vises, chucks, and doors, and the initiation of stop/start/wait cycles. This can help you to run your CNC machines lights out, which can increase the efficiency of your manufacturing process and reduce the need for human intervention.

Do you want to streamline your operations and improve the efficiency of your manufacturing process? Our FlexxCNC™ system is a standardized platform that makes it easy to integrate, set up, and control CNC machines. Our team of experts is here to support you every step of the way. So don’t let the complexity of automated CNC machine tending hold you back. Contact Flexxbotics today to learn more about how we can help you standardize your CNC machine tending solutions and take your manufacturing business to the next level.

Contact us today to get started.

Challenges with setting up a CNC machine tending workcell

Challenges with setting up a CNC machine tending workcell

Flexxbotics Partner Insights - Svenska Elektrod

In this partner insights video, Karl Ericsson, Managing Director at Svenska Elektrod AB, talks all things CNC machine tending. Founded in 1981 and based in Täby, Svenska Elektrod is a certified partner and system integrator with Universal Robots, supplying a wide range of collaborative robots, components and accessories.

The interview covers;

1.    Who is Svenska Elektrod AB?
2.    What is CNC machine tending?
3.    What industries do you see the most CNC machine tending in your region?
4.    What are the biggest challenges with setting up a machine tending application?
5.    How do you help manufacturers overcome these challenges?
6.    What is your prediction for CNC machine tending in 2023 and beyond?

Find out more about our partnership with Svenska Elektrod AB here.

Learn more about FlexxCNC™ here

Flexxbotics Partners with CIMTEC Automation

Flexxbotics Partners with CIMTEC Automation

Flexxbotics & CIMTEC Automation Partnership

Flexxbotics is excited to announce a new partnership with CIMTEC Automation, expanding our presence in Virginia, North Carolina and South Carolina.

Established in 1987, CIMTEC is a certified partner with Universal Robots and a leader in full-service, customized industrial automation services and products. CIMTEC has become one of the industry’s largest, most advanced, responsive and trusted automation products and engineering solutions providers across a variety of industries.

Flexxbotics and CIMTEC will work together to provide cobot and CNC automation solutions including FlexxReference™, FlexxCNC™, and FlexxConnect™ UR to discrete manufacturers in these regions.

FlexxReference™

FlexxReference™

FlexxCNC™

FlexxCNC™

FlexxConnect™ UR

FlexxConnect™ UR

Tyler Bouchard, CEO at Flexxbotics, said: “We’ve expanded our partner network a lot over the last 18 months and are pleased to continue this momentum in 2023. We look forward to working closely with CIMTEC to help manufacturers build more product, faster!”

Learn more about FlexxConnect™ UR here

Flexxbotics Partners with Morris South

Flexxbotics Partners with Morris South

Morris South Announcement

Flexxbotics is pleased to announce a new partnership with Morris South to provide discrete manufacturers with robotic automation solutions for CNC machine tending applications.

Morris South is a leading CNC machine tool distributor, and has been the exclusive distributor of Okuma CNC machine tools in Alabama, Arkansas, Georgia, Mississippi, North Carolina, South Carolina, Tennessee, and Virginia since 1980.

Flexxbotics and Morris South will work together to provide cobot and CNC automation solutions including FlexxReference™, FlexxCNC™, and FlexxConnect™ UR to manufacturers in this region.

FlexxCNC™ is the leading Universal Robot (UR) to CNC interface, which can integrate a UR cobot to any machine in your shop in half a day, enabling you to automate all aspects of your CNC and run your machine tending applications lights out.

Looking to automate your CNC machine before the end of the year? Have you considered what type of interface makes the most sense? Check out our financial comparison today here.

FlexxCNC Financial Justification

Learn more about FlexxCNC™ here

The Right Way To Get Real-Time Manufacturing Data

The Right Way To Get Real-Time Manufacturing Data

The Right Way To Get Real-Time Manufacturing Data

Data analytics is a vital tool for today’s leading manufacturers. The insights they gain allow them to operate smarter, more productive, and more efficient operations. However, not all manufacturers currently take advantage of the opportunity data provides in their facilities. Understanding what data analytics for manufacturing is and how to leverage this opportunity enables manufacturers to optimize their operations better than ever before.


What is Manufacturing Analytics?

Manufacturing data analytics is collecting and analyzing data from machines and operations to make better business decisions. Such data can include machine performance data, inventory models over time, QA measurements, and downtime reports. By analyzing this data, companies can arrive at insights that help them diagnose problems, improve machine performance, and run a more profitable business. Companies collect data for manufacturing analytics via manual and automated methods. Likewise, they can perform data analysis through manual or software-assisted means. However, the amount of data provided by manufacturing machinery today means that companies can lose out on many insights by relying on manual methods alone.


Why is Manufacturing Data Important?

The amount of potential data from a manufacturing line and its potential impact can be invaluable for modern manufacturers. In the short-term, companies that leverage data analytics find it easier to make improvements and identify problems in their processes. Companies can better support their customers and interface more intelligently with suppliers by enriching their ERP and MES systems with manufacturing data.

Manufacturing Data Helps Define Effectiveness
Defining machine performance and effectiveness without data is a challenge. Without data, manufacturers are blind to how their machines are performing and where potential problem spots might be. Overall Equipment Effectiveness (OEE) is a gold standard for measuring optimal machines’ performance, but it requires data inputs to be calculated. And while other KPIs are more effective for measuring robot effectiveness, those measurements will also require data.

Manufacturing data also allows operators to measure the real-time performance of their equipment. Facilities use real-time data capture to display visualizations on HMI screens or SCADA systems. These tools allow operators and management to understand how their equipment performs in real time. By leading with data first, manufacturers can react quickly to alarms and correct potential problems.

Data Illuminates Areas of Improvement
Over time, manufacturing data can identify problem spots in your manufacturing process. Manufacturers use stored data to look for patterns indicative of issues. Perhaps during a certain time of day, a machine’s performance drops slightly, or part quality falls off. These problems might go unnoticed without the aid of data analysis to illuminate these insights.

Device history and logging allow operations managers to review machine performance before and after changes have been made to the system. Manufacturers can be hesitant to change their machines if they can’t verify that the changes have positively impacted them. However, device history and logging data allow companies to move forward with confidence on changes to the system because they know they can see the results and decide if the changes are worthwhile.


Types of Manufacturing Data Collection Systems

Manual Data Collection

Manual:
Manufacturers generally collect data in two ways: manual and automated methods. Even manufacturers with little experience or ability to leverage data analytics perform some level of manual data collection. They can gather at least some level of data through simple observation. Data points such as approximate cycle time, estimated throughput, and quality assurance metrics can be estimated over short periods of time. However, it’s often inefficient to dedicate staff to data collection over the long term. This is crucial because long-term data offers the most actionable insights for manufacturers.

Automated Data Collection

Automated:
Automated data collection systems are much more scalable. Thanks to the emergence of industry 4.0, the number of devices that support manufacturing data collection is increasing each year significantly. These systems also offer a higher level of data resolution than manual observation. Automated systems can measure thousands of data points per second. This is valuable information for manufacturers looking for every competitive edge they can find in their facility. Machines’ control systems can be a gold mine of potential performance data. However, extracting this data is only the first step–making sense of the data is critical.


Creating Data Pipelines

Usable data unlocks the possibility of using a fully integrated manufacturing tech stack. Data from the machine level is accessible to operators via an HMI. This data feed comes from sensors and the control system of the machine. Additionally, more detailed data is available at the SCADA level for multiple machines. This allows for supervisory control over an entire plant floor for plant managers. Machine-level monitoring provides real-time performance statistics to analyze effectiveness, performance, and efficiency. Machine data is fed to the MES system for performance analysis, data acquisition, and operational control. Management can monitor MES and ERP systems that–with the enriched data from the shop floor–can now make better decisions around scheduling, labor, and resource allocation.

Contextualization

While manufacturing data is immensely valuable, it means little without the right context. Extracting the data is the easy part, relatively speaking. For most companies, that involves ingesting data into a data lake for storage. However, this data is unprocessed and disorganized in such a state. Contextualization is getting this data in a state that’s usable for stakeholders. Contextualizing data might include:

– Data cleaning and normalization
– Data aggregation
– Data transformation
– Defining data schemas
– Creating relationships between data sets

Visualization

Of course, all this contextualized data should be stored in a relational database. Manufacturers can analyze historical data to look for trends and opportunities to improve their operations continuously. Powerful data visualization tools allow stakeholders to communicate findings from the data trends to support their conclusions.

Without contextualized data, decision-makers and analysts can’t ask questions about the data that will deliver those valuable insights to the business. It’s not data itself, but data that is usable that is of value to business leaders. Once data is properly contextualized, decision-makers can analyze it for insights.


Measuring Performance
with the FlexxConnect UR™

Integrating a manufacturing analytics stack from scratch can be a daunting task. However, it’s critical to running an efficient and optimized manufacturing operation. It’s especially important when running automated robotic workcells due to the dynamic nature of the application. The FlexxConnect UR™ lowers the barrier to entry for manufacturers looking to automate with a data-forward model in mind. The FlexxConnect UR™ offers three major benefits to manufacturers automating machines such as CNCs, injection molding machines, or inspection stations.

FlexxConnect UR
Ease Of Use

Ease of Use
The FlexxConnect UR™ is easy for operators with little to no robotics experience. Non-programmers configure jobs through a no-code interface. This empowers machine operators to assume ownership of the work cell. Now that manufacturers can quickly set up new jobs, your cobot spends more time in operation and less downtime for programming.

Real Time Data

Real-Time Data
Quick access to status and performance data is critical for understanding the status of your machine. The real-time data provided by the FlexxConnect UR™ shows operators the current status of the workcell. Operators can quickly react to changes or issues with this immediate access to performance data. Many manufacturers feel that they don’t have the personnel to extract and contextualize data for proper machine analytics–the FlexxConnect UR™ provides pre-built analytics tools, giving manufacturers actionable insights they can use to improve critical metrics such as throughput, cycle time, or production efficiency.

Cell Performance Analysis

Cell Performance Analytics
Access to performance data is key for decision-makers. The FlexxConnect UR™ provides manufacturing data collection software for key stakeholders to analyze cell performance. Manufacturers can calculate OEE and other KPIs to optimize their UR. Management can leverage historical performance data to look for trends and areas of opportunity.

Flexxbotics Integration Service

BONUS: Flexxbotics Integration Service
As a value-added service, Flexxbotics will fully integrate your Flexxbotics hardware and software into your workcell. This removes a massive lift for manufacturers new to robotic automation, manufacturing data analytics, or both. Flexxbotics can even remotely integrate the FlexxConnect UR™ into your existing business systems. This way, you can focus on running a productive automated workcell operation while leveraging all the benefits that manufacturing data has to offer.

Interested in learning more? You can read more about
the FlexConnect UR™ here or reach out to us today!

FlexxCNC™ Financial Justification

FlexxCNC™ Financial Justification

FlexxCNC Financial Justification

I’m Ready to Automate my CNC, now what?

So you’ve taken the plunge into automating your CNC machine. You’re tired of the lack of machinist labor and your current team is completely strapped keeping up with demand. Overall this is a smart move and your operations will benefit very quickly from the choice to switch to automated CNC’s. There are some things you need to know when kicking off an automation project, which can be reviewed in our article here. Having a solid interface between your CNC and robot is essential to a successful automation installation. Let’s run through your options and how each one generally works.

There’s generally three options for interfacing your robot to your CNC;

– Using Third Party Integration Services
– Do It Yourself (DIY) Integration
– Productized Robot to CNC Interface (FlexxCNC™)

When evaluating each of one these methods it’s important to understand the:

– Time it takes to execute
– Downtime associated
– Functionality you obtain


FlexxCNC™ Integration Cost Savings

The first and most straightforward justification for a CNC to Robot interface is the time x cost savings tied to rapid integration of your robot. Flexxbotics FlexxCNC™ interface touts the total integration time to interface your robot to your CNC is 4 hours or less. Traditional integration on average takes 2 days or 16 hours. If you’re planning on doing it yourself make sure to set aside 1 week to complete and that’s if you’re experienced with Systems Engineering. If you’re not, we suggest staying away from the DIY method. The “cost savings” quickly add up to internal costs, downtime and overall headaches.

To be clear, when we say interfacing we mean the interfacing integration only of your robot to your CNC. There are other integration costs associated with a robot integration including peripheral installation, part in-feed and out-feed assembly/integration and general robot programming/training. In this justification exercise, we are only focusing on the interfacing portion.

So let’s play this with the total cost associated with all three methods.

Integration Cost Savings FlexxCNC
Integration Cost Savings Traditional Integration
Integration Cost Savings DIY

(Average Output/Hours = $500/hour)*

It’s clear to see the cost savings associated using the FlexxCNC™ vs traditional integration or DIY.

FlexxCNC vs Traditional Integration
FlexxCNC vs DIY Integration

An added bonus to using a standardized interface is the additional automation output (labor reduction costs) you receive. You gain 12 additional hours over traditional integration and 36 hours over DIY, which translates to $300 and $900 labor savings respectively.


Fully Automated CNC

One significant and unique benefit of using the FlexxCNC™ is the ability to command the CNC to execute g-code, m-codes and macros through the robot. Any CNC machinist knows macros are essential when accounting for tool wear offsets on your g-code programs. The FlexxCNC™ gives you the ability to automate sending these macros from the robot to the CNC giving you true lights out manufacturing of your unattended CNC. The alternative is automating without using macros leaving you exposed to quality events usually resulting in scrapping our reworked parts. From our experience an event like this occurs once a month with an interface method that doesn’t allow the ability to utilize macro loading on the CNC. A quality event cost can then be calculated using the following assumptions.

Fully Automated CNC

Your total costs associated with this quality event would then be $7,000. Extrapolate over 12 months and you have $84,000 in lost output. Every facility of course is different so use your own numbers, but it’s clear even one quality event is detrimental to your CNC’s output.

Total Lost Output Costs per Month
Lost Output and Costs Over 12 Months

Standardizing your Automated CNC Operations

Great, you’ve integrated your robot! The hard part is done right? Well not exactly. You still need to have a plan for operating your automated CNC work cell. So what’s the ideal way to manage your automated work cells? First is standardizing the way you program your robots. Using the FlexxCNC™, allows you to use the same digestible program nodes and structures allowing your machinists to easily grasp programming the robot and translate training and knowledge across all of your automated CNC’s despite the brand or controller. Trust us when we say, empowering your machinists to manage your robot work cells will be the best automation investment you make next to the robot itself.

The second benefit of the FlexxCNC™ is the ability to do both single operation and multi operation CNC jobs. The FlexxCNC™ can run multiple g-code programs in sequence on your CNC unattended and without having to alter any of your existing g-code. This allows any skilled level operator to manage both the machine and robot with less interruptions, downtime and programming.

So how do you tangibly calculate the cost savings associated with these standardized operations? We compare the time it takes to program and setup the robot with the FlexxCNC™ interface and without with a few assumptions.

Standardizing Your Automated CNC Operations
Operational Cost Savings

So all in all it seems that the way you integrate and utilize your robot to CNC interface is the most crucial aspect of any CNC automation project. Your total one time cost savings can range from $12k-$14k and yearly operational costs can range from $100k-$120k per year greatly impacting your CNC operational equipment effectiveness (OEE). The ROI is clear with the FlexxCNC™ and if you’re in the midst of conducting an CNC automation integration reach out to us to learn more!

Total One Time Cost Savings
Yearly Operational Costs

If you would like to talk with a salesperson for an official quote
on the FlexxCNC™ reach out to sales@flexxbotics.com

What Is OEE & Why Has It Become The Gold Standard For…

What Is OEE & Why Has It Become The Gold Standard For…

OEE & Alternative KPIs For Cobot Operations

Most modern manufacturers use Overall Equipment Effectiveness (OEE) as the gold standard for manufacturing process optimization. OEE is a great metric for many traditional manufacturing applications. However, OEE as the only optimization target in high-mix and dynamic production environments might lead you to less-than-optimal conclusions. By understanding this context and applying alternative KPIs, you can make better decisions to optimize your cobot machine tending operations.


What is Overall Equipment Effectiveness (OEE)?

OEE stands for Overall Equipment Effectiveness. It is a calculation that determines how optimized a manufacturing process is based on a few key metrics. These metrics are used to compare the current performance of the process to how it should perform at its highest potential. Through this analysis, manufacturers can find specific areas of improvement. OEE is broadly considered to be best practice in the manufacturing industry.

Key Metrics of OEE:
Manufacturers calculate OEE using three key metrics: Availability, Performance, and Quality

Availability

Availability

Availability is the percentage of time that the machine operates. Availability is more colloquially known as “uptime.” The overall uptime is compared to the downtime to give manufacturers an idea of how often the machine is actually in operation.

Performance

Performance

Performance accounts for the speed of the process. The performance metric includes the ideal cycle time and total cycles and compares this value to the total running time of the machine. This metric gives manufacturers insight into whether their machine is reaching its speed potential.

Quality

Quality

Quality measures the percentage of acceptable units as a percentage of all units produced. Since some units will be defective, the quality metric quantifies the ability of the production process to create usable parts.

OEE Calculation
Manufacturers can calculate OEE by first calculating availability, performance, and quality. Then, by multiplying these values together, you’re left with a percentage that theoretically defines the effectiveness of your current workflow.

The Overall Equipment Effectiveness Formula:

Availability =

Run Time


Planned Production Time

Performance =

Ideal Run Time x # of Cycles


Run Time

Quality =

Ttl Parts Produced – Defective Parts


Ttl Parts Produced

OEE = Availability X Performance X Quality

Most modern manufacturers use Overall Equipment Effectiveness (OEE) as the gold standard for manufacturing process optimization. OEE is a great metric for many traditional manufacturing applications. However, OEE as the only optimization target in high-mix and dynamic production environments might lead you to less-than-optimal conclusions. By understanding this context and applying alternative KPIs, you can make better decisions to optimize your cobot machine tending operations.


Why is OEE the Gold Standard for Manufacturing?

OEE is considered the gold standard for manufacturing because it can be calculated easily and offers valuable insights. Manufacturers can use these insights to optimize their production processes. Ultimately, these improvements lead to leaner, more efficient, and more profitable facilities.

The OEE calculation lends itself well to helping manufacturers hit their manufacturing goals. The metrics that makeup OEE align well with specific KPIs. For example, identifying quality issues aids in waste reduction efforts. Additionally, for manufacturers aiming to increase throughput, investigating factors affecting availability and performance are good places to start.

These areas of improvement are categorized as the “Six Big Losses.” By identifying factors leading to losses in these categories, manufacturers can take appropriate action to improve.

Availability

Planned Downtime

Breakdowns/Unexpected stops

Performance

Minor stops

Speed loss

Quality

Production reject

Rejects on start up

Most modern manufacturers use Overall Equipment Effectiveness (OEE) as the gold standard for manufacturing process optimization. OEE is a great metric for many traditional manufacturing applications. However, OEE as the only optimization target in high-mix and dynamic production environments might lead you to less-than-optimal conclusions. By understanding this context and applying alternative KPIs, you can make better decisions to optimize your cobot machine tending operations.


Why OEE isn’t Enough for All Circumstances

Unfortunately, OEE is not a silver bullet to improve all manufacturing processes. While it’s an excellent benchmark for most manufacturers, OEE doesn’t take specific context into account. This context is critical when making decisions on workflow changes. Blindly adhering to OEE can be detrimental to the optimization of your process. Let’s cover a few examples where OEE doesn’t capture the entire picture.

Cost:
You might’ve noticed that there’s no cost component to OEE. This calculation is purely looking at hard efficiency and production metrics. However, manufacturing is a business. Overlooking the impact of costs can lead to optimizations that negatively impact your bottom line. For example, it might be more expensive to run production at specific times or in certain circumstances. Optimizing purely for OEE here could mean running production at a higher expense. Furthermore, some parameters might be more costly than others. As an example, imagine you have two options available to you:

1. Improving performance by 10%
2. Improving quality by 15%

These would both significantly positively impact OEE. All else equal, improving quality seems like the better choice. However, this doesn’t take cost into account. Let’s assume the performance improvement costs $20,000, but the quality improvement costs $100,000. Considering the business component, it might make more sense to opt for performance improvements in this example.

Dependencies:
Some parameters might have dependencies on each other. OEE tends to imply its components exist in isolation from one another. In reality, changes to one part of the system can affect others. Consequently, changes aimed at improving one component of OEE impact other components. These effects can be both positive and negative. It’s important to take the entire effects of the system into account.

Dynamic Environments:
OEE doesn’t adapt well to dynamic production environments. Manufacturers commonly deploy cobots into these environments thanks to their adaptability. Examples include high-mix production environments with high cycle time variability, run time, batch size, etc. It’s not usually reasonable to recalculate OEE every time there’s a production change. Small production runs might also be active for a few days. This doesn’t provide much time for optimization.

Furthermore, your metrics will be skewed when measuring current production runs against OEE calculations against production runs on other parts. For example, cycle times for batch A might be 3 mins, but 5 mins for batch B. If you originally calculated OEE against the machine running batch A, comparing the performance of batch B based on that benchmark will yield very poor results. Even huge improvements to batch B’s performance will still lead to terrible OEE results from this perspective.


Other KPIs to Consider

It’s important to have other KPIs in mind when using cobots. Relying on OEE typically isn’t enough for cobot applications. Instead of optimizing for specific values in the OEE formula, manufacturers should aim for profitable, productive, and lean production. Let’s look at a few examples.

Improvements In Cycle Time

Improvements in Cycle Time:
Robots can significantly impact cycle times. Measuring cycle time improvements is an important KPI for cobot automation. The jump from manual to automated processes typically sees great improvements in cycle time. Additionally, automated systems have much more predictable cycle times when compared to manual production. However, manufacturers can measure cycle time improvements to previously automated systems by implementing process improvements.

Ways to improve cycle time include:
– Reducing common faults
– Optimizing for reduced wait time
– Tuning out motion inefficiencies

Improvements In Total Cycle

Improvements in Total Cycles:
Total cycles completed are analogous to overall throughput. A huge benefit of cobots is that they enable manufacturers to run more cycles per day in most circumstances. For example, cobots can continue running as long as material is available. The positive impact on total cycles is a critical KPI to measure the effectiveness of your cobot system.

Ways to improve total cycles include:
– Increasing cycle time
– Reducing downtime
– Reducing changeover/switch time

Improvements In Machine Utilization

Improvements in Machine Utilization:
Machine utilization is important for all machines in a manufacturing facility. Certainly, you can measure machine utilization from the perspective of the machine’s utilization. However, it’s equally important to consider the cobot’s utilization. Cobots have a special strength in being especially flexible in the tasks they can handle. For this reason, it’s even more important to monitor the utilization of your cobot. For example, a cobot’s primary task might be machine tending. However, if there are no more parts to run for the time being, a cobot could be switched to other tasks such as packaging or polishing. This increases the cobot utilization rate. A high utilization rate ensures that you’re getting the most out of your investment.

Ways to improve machine utilization include:
– Reducing downtime
– Reassigning your cobot to secondary tasks


How to Record Data for Robot KPIs

Manufacturers have many tools available to them to measure machine performance to calculate OEE and alternative KPIs. The source of these measurements lies in the data collection. Data collection can occur in one of two ways: automated or manual.

Automated data collection systems allow for real-time tracking of machine performance across dozens of metrics. Automated data tracking offers the richest source of data collection for analysis. Automated data collection tools tend to allow for easy pairing with data analysis software. Automated tools can be either first-party or third-party software products.

Manual data collection refers to people explicitly taking measurements in-person. There are many drawbacks to this system including measurement error, observer bias, and low measurement resolution. While automated data collection systems are preferable, manual solutions are better than nothing.

Today’s data-driven manufacturers are making constant improvements and finding competitive advantages. These leading manufacturers understand that high-end cobot operations go beyond OEE. By applying context and considering alternative KPIs, these companies are making the best decision for creating a lean, profitable, and high-performing production environment.

The FlexxConnect UR™ is a great choice for manufacturers moving towards a data-informed approach to continuous improvement. The FlexxConnect UR gives operators real-time feedback on what’s happening with their Universal Robots. For deeper analytics, more detailed information is available to look for areas to optimize. FlexxConnect UR is friendly, simplified, and easy to use. Designed for manufacturers, it puts your Universal Robots data into context and shows you the most important information.

FlexxConnect UR™

Reach out to us today to schedule your demo!

FlexxConnect™ UR Product Launch

FlexxConnect™ UR Product Launch

FlexxConnect™ UR Product Launch

Flexxbotics Launches Continuous Cobot Improvement Platform

Flexxbotics has today announced the launch of FlexxConnect™ UR, a continuous cobot improvement platform that empowers discrete manufacturers to easily manage their cobots and maximize cobot performance.

FlexxConnect™ UR provides instant access to contexualized data and intelligence enabling you to fully optimize and continuously improve cobot performance.

The platform also gives simple step-by-step instructions enabling a quick transfer of ownership of cobot work cells to operators, upskilling the existing workforce. 

FlexxConnect™ UR Product Launch Benefits

Take the first step to your digital transformation with a single cobot and quickly expand to multiple cobots. Don’t stop there with FlexxConnect™ having the ability to expand to any type of work cell with it’s industrial no code connectors and can be integrated into existing business systems such as ERP, MES and SCADA business systems.

Tyler Bouchard, Co-founder & CEO at Flexxbotics, said: “When manufacturers invest in a cobot, it’s important that it runs to the highest utilization possible. We are excited to expand the FlexxConnect™ platform with the UR specific module that ensures they can achieve this and empower their workforce to manage these work cells at the same time!”

Learn more about the new FlexxConnect™ UR platform or book a demo today!